Stud Welding Selection Guide | Hebei Wotu Fastener Manufacturing Co., Ltd.

Stud Welding for Metal Assemblies

Stud welding attaches a threaded or plain stud to a metal surface from one side, giving you a fixed mounting point without drilling through the panel or fitting a nut behind it. The key purchase decision is matching the stud, welding process and base material to the load, panel thickness and finished application.

For enclosures, brackets, insulation systems and structural assemblies, the right choice can reduce assembly steps and preserve the opposite face of the workpiece. Ask first which stud form and welding method suit the metal and joint function, rather than choosing by thread size alone.

Related Products

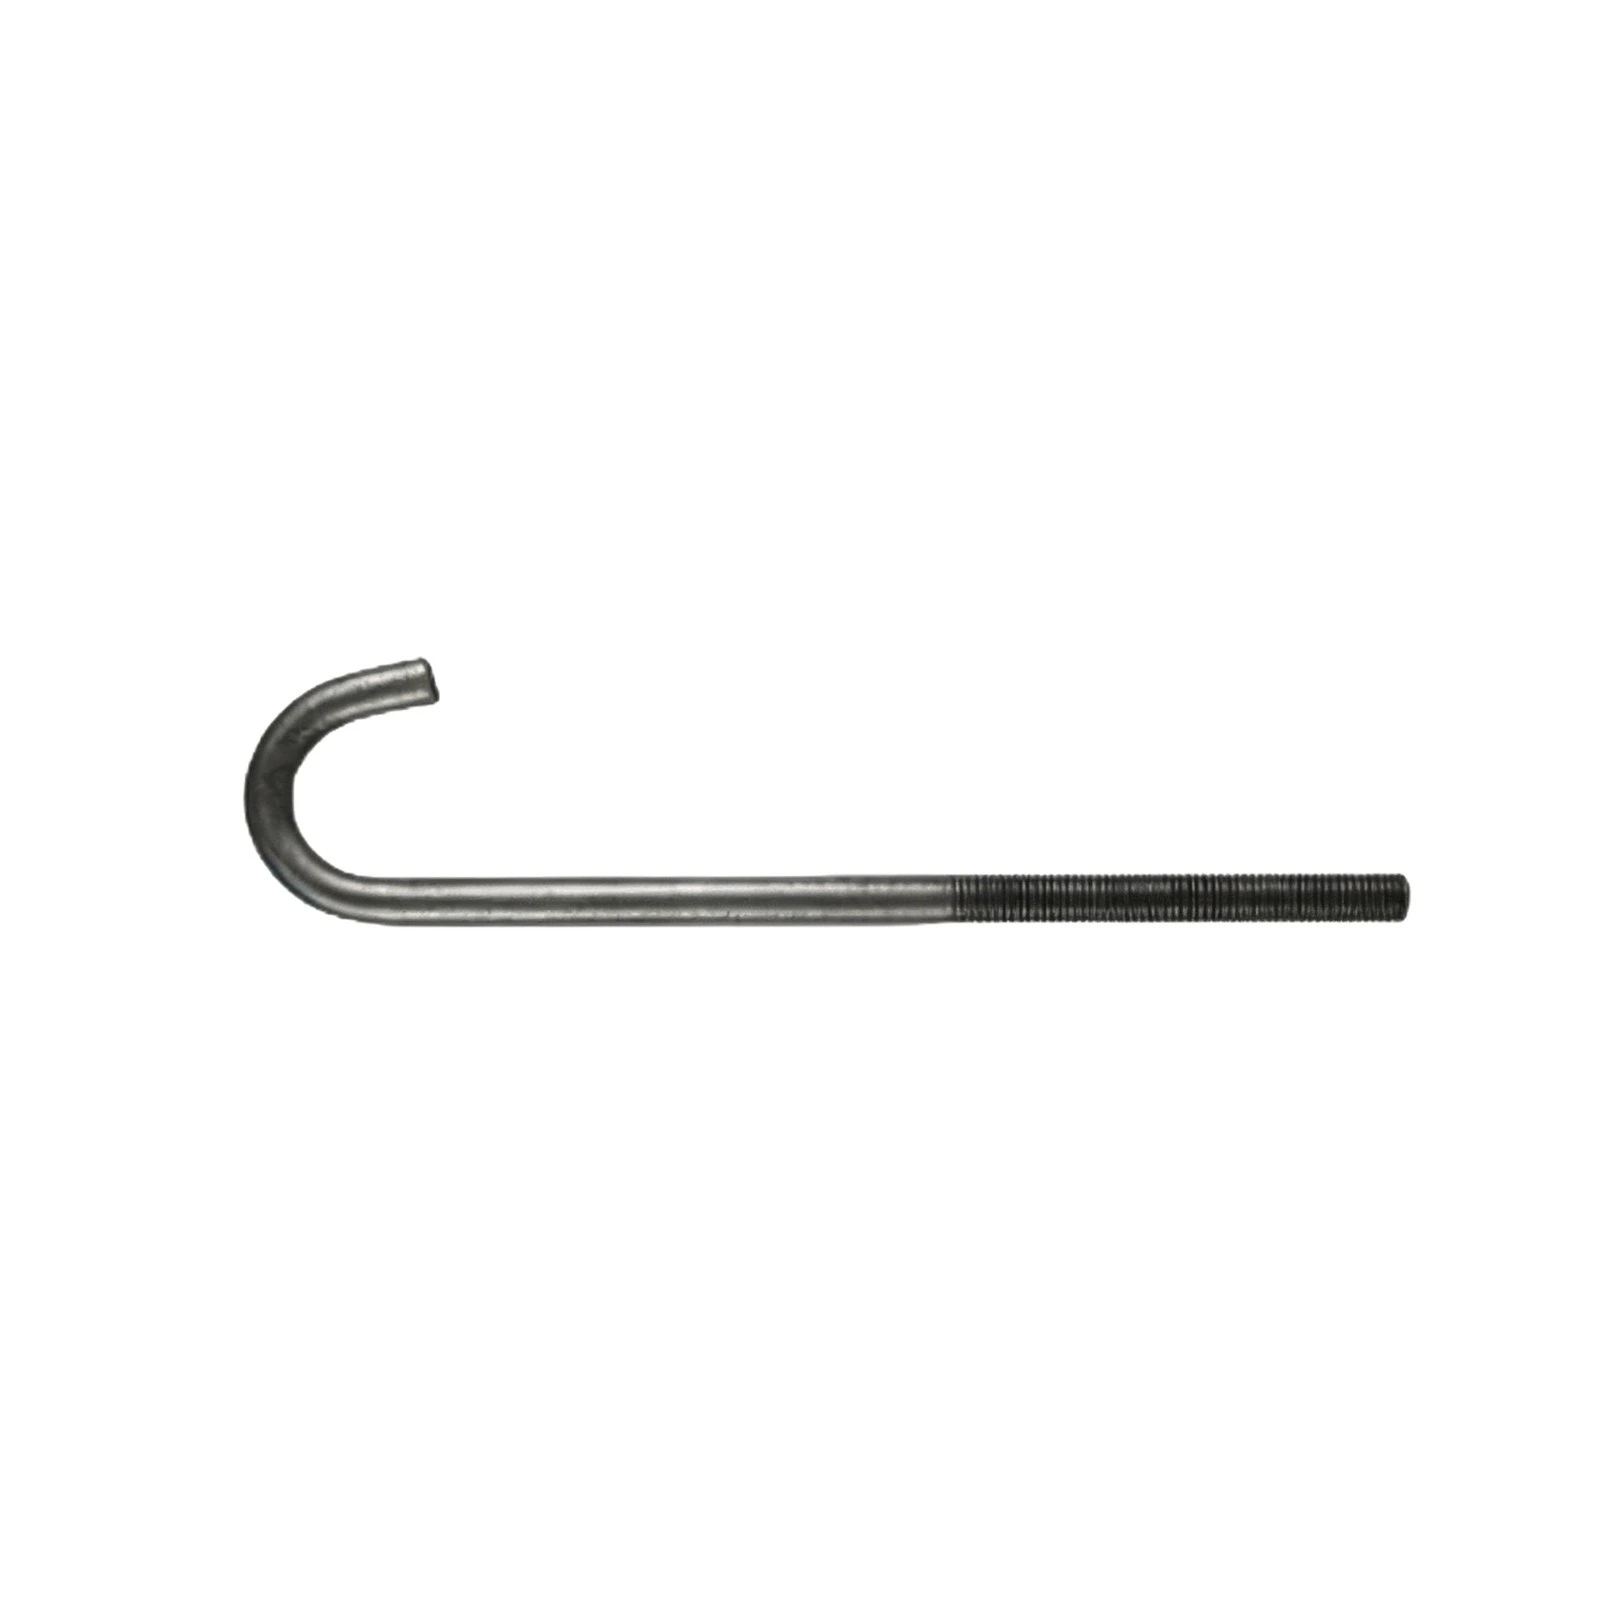
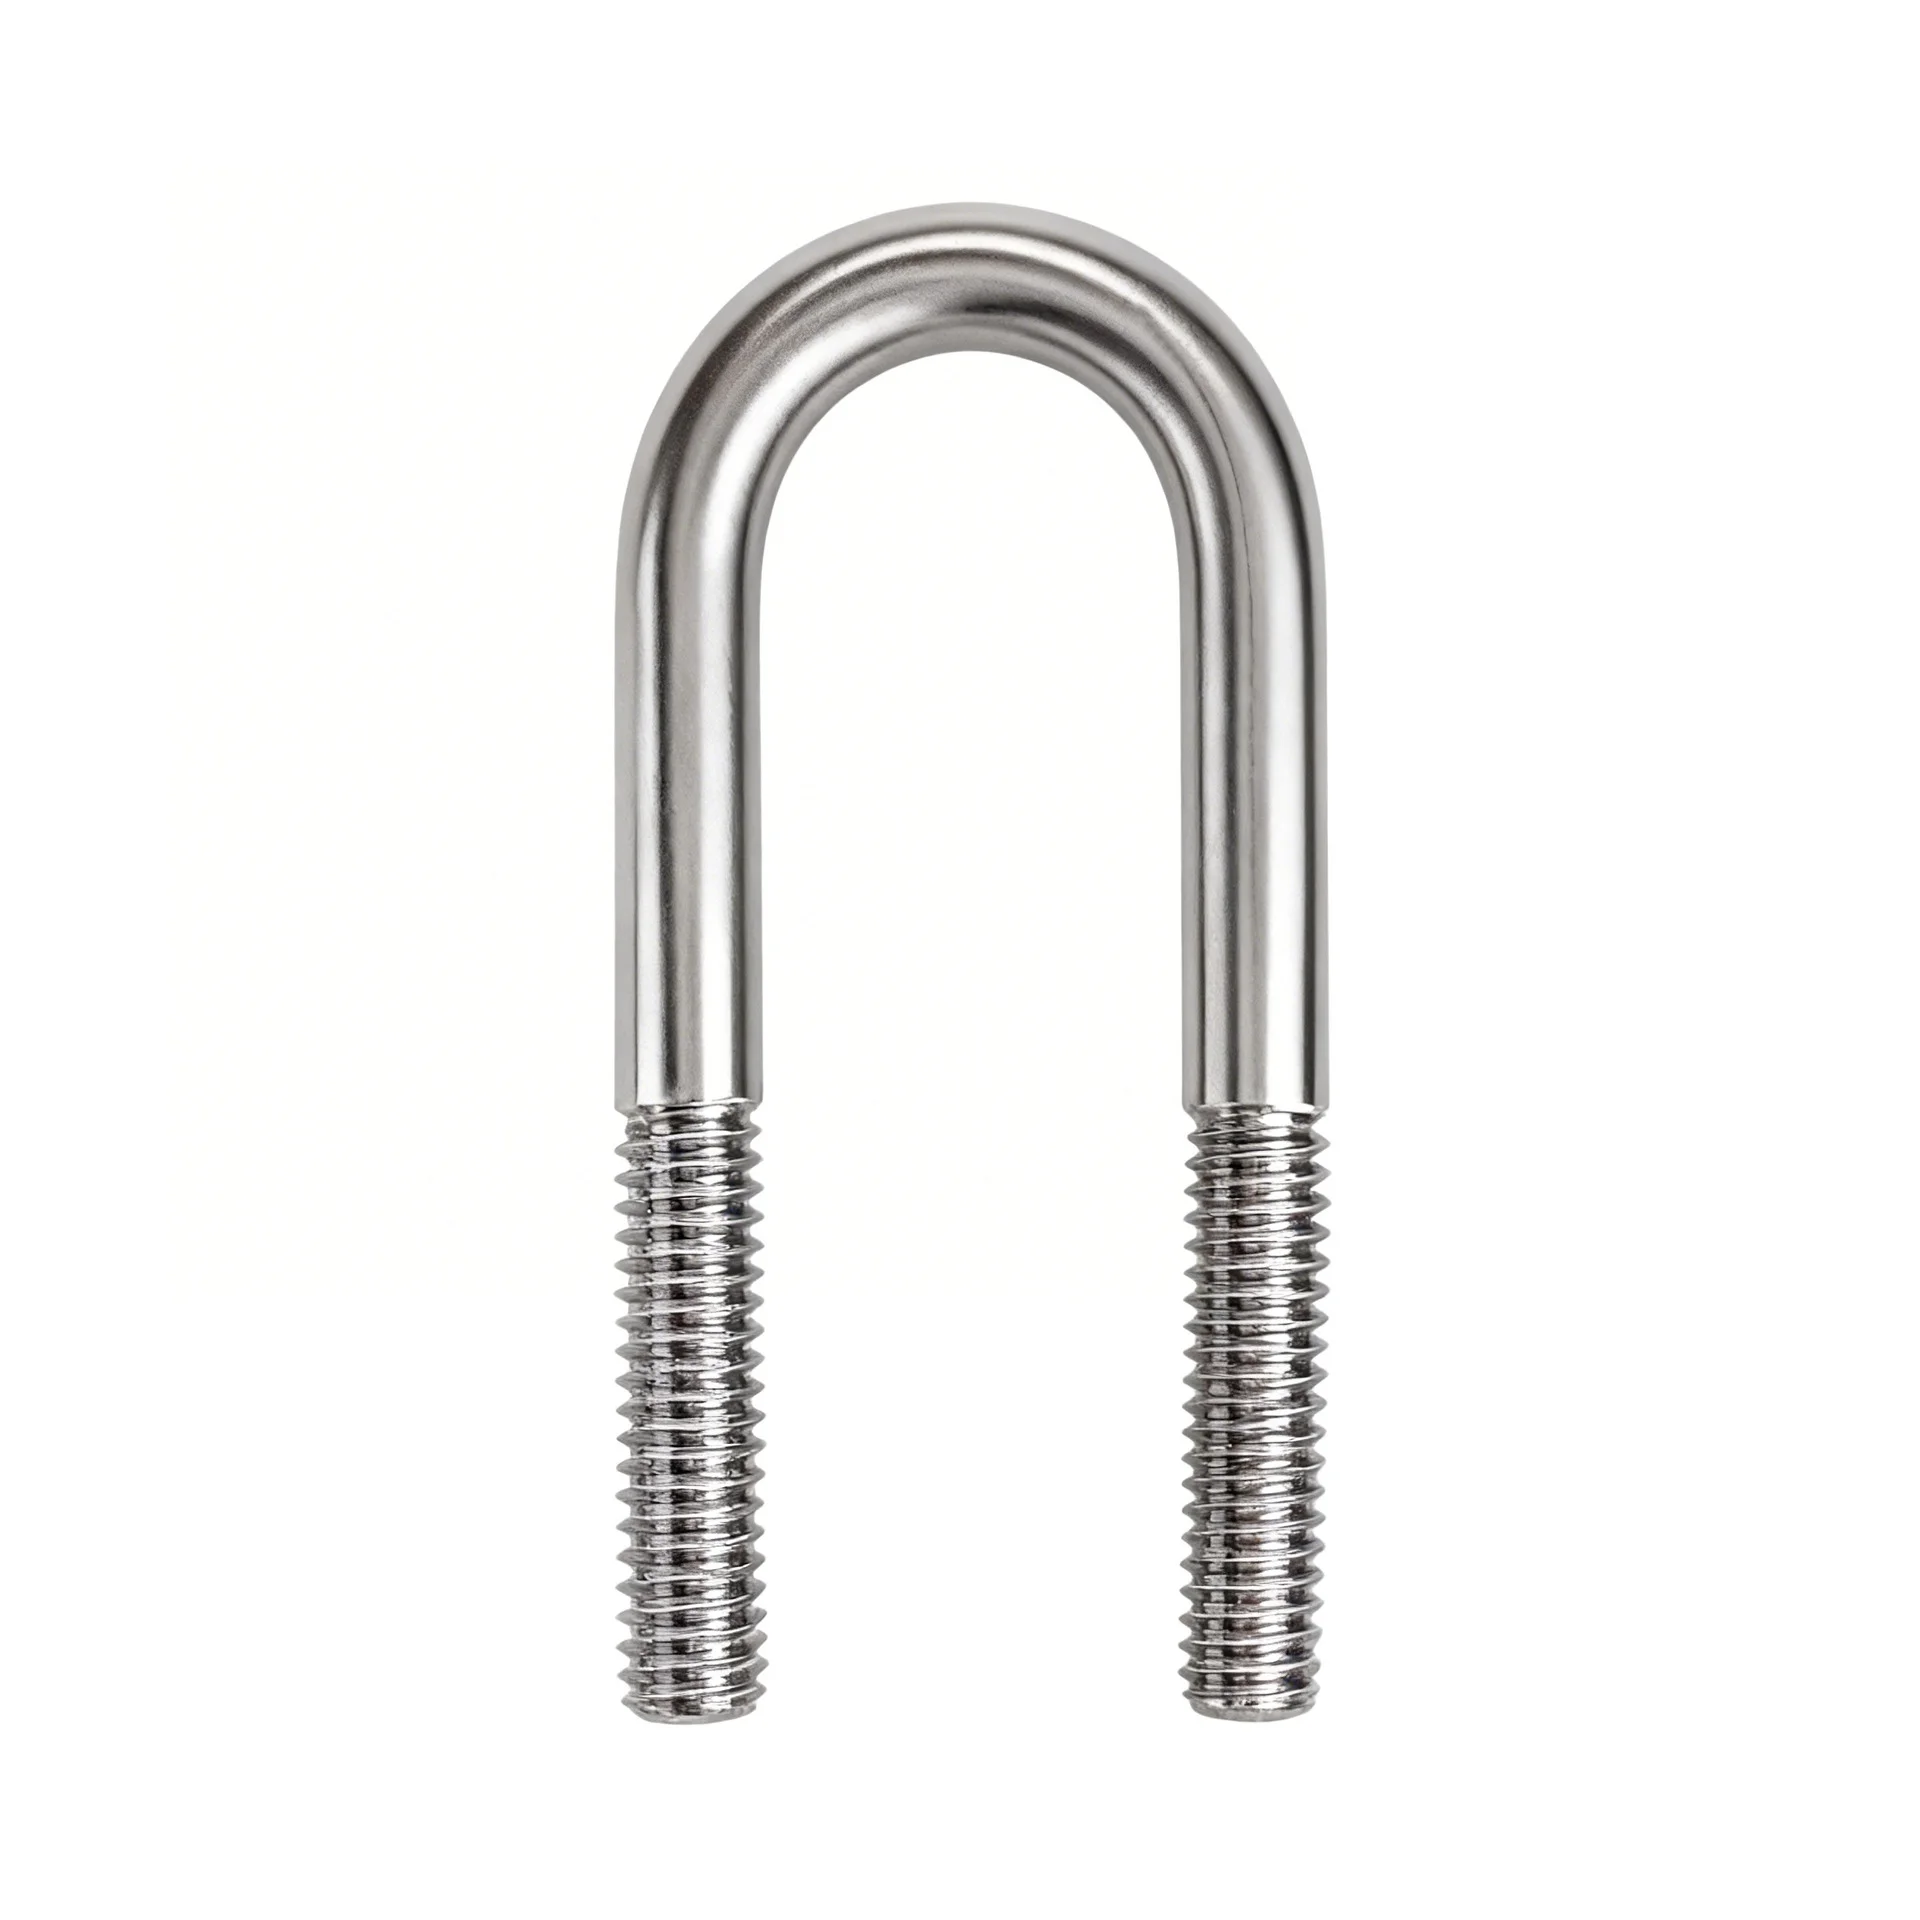
U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

Brand: Wotu Surface: natural black oxide / hot-dip galvanized / blue-white zinc plated, multiple processes available Specifications: Based on common industry drawing parameters, suitable for pipe diameter 25mm~139.7mm, screw diameter M10~M24, total length can be nonstandard customized Matching: can be matched with nut, flat washer and spring washer of the same specifications for complete shipment Packaging: Bundling and packaging + 25kg export carton, full-container wooden pallet wrapped with film, supports private-label export packaging

Read More

Compare stud types by joint function and base material

Stud welding options

Compare stud options by function, material compatibility, thread or shank form, dimensions, coating, weld-process compatibility and the load or fastening arrangement they must support. The correct choice also depends on the base-metal thickness, access for the welding tool and the finish required after attachment.

Criterion What To Check Why It Matters Buyer Tip
Stud type and end design Confirm whether the stud is threaded, unthreaded, headed, or internally threaded, and check the weld-end design. The end design must suit the fastening method and the load the finished joint will carry. Ask which stud geometry is recommended for your joint and welding process.
Base material compatibility Match the stud material and grade with the parent metal, thickness, and service environment. An unsuitable combination can cause poor weld formation, distortion, or corrosion at the joint. Provide the base-metal grade, thickness, and exposure conditions for a compatibility review.
Welding process and equipment fit Verify compatibility with the available stud-welding process, power source, chuck, and accessories. A stud that does not fit the equipment or process may not weld consistently or seat correctly. Ask for the required equipment setup and whether sample welds can be checked before production.
Thread and dimensional control Compare thread form, diameter, length, head dimensions, and any tolerance information with the assembly drawing. Incorrect dimensions can prevent nuts, brackets, or mating parts from fitting after welding. Send the drawing or a controlled part specification rather than ordering from a nominal size alone.
Surface finish and protection Confirm plating, coating, or bare-metal condition and how the finish is maintained through welding and service. Surface treatments can affect weldability, corrosion resistance, and the final appearance of the joint. Ask whether the supplied finish is intended for welding and what post-weld protection is required.

Choose a stud-welding setup that fits the joint

Capacitor-discharge welding is commonly considered for smaller studs and thinner sheet because its short cycle can limit heat exposure. Drawn-arc welding is generally considered for larger studs, heavier sections or applications requiring deeper fusion. The suitable process depends on the base-metal grade and thickness, stud diameter, joint loading and available equipment.

This distinction matters because an unsuitable process can cause weak attachment, distortion, surface damage or inconsistent results. Confirm the recommended process and qualification basis for the exact stud and material combination before placing an order.

Start with the joint function. Specify whether the stud will carry a threaded fastener, support insulation, locate a component or transfer structural load. Threaded studs, shear-style studs and insulation pins serve different purposes; substituting one for another can create clearance, strength or installation problems.

Match the materials and finish. Identify the base metal, stud material, coating and any post-weld treatment. Galvanized, painted or otherwise coated surfaces may require a defined preparation and process, while dissimilar metals can raise corrosion or weldability concerns. Ask what material combinations the manufacturer supports and what surface condition is required.

Check geometry and access. Provide the stud length, thread or plain-shank form, diameter, projection requirement and the panel or section thickness. Allow for nearby edges, bends, holes and coatings. A stud that fits the drawing may still be unsuitable if the welding tool cannot reach the surface or the finished assembly needs more clearance.

Confirm consistency before committing to volume. Request representative samples or a documented evaluation using your actual material and joint design. Include the intended quantity, inspection expectations and packaging needs in the enquiry. Ask Hebei Wotu Fastener Manufacturing Co., Ltd. whether it can supply the required stud type and what process, material and quality information it can provide for your application.

Criteria Importance Description Example Options
Welding process Usually one of the first decisions Capacitor-discharge and drawn-arc methods suit different stud sizes, base materials and heat input requirements. The process should match the joint strength, surface condition and section thickness. A small mounting stud on thin sheet may call for a different process than a larger stud on a heavy bracket.
Stud function and form Directly affects fit and performance Threaded studs, plain pins and shear-style studs are not interchangeable. The selected form should match how the finished assembly carries load, locates parts or supports another component. A threaded mounting point for a cover panel has different requirements from a pin used to retain insulation.
Base material and surface condition Critical for weld quality Material grade, thickness, coatings, paint, scale and surface contamination can change weldability and preparation needs. Confirm the acceptable surface condition before production. A coated panel may need a defined preparation method before welding, while bare steel may require a different handling approach.
Access and clearance Important before finalizing the drawing The welding tool needs enough room around the stud location, and the finished stud must leave space for the mating part, nut or washer. Nearby bends, edges and holes can restrict installation. A stud placed close to a formed corner may fit in CAD but be difficult to weld consistently.
Verification before volume supply Recommended for new combinations A new stud, material or coating combination should be checked using representative parts. The buyer should agree how the attachment will be inspected or evaluated before committing to larger quantities. A sample run on the actual panel material can reveal distortion, weak attachment or clearance problems before production.

Blog Articles / Reviews

The Concept of Hexagonal Self-Drilling Screws and High-Pressure Standard Parts

The Concept of Hexagonal Self-Drilling Screws and High-Pressure Standard Parts

Hexagonal self-drilling screws, manufactured by Hebei Wotu Fastener Manufacturing Co., Ltd., operate under a modern enterprise system and strictly manage according to the ISO9001:2015 quality system. The company uses “Wotu” as its registered trademark. The term “standard parts” in China is a shorthand for “standard fasteners,” a narrow definition. High- and medium-pressure standard parts refer […]

Frequently Asked Questions

Is this process suitable for thin sheet metal?

It can be, but the welding method matters. Capacitor-discharge stud welding is often considered for thinner sheet because it uses a short welding cycle, while the final choice still depends on sheet thickness, base metal, stud size and surface condition.

How is stud welding different from drilling and bolting?

Stud welding creates a fixed attachment point from one side of the workpiece, so it can avoid through-holes and rear-side access. Drilling and bolting may be easier to inspect or replace, but they add holes, extra hardware and possible sealing concerns.

Can the same stud be used with any welding process?

No. Stud geometry, diameter, material and weld end design need to match the intended process, such as capacitor-discharge or drawn-arc welding. A stud that fits the drawing dimensionally may still perform poorly if it is not designed for the welding method and base metal.

What information should be included in an enquiry?

Send the stud drawing or basic dimensions, thread or shank type, material, coating, base-metal grade and thickness, application, expected load if known, and quantity. It is also useful to state whether surface appearance, corrosion resistance, packaging or inspection records are important for the project.

What is a common mistake when selecting welded studs?

A common mistake is choosing only by thread size and length. The weld process, stud end design, base-metal thickness, coating and access for the welding tool can be just as important as the thread specification.

Leave Your Message

Tell us the stud type or drawing, the base-metal grade and thickness, and the application or expected load so we can address process and compatibility questions.