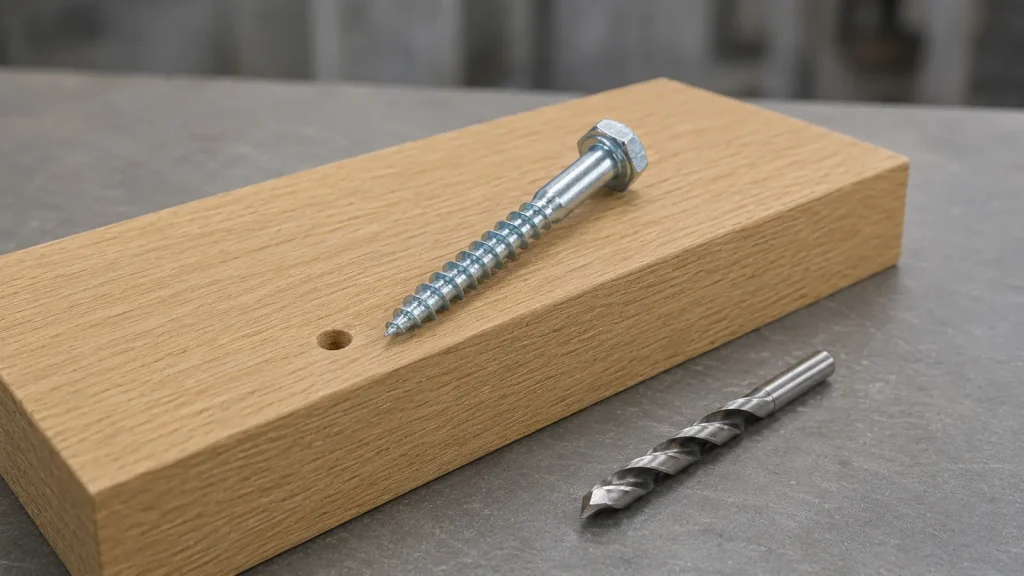
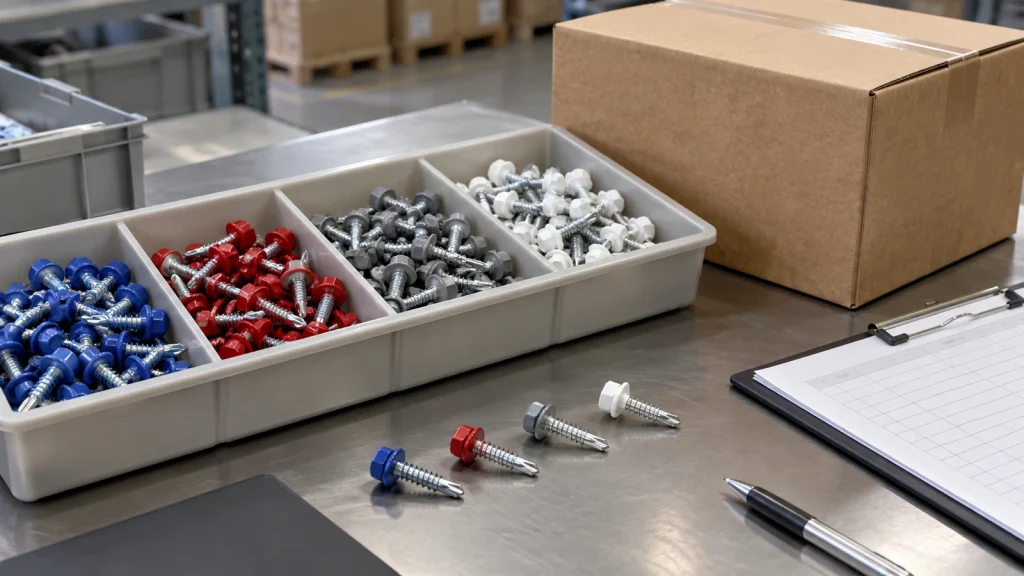
| Head style and drive interface |
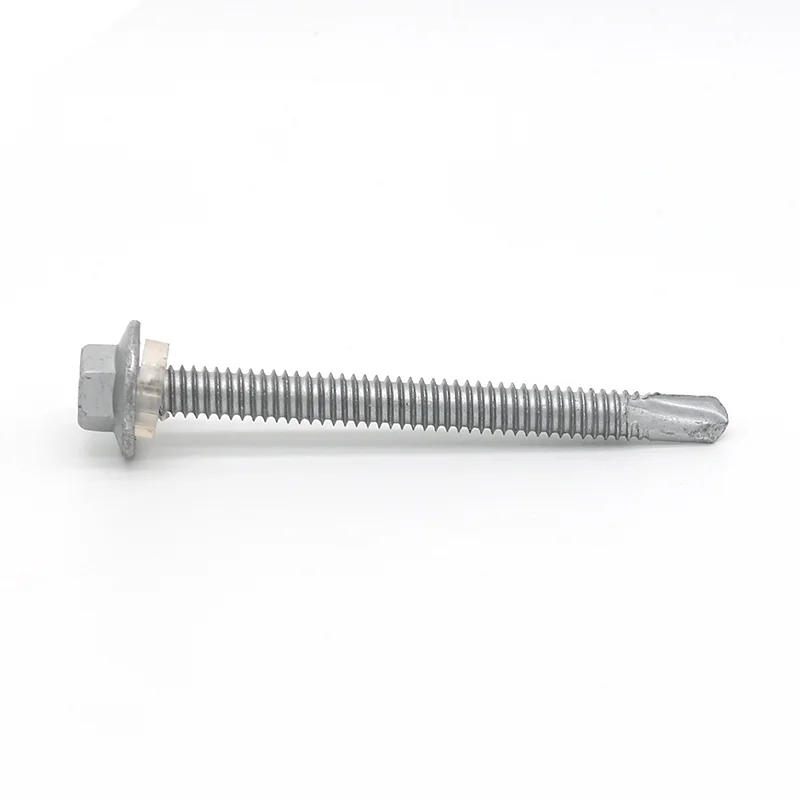
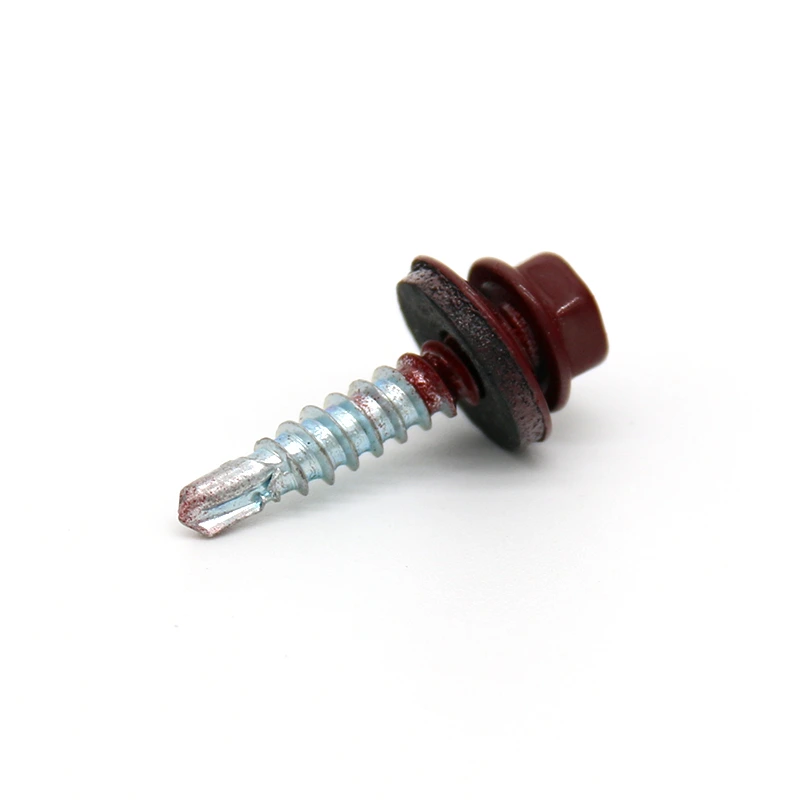
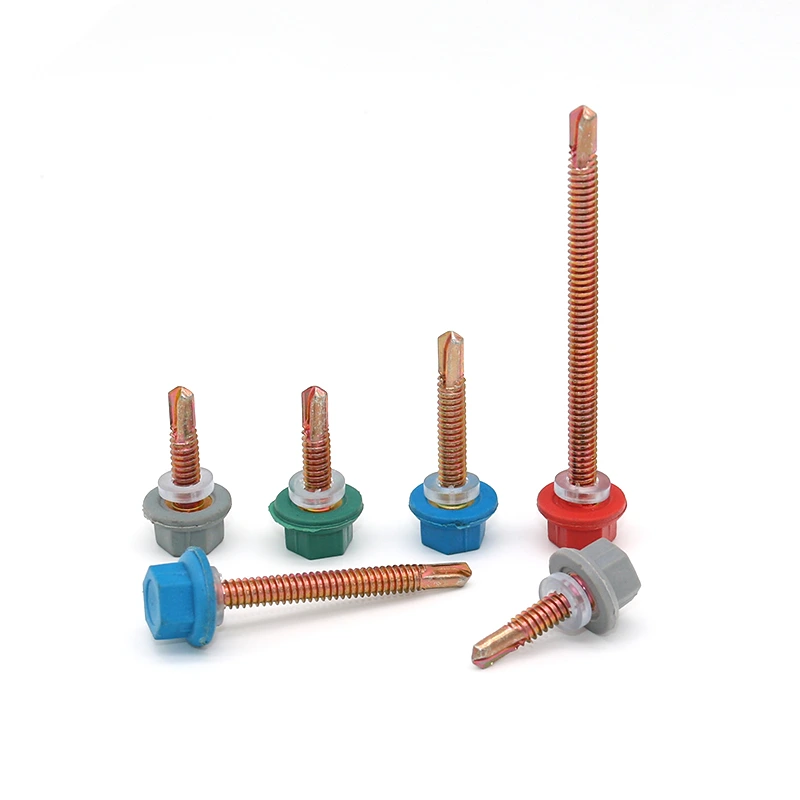
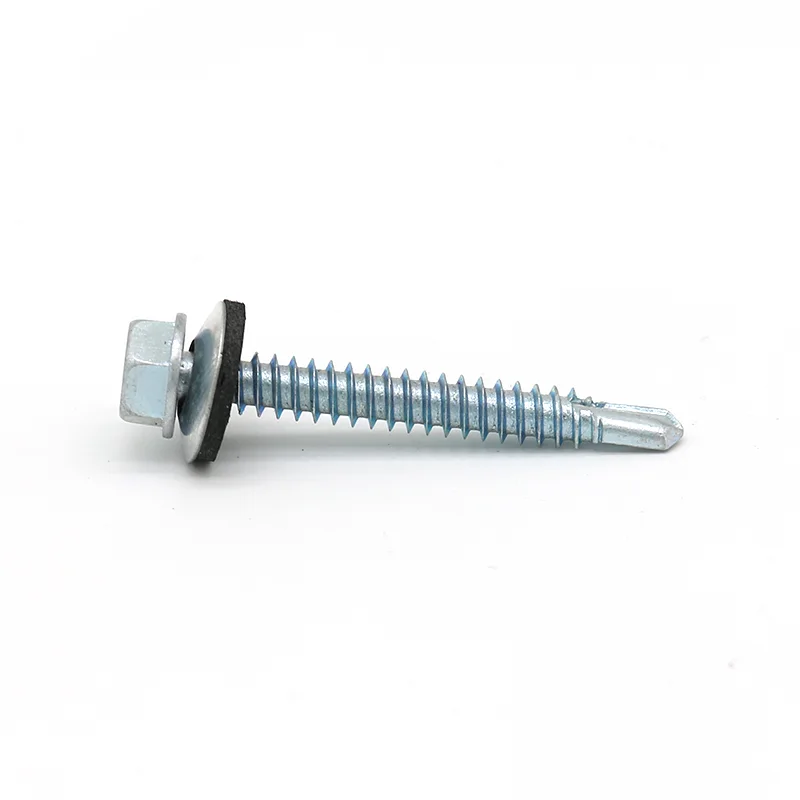
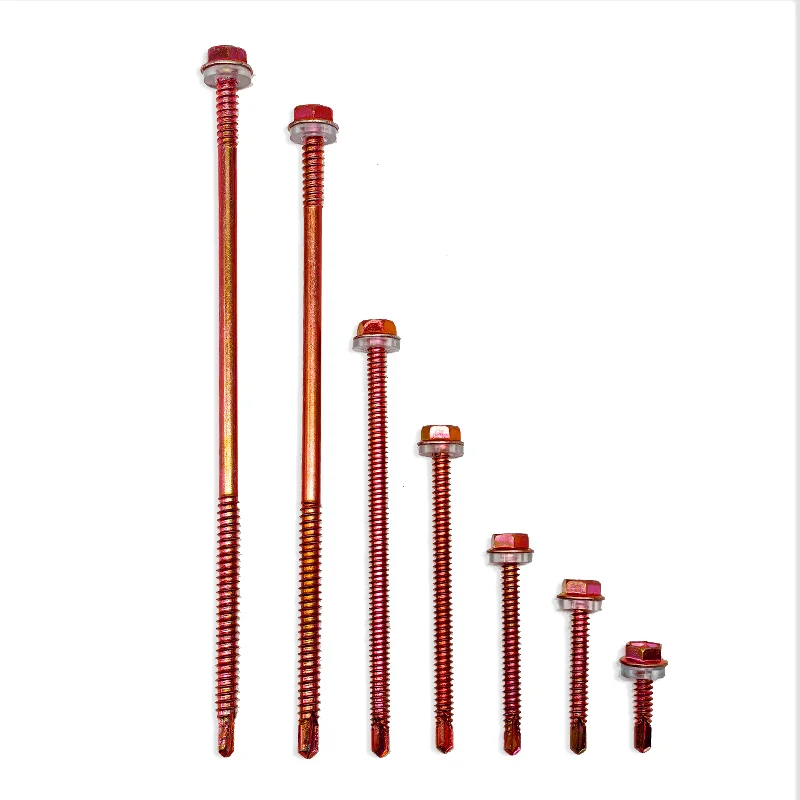
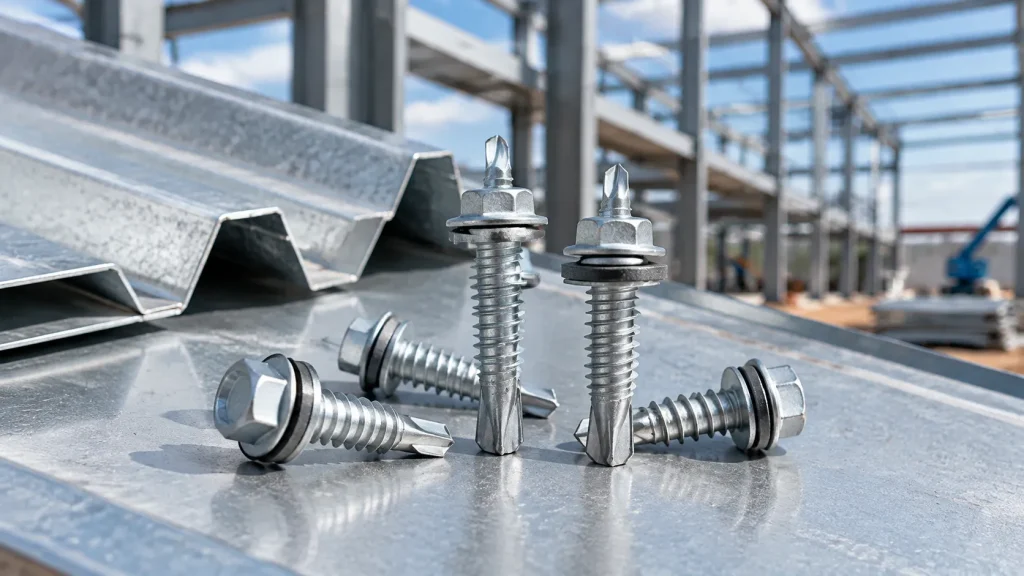
Confirm whether the screw has an external hexagonal head, an integrated washer, and a compatible wrench or socket size. |
The head determines tool access, tightening control, clearance around the joint, and the risk of tool slip during installation. |
Ask for a dimensioned drawing showing head width, head height, washer details, and the required tool size. |
| Thread form and intended material |
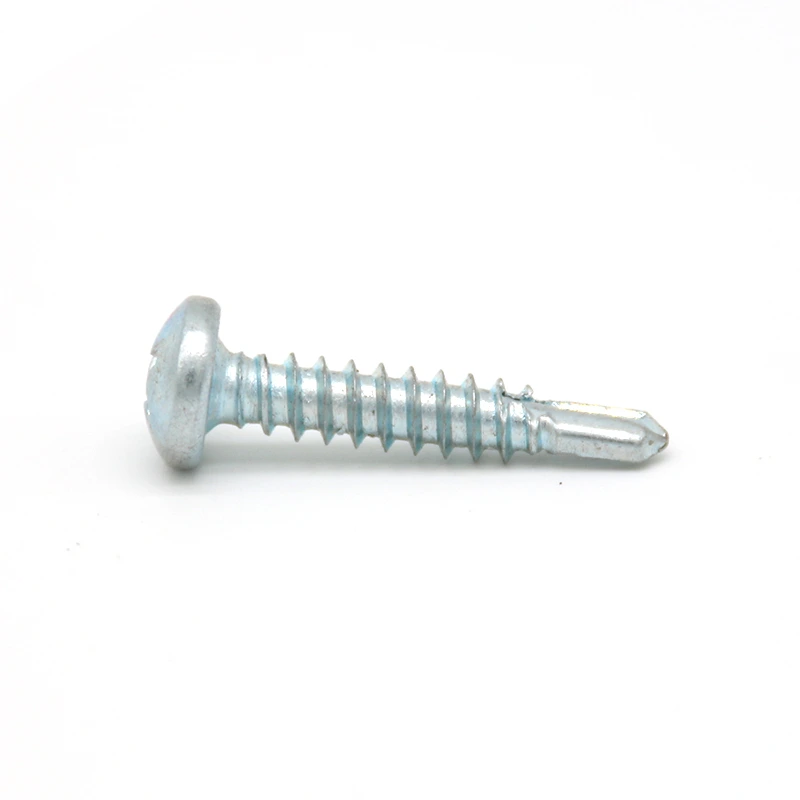
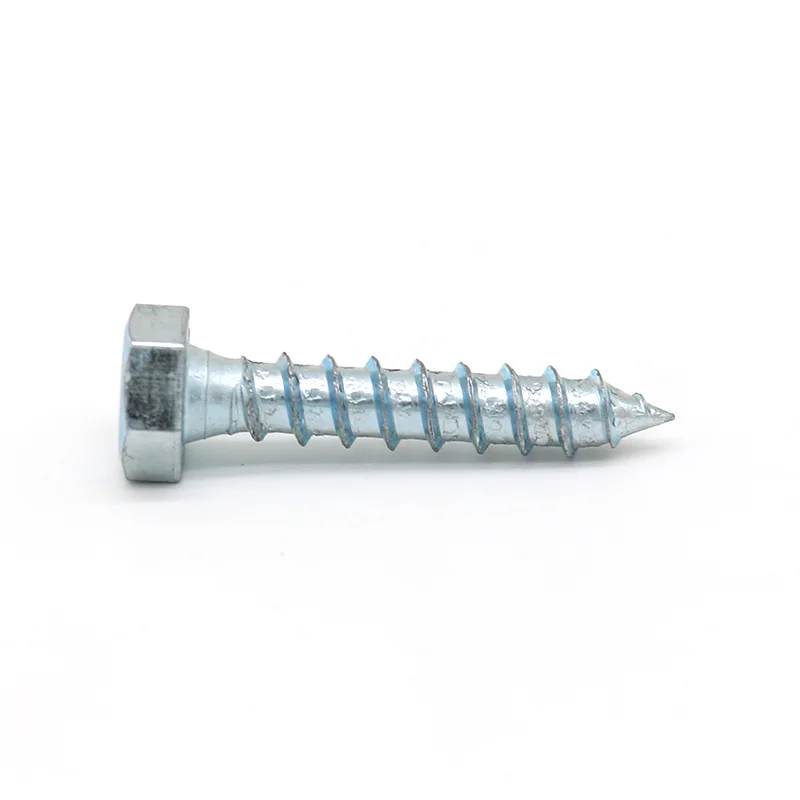
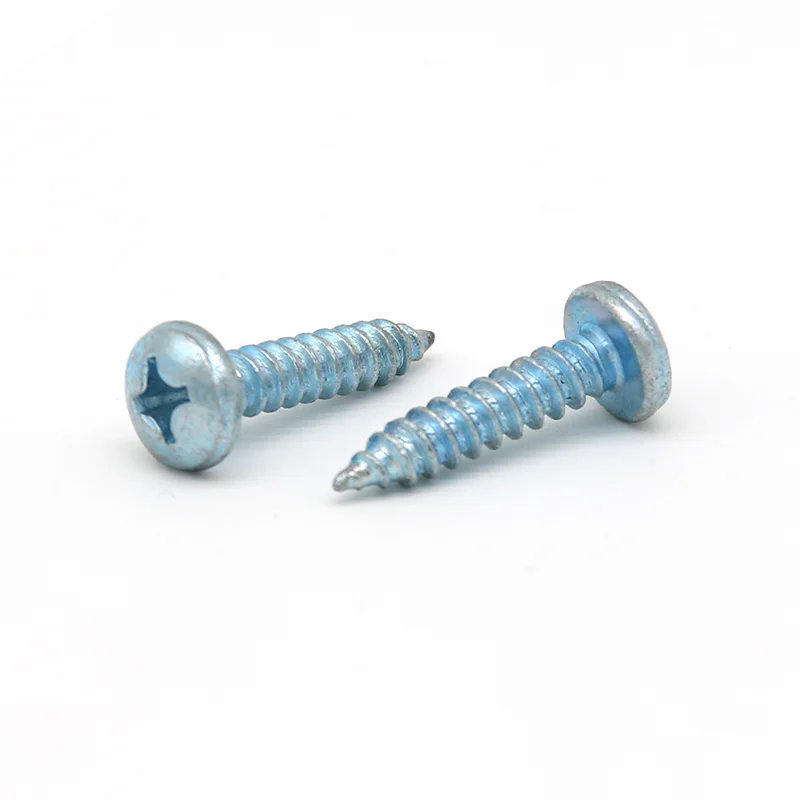
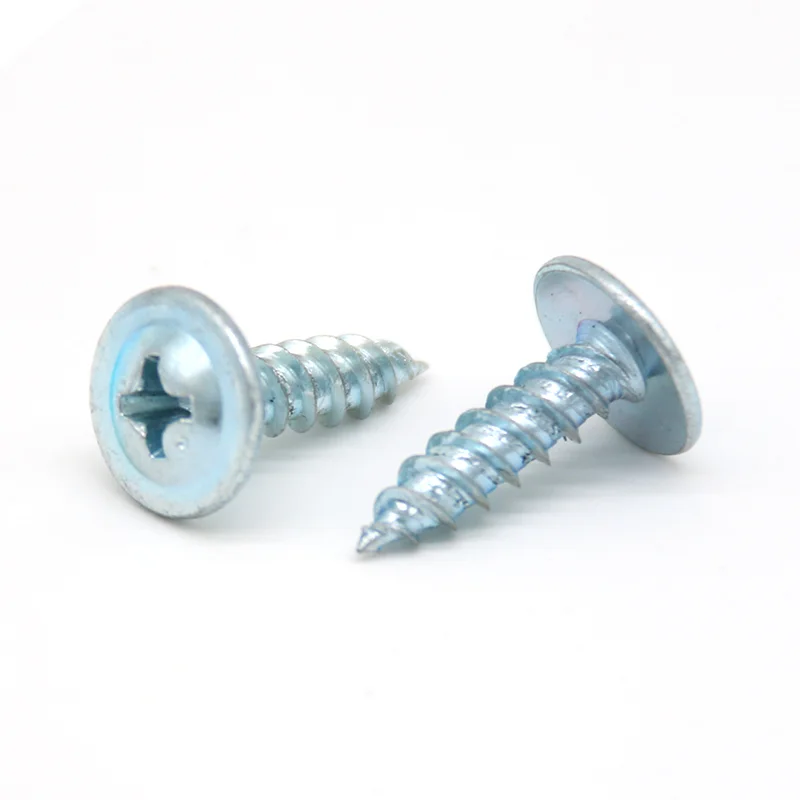
Match the thread type and pitch to the joining materials, such as metal sheets, timber, or a pre-tapped metal part. |
A thread suited to the wrong material can reduce holding power, cause poor engagement, or damage the assembly during tightening. |
Provide the material thicknesses and ask whether the screw is intended for a clearance hole, pilot hole, or threaded hole. |
| Length and usable engagement |
Compare the specified length with the grip thickness, washer or bracket thickness, and the required thread engagement beyond the joint. |
An undersized screw may not develop enough engagement, while an overly long screw can interfere with components or protrude from the assembly. |
Send a joint cross-section or state the total clamped thickness before selecting the length. |
| Point design and installation method |
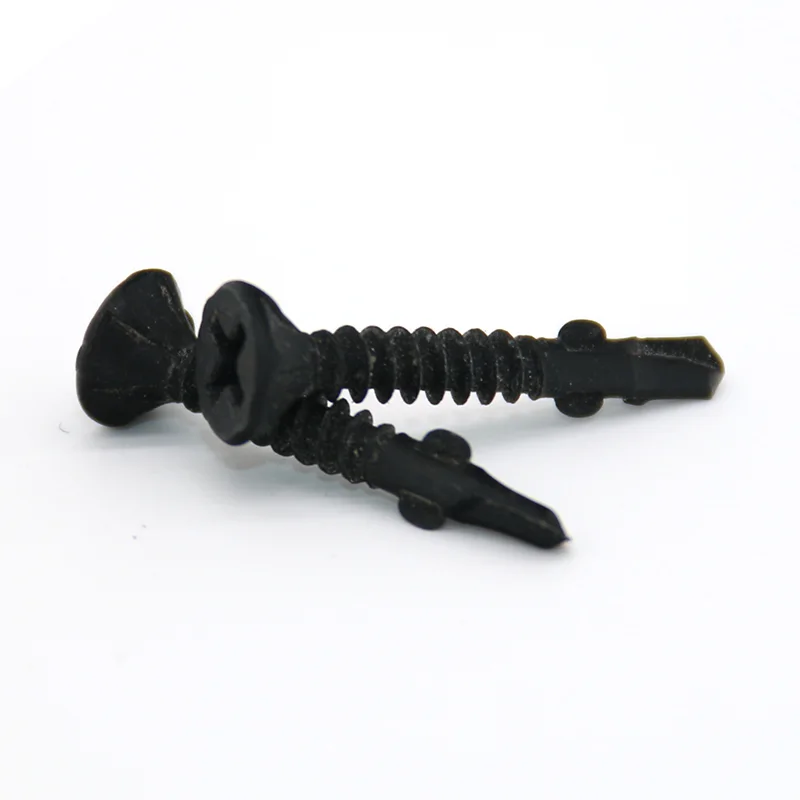
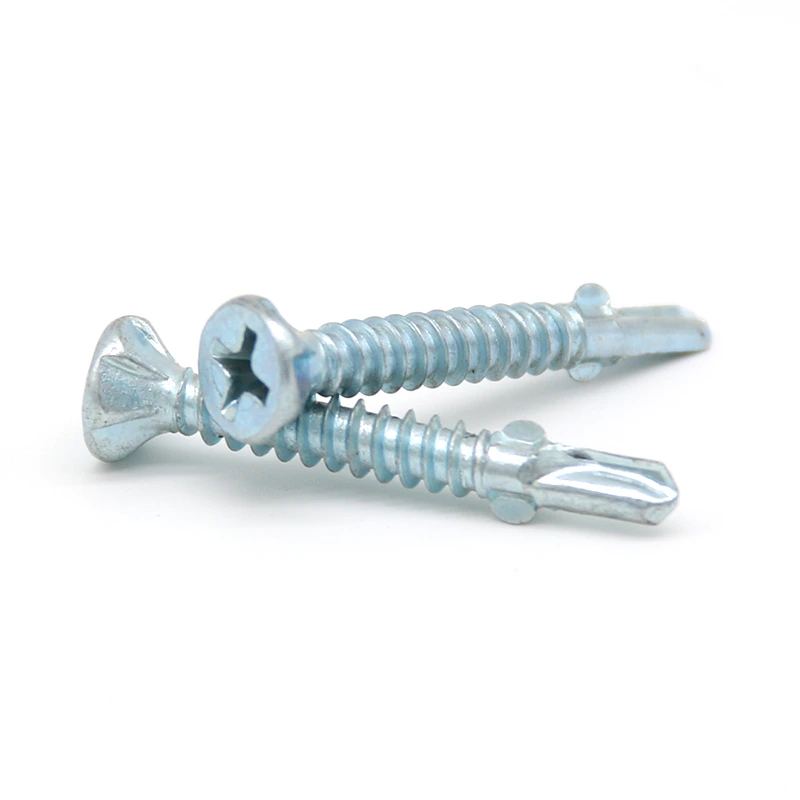
Check whether the screw has a standard, sharp, drilling, or other point suited to the planned hole preparation and substrate. |
The point affects whether a pilot hole is needed, how easily the screw starts, and the risk of splitting or deforming the material. |
Ask for a sample or drawing and confirm the recommended installation method for the actual substrate. |
| Material and surface finish |
Confirm the base material, coating or plating, colour requirements, and compatibility with the surrounding materials and environment. |
Material and finish affect corrosion behaviour, appearance, galvanic compatibility, and suitability for indoor or exposed use. |
Describe the installation environment and ask which finish and inspection information will be supplied for the specified screw. |