Hole Saw Machine Selection Guide | Hebei Wotu Fastener Manufacturing Co., Ltd.

Choosing a Hole Saw Machine for Metal Parts

A hole saw machine is usually bought for one practical reason: making clean, repeatable circular holes in sheet metal, tube, pipe, panels, or assembled parts without slowing the line down. The right choice depends less on the name of the machine and more on the material, hole diameter range, production volume, and how accurately each hole must be positioned.

For buyers working around fasteners, brackets, frames, enclosures, or installation hardware, the key decision is whether the work needs a dedicated drilling station, a portable magnetic drill with hole saws, a bench machine, or a more automated setup. Each option changes labor time, fixture design, hole quality, and tooling cost.

Related Products

U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

Brand: Wotu Surface: natural black oxide / hot-dip galvanized / blue-white zinc plated, multiple processes available Specifications: Based on common industry drawing parameters, suitable for pipe diameter 25mm~139.7mm, screw diameter M10~M24, total length can be nonstandard customized Matching: can be matched with nut, flat washer and spring washer of the same specifications for complete shipment Packaging: Bundling and packaging + 25kg export carton, full-container wooden pallet wrapped with film, supports private-label export packaging

Read More
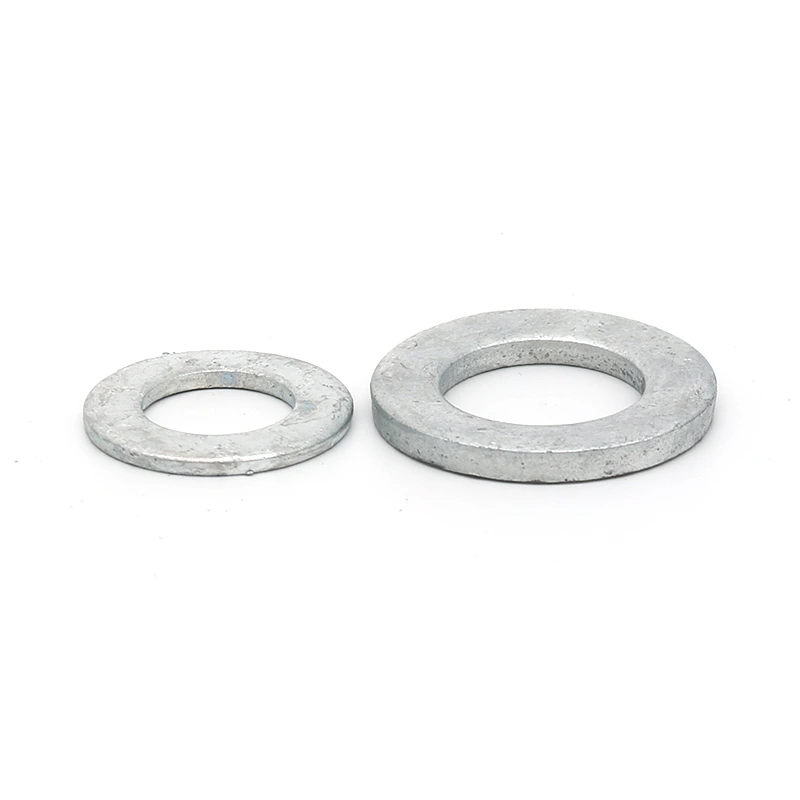
Hot-Dip Galvanized Chinese National Standard Flat Washer (GB/T97.1A Level Flat Washer)

Hot-Dip Galvanized Chinese National Standard Flat Washer (GB/T97.1A Level Flat Washer)

Brand: Wotu Surface: overall hot-dip zinc plated anti-corrosion treatment, optional blue-white zinc plated, color zinc plated, black oxide Specifications: Execute GB/T97.1-2002 Chinese national standard, in stock M6-M64 full range of specifications, inner diameter, outer diameter, thickness strictly comply with Chinese national standard parameters, support nonstandard size customized Packaging: 25kg woven bag / export carton packaging, full pallets wrapped with film, supports private-label customization

Read More
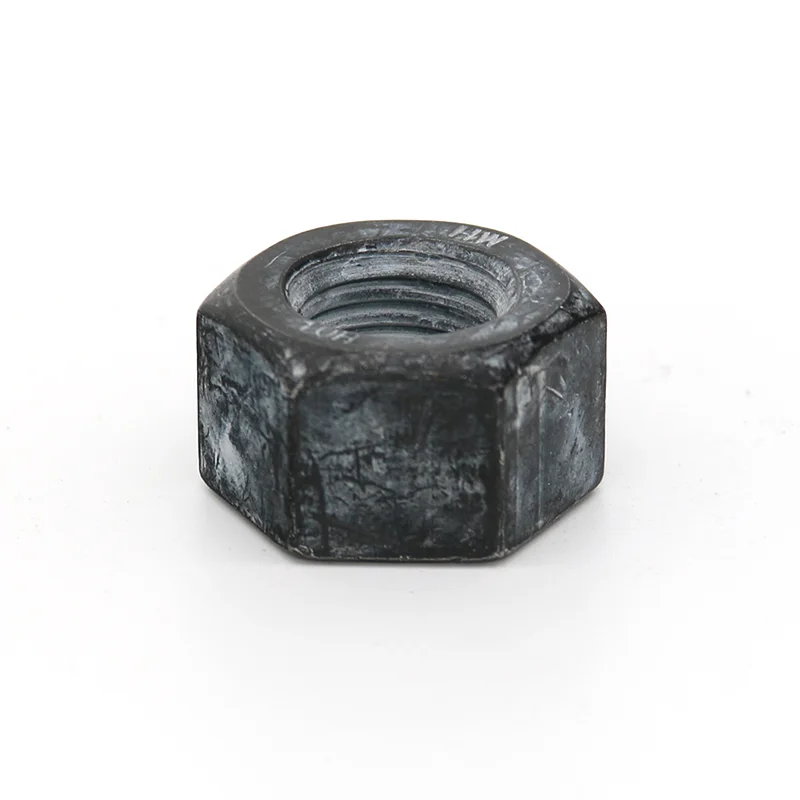
Grade 8/Grade 10 High-strength Black Oxide Hex Nut (DIN934/GB Chinese National Standard Thickened Nut)

Grade 8/Grade 10 High-strength Black Oxide Hex Nut (DIN934/GB Chinese National Standard Thickened Nut)

Brand: Wotu Surface: quenching and tempering heat treatment + high temperature black oxide anti-rust treatment Specifications: Comply with DIN934, GB/T6170 standards, in stock M6-M48 full range of specifications, nonstandard sizes can be customized Packaging: 25kg carton/woven bag inner packaging, whole wooden pallet wrapped with film for export packaging, supports neutral/private-label customization packaging

Read More
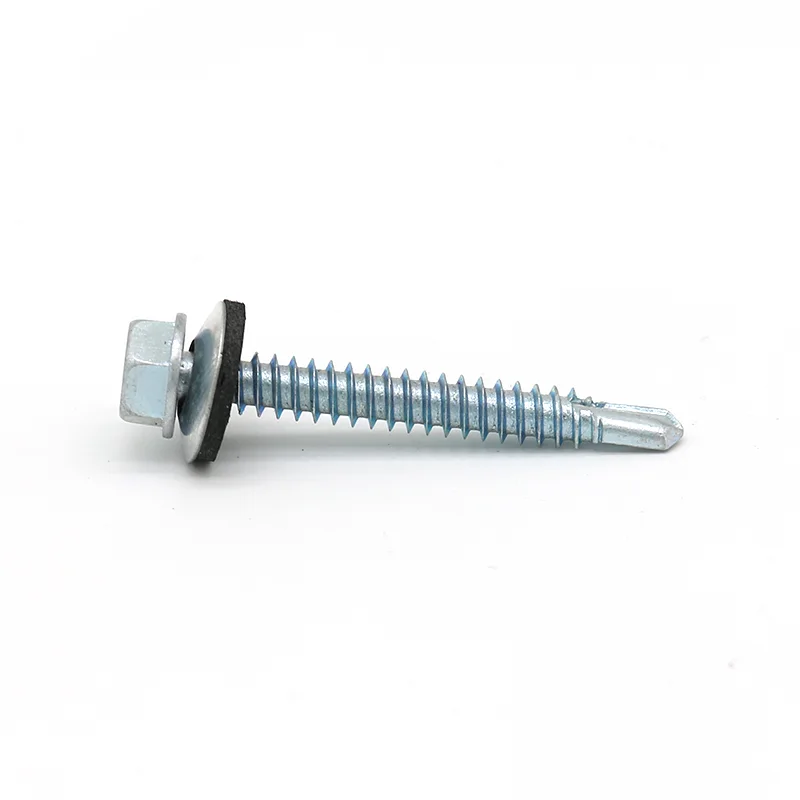
Hex Head Self-Drilling Screw With Bonded Washer

Hex Head Self-Drilling Screw With Bonded Washer

Brand: Hengzuan Surface: blue and white zinc plated, color zinc plated can be customized on request Specifications: in stock 4.2/4.8/5.5/6.3mm mainstream wire diameter, length 20mm~165mm full range of specifications, nonstandard rod length, drill point size can be customized Packaging: 25kg export cartons, full pallets wrapped with film, supports neutral export packaging, customer private-label customization

Read More
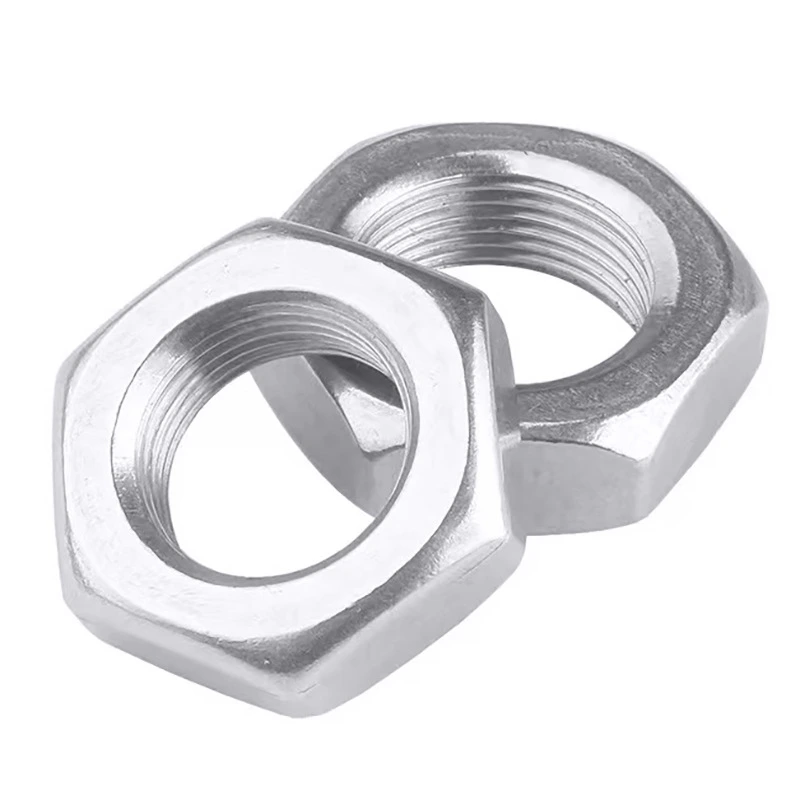
Hex thin nut

Hex thin nut

Brand: Wotu Surface: zinc plated Specifications: in stock M8~M64 full standard specifications, covering precision, machinery, and steel structure full size range, supporting nonstandard tooth pitch and customized thickness Matching: Can be matched with bolts of corresponding specifications, flat washer, spring washer complete set of shipment Packing: packed in 25kg cartons and packed on wooden pallets.

Read More
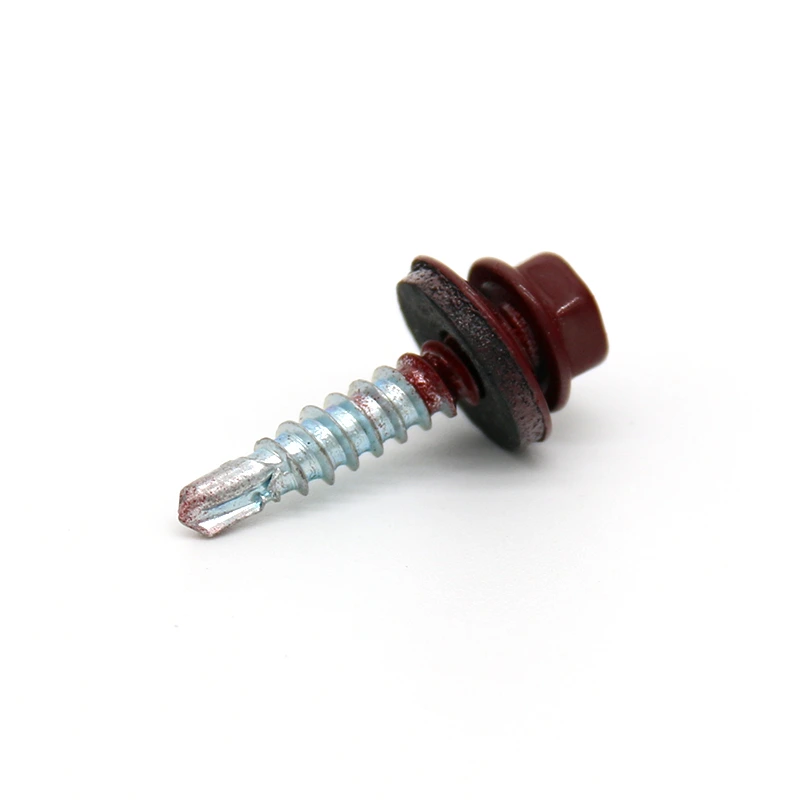
Painted Hex Head Self-Drilling Screw

Painted Hex Head Self-Drilling Screw

Brand: Hengzuan Surface: screw color zinc plated + hex head outdoor paint Specifications: ST5.5, ST6.3, rod length 25mm~120mm in stock, supports nonstandard customization, suitable for drilling steel sheets 2~5mm Packaging: 25kg cartons, whole wooden pallets

Read More

Choosing a hole saw setup for metal parts and hardware production

Hole-making selection notes

Compare hole-making options by workpiece material, hole diameter range, required accuracy, clamping method, tooling compatibility, and how often cutters must be changed. A suitable setup should hold the part securely, guide the cutter straight, and support the operator’s normal production rhythm without excessive marking, rework, or tool wear.

Criterion What To Check Why It Matters Buyer Tip
Hole diameter range and arbor compatibility Confirm the smallest and largest hole saw sizes the machine can run, and check the arbor or adapter style required. A mismatch can cause poor centering, wobble, damaged cutters, or the need for extra adapters before production can start. What hole diameters, arbor types, and cutter brands do you need the machine to support?
Material and thickness to be cut Match the machine setup to the workpiece material, thickness, and expected hole depth rather than only the cutter diameter. Thin sheet, pipe, plate, wood, plastic, and stainless steel place different loads on the cutter and drive system. Ask what material grades and thicknesses the supplier expects the machine to cut regularly.
Feed control and cutting stability Compare whether the machine uses manual feed, controlled feed, or fixture-assisted cutting, and look at how the workpiece is clamped. Stable feed and firm clamping reduce chatter, tooth breakage, oval holes, and operator fatigue. Can the supplier explain how the machine holds the workpiece and controls pressure during cutting?
Coolant, chip removal, and cutter life Check whether the process needs coolant, lubricant, chip clearance, or pauses between cuts for the materials you plan to drill. Heat and packed chips shorten hole saw life and can leave rough edges or seized cutters. Ask what coolant or lubrication method is recommended for your material and production volume.
Production use versus occasional cutting Define expected daily hole count, changeover frequency, and the number of hole sizes used in one shift. A machine that works for maintenance jobs may be slow or inconsistent for repeated production cuts. Share your typical batch size and hole pattern so the supplier can recommend the right drive power, fixture, and setup style.

What to confirm before selecting a hole saw machine

The main distinction is between a machine that simply drives a hole saw and a process that controls the whole cut. A basic drill setup may be enough for occasional holes in thin material, but repeated holes in metal parts need stable clamping, correct spindle speed, suitable coolant or lubrication, and a way to clear chips. Without those controls, hole saw teeth wear quickly and the finished hole can become oversized, rough, or off-center.

Buyers should also separate hole saw cutting from punching, laser cutting, and core drilling. Hole saws are useful when tooling flexibility matters and hole sizes change, but they are not always the fastest method for high-volume flat sheet work. If the same hole repeats thousands of times in the same material, a punch tool or dedicated fixture may be more economical. If the part is already fabricated or too large for a press, a hole saw machine can be the more practical choice.

Start with the workpiece, not the machine label. Confirm the material type, thickness, shape, and whether the part can be clamped flat. A machine that performs well on light-gauge sheet may struggle with thicker plate or curved tube unless it has enough rigidity and a proper fixture. For stainless steel or harder alloys, tool speed control and lubrication become more important than raw motor power alone.

Match the setup to the hole pattern. Occasional maintenance holes can often be handled with a portable or bench-mounted system. Repeated holes in brackets, frames, or production parts need stops, guides, jigs, or a positioning table so operators do not mark and measure every piece by hand. The fixture can affect output as much as the machine itself.

Avoid choosing only by maximum hole size. Large diameter capacity matters, but the common hole sizes, edge distance, burr expectations, and acceptable tolerance usually decide whether the machine will be efficient. Buyers also overlook arbor compatibility, pilot drill replacement, chip removal, and the cost of consumable cutters. These details affect downtime and per-hole cost.

Before requesting a quote, prepare a sample drawing or a short process description. Include the material, thickness, hole diameter range, number of holes per part, expected batch size, and whether the workpiece is flat, tubular, or already assembled. If Hebei Wotu Fastener Manufacturing Co., Ltd. is being asked to support a related fastener or fabrication requirement, confirm whether the inquiry concerns equipment supply, machined parts, compatible fasteners, or a complete production process.

Criteria Importance Description Example Options
Workpiece shape and clamping Critical for hole position and cutter life Flat sheet, tube, formed brackets, and assembled parts need different support methods. If the part moves or flexes during cutting, the hole can become oversized or off-center. A flat mounting plate may work with a simple stop and clamp, while a round tube may need a shaped fixture to prevent rotation.
Material and thickness Strongly affects speed, lubrication, and tooling choice Harder or thicker materials usually require more rigid control, slower cutting speeds, and better lubrication than thin mild steel or light-gauge material. A setup used for thin panel holes may not be the right choice for repeated holes in thicker stainless components.
Production volume Determines whether flexibility or cycle time matters more Low-volume work may favor a flexible drill or bench setup. Repeated production may justify fixtures, stops, positioning tables, or a different hole-making process. A maintenance team cutting occasional access holes has different needs from a shop making the same bracket in batches.
Hole size range and changeover Important for tool cost and downtime A machine should match the common hole diameters, not only the largest possible size. Frequent diameter changes require easy cutter replacement and compatible arbors. A buyer cutting several standard fastener-clearance holes should check the everyday cutter sizes and pilot drill replacements.
Alternative process fit Can change the total cost per hole Hole saw cutting is useful for flexibility and formed parts, but punching, laser cutting, or other machining may be better for certain materials, tolerances, or volumes. A flat sheet with thousands of identical holes may suit punching, while a fabricated frame may be more practical to drill with a guided hole saw setup.

Product Selection

Related Options

For a production line making metal brackets, mounting plates, frames, or hardware with repeated circular openings, the priority is a stable and repeatable cutting process. The most useful option is the one that matches the part geometry and batch size, keeps the hole position consistent, and uses cutters that are easy to replace when the material or hole diameter changes.

Blog Articles / Reviews

Frequently Asked Questions

Is a hole saw setup suitable for thick metal plate?

It can be suitable, but thickness changes the decision quickly. Thicker plate needs a rigid machine, secure clamping, correct cutter speed, lubrication, and enough chip clearance; otherwise the cutter may overheat, wander, or leave a rough hole. For very thick or high-precision work, another process may be more efficient.

How does this compare with punching or laser cutting?

A hole saw is flexible when hole sizes change, parts are already formed, or production volume does not justify dedicated tooling. Punching is often faster for repeated holes in flat sheet, while laser cutting can handle complex profiles without a physical cutter. The best choice depends on batch size, material, tolerance, and whether the part can be placed in the required machine.

Does a larger maximum hole size mean a better machine?

Not by itself. Buyers often focus on the largest advertised diameter and miss the sizes they cut every day, the material thickness, arbor compatibility, and how firmly the part can be held. A smaller, more rigid setup with the right fixtures may produce better results than a larger machine used near its limit.

What information should be shared before asking for a recommendation?

Provide the material, thickness, hole diameter range, hole quantity per part, expected batch size, and workpiece shape. A simple drawing or photo is useful because tube, plate, brackets, and assembled parts all create different clamping and access issues.

Can one machine handle different hole diameters?

Often yes, if the spindle, arbor, and cutter system support the required range. The trade-off is changeover time, cutter inventory, and the need to adjust speed or lubrication for different materials and diameters. Confirm cutter compatibility before assuming all sizes will run on the same setup.

Leave Your Message

Share the workpiece material and thickness, the hole diameter range, and the expected batch size or holes per part. If the part is tube, plate, bracket, or an assembled component, mention that too so the clamping and tooling requirements can be checked.