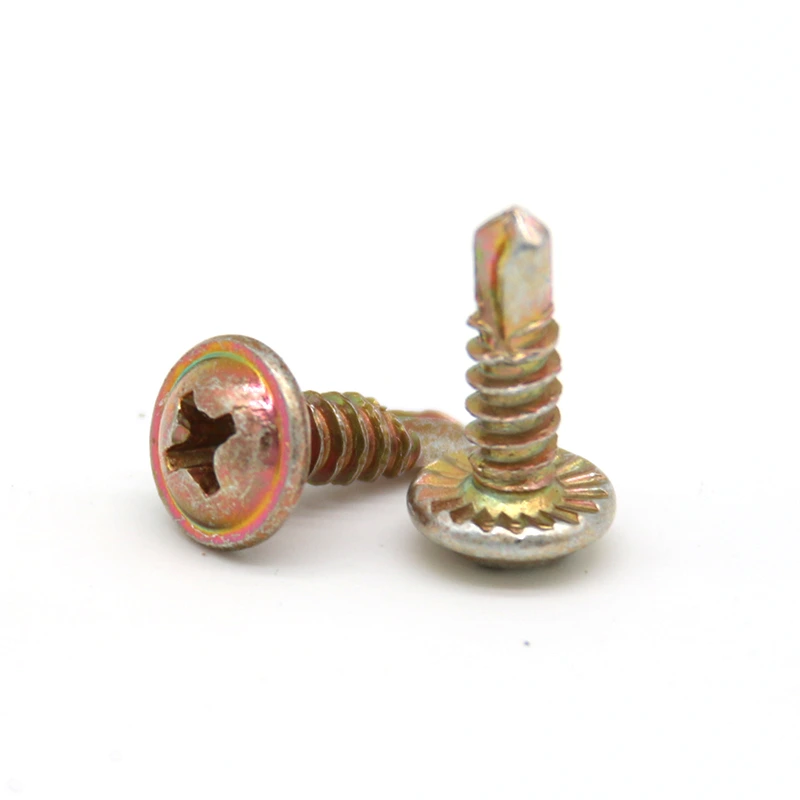
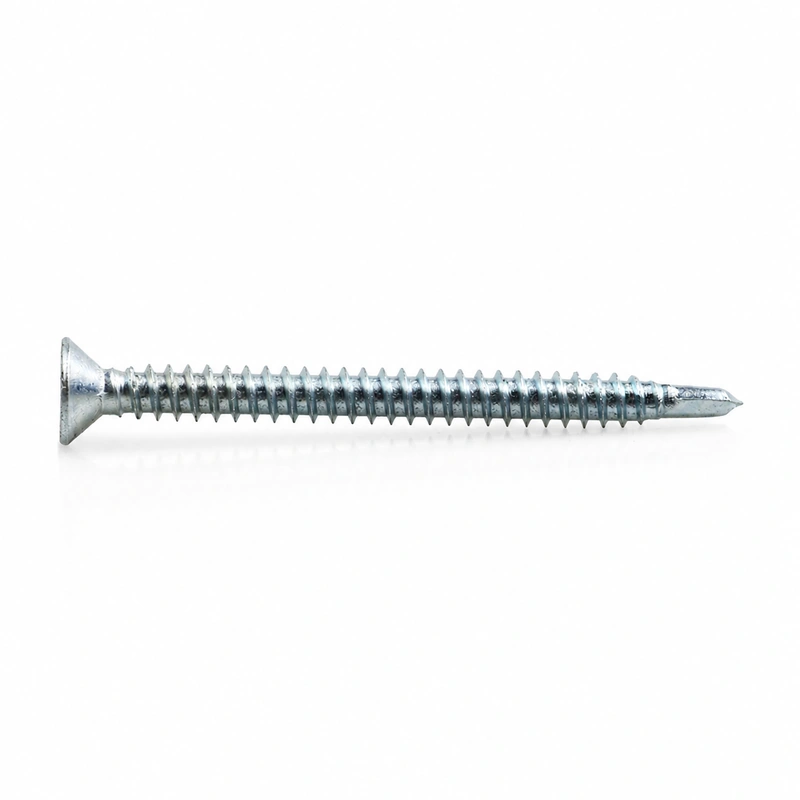
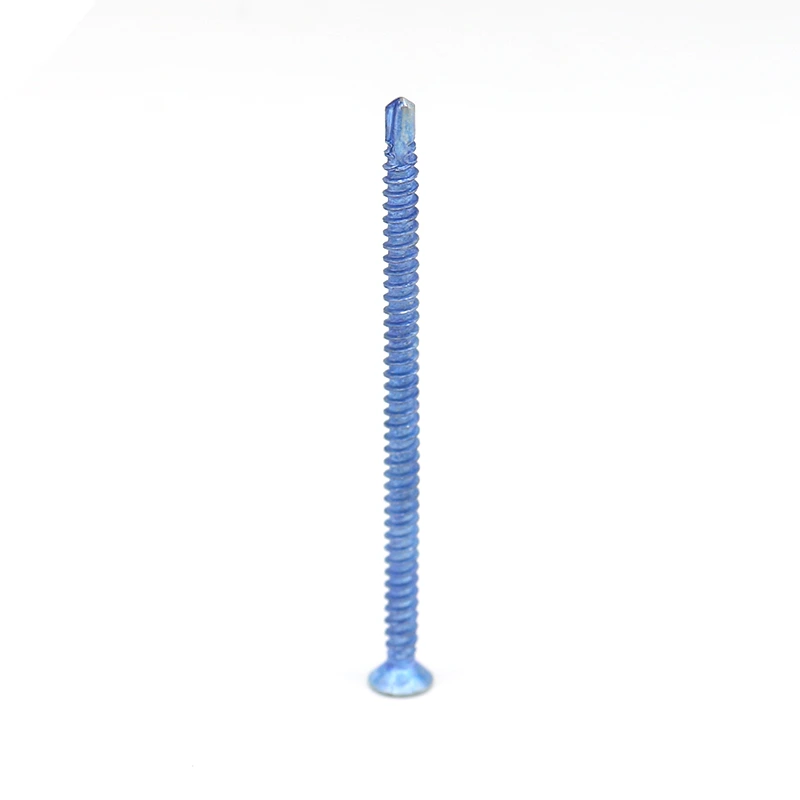
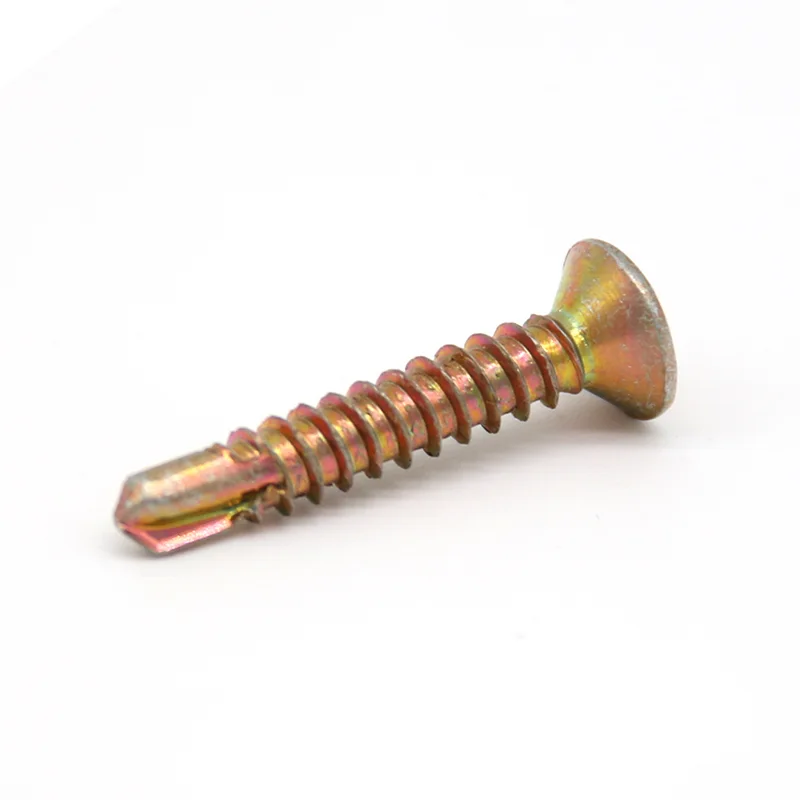
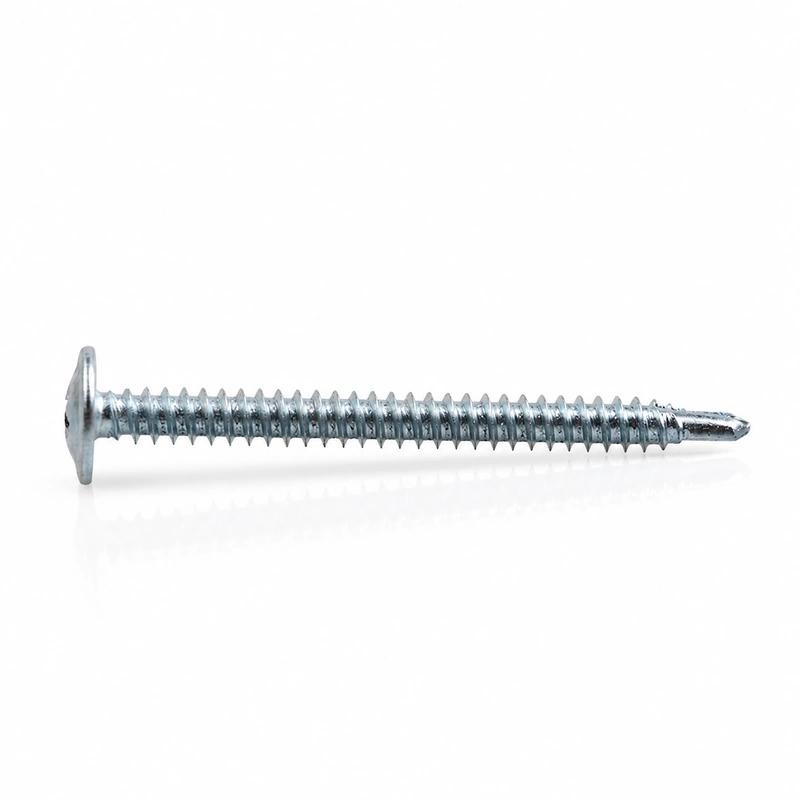
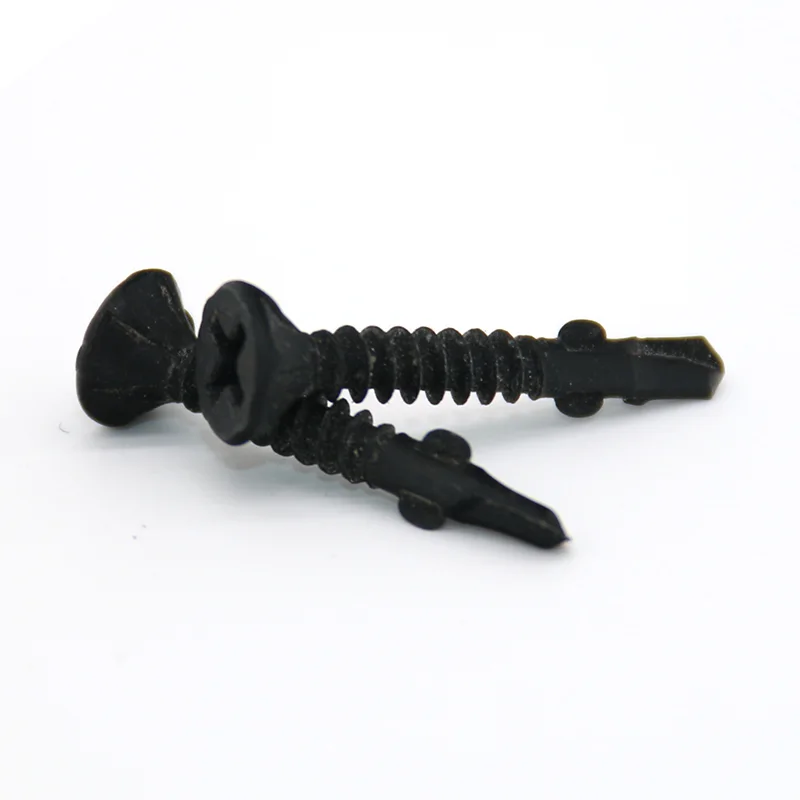
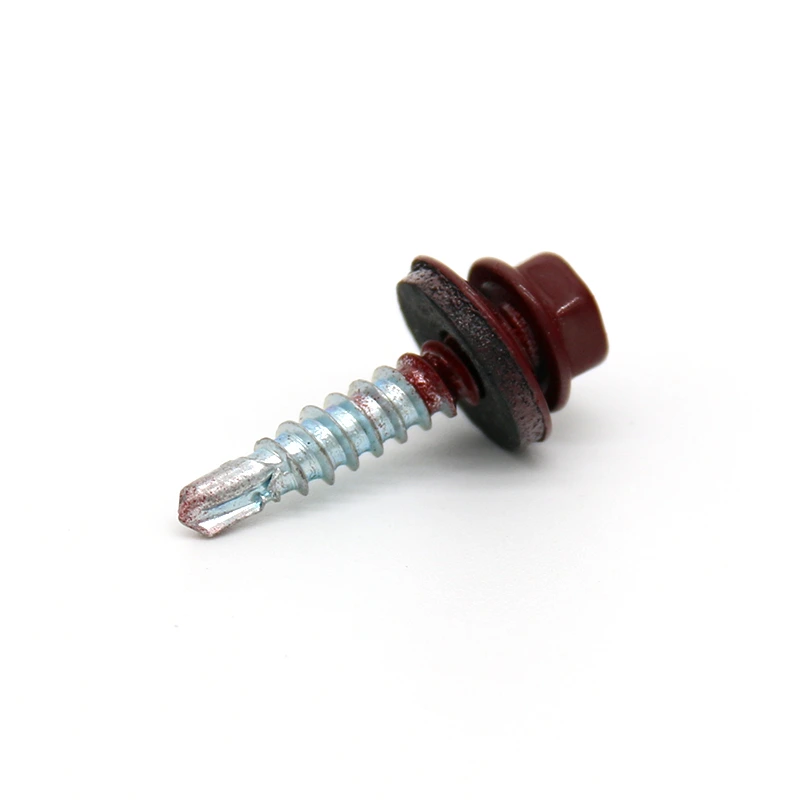
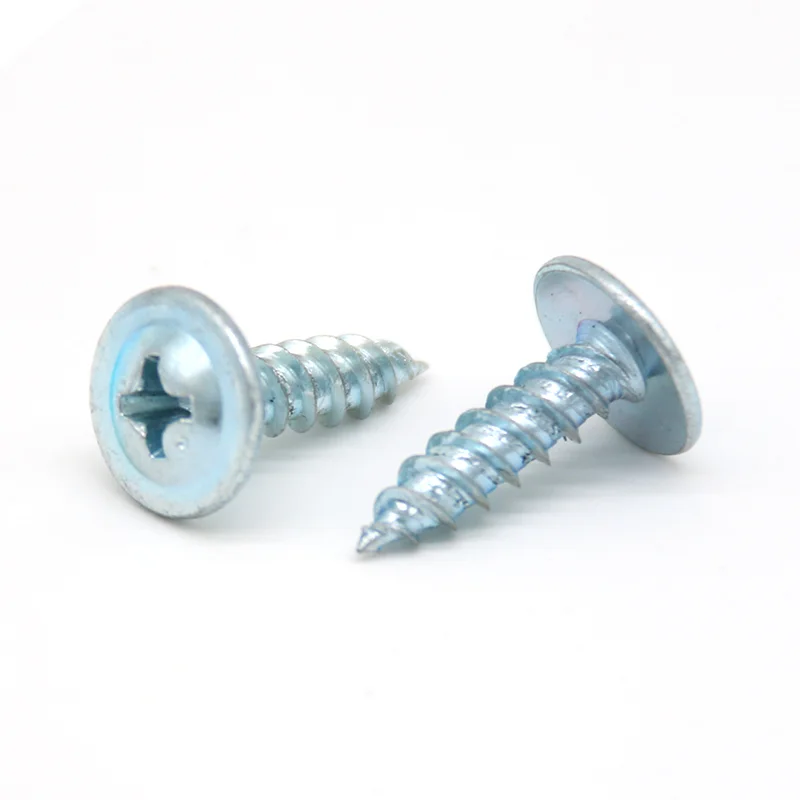
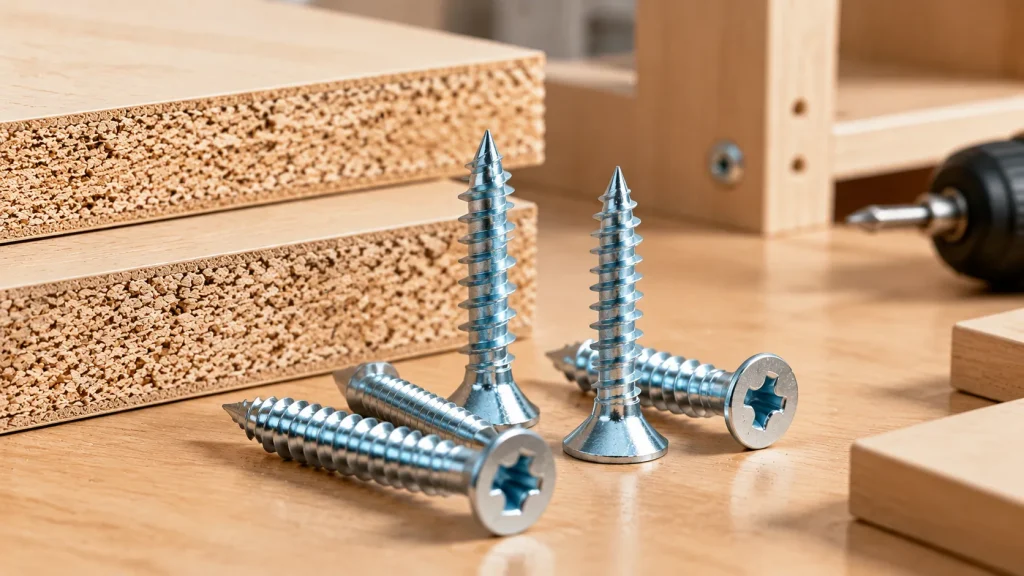
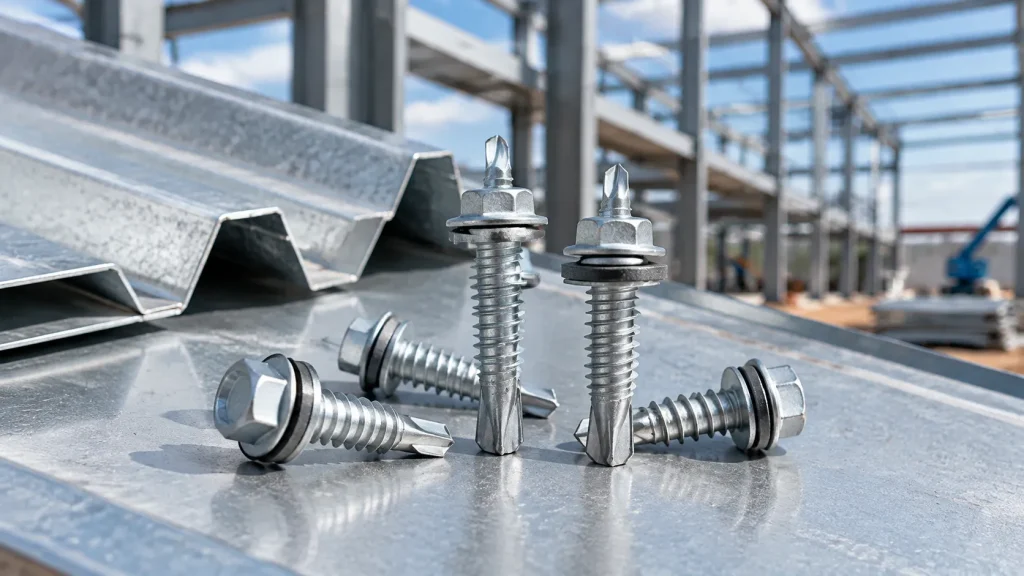
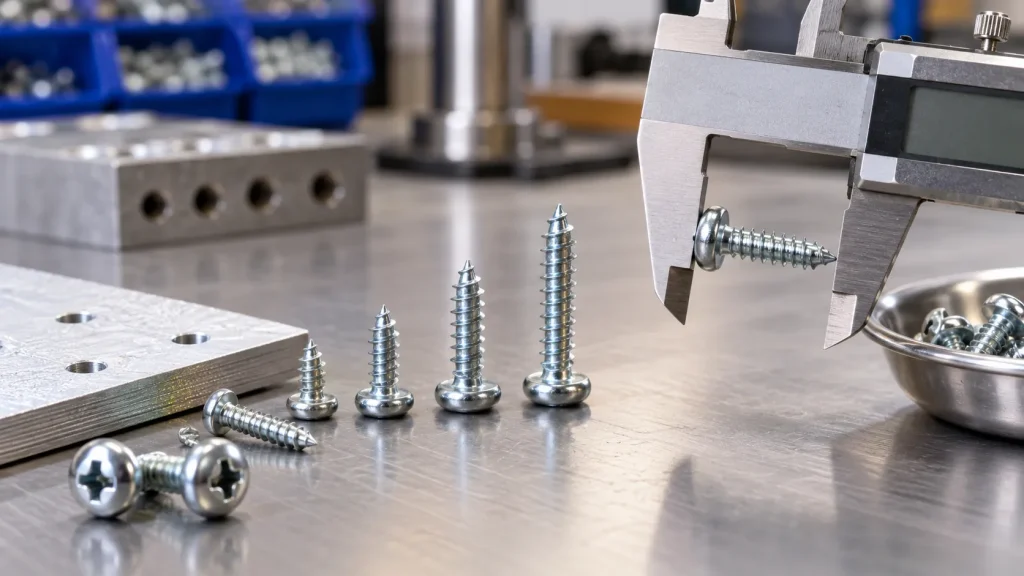
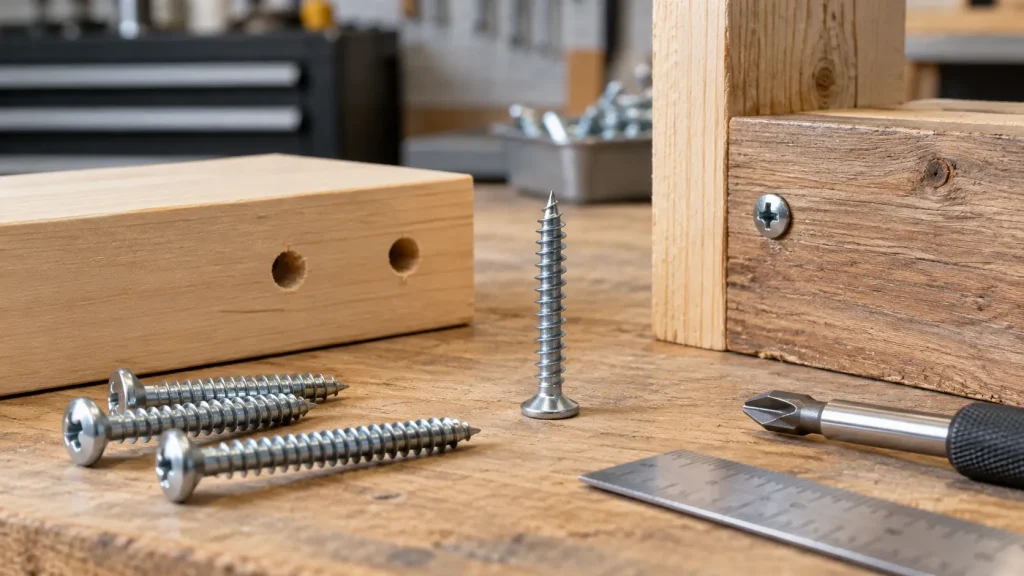
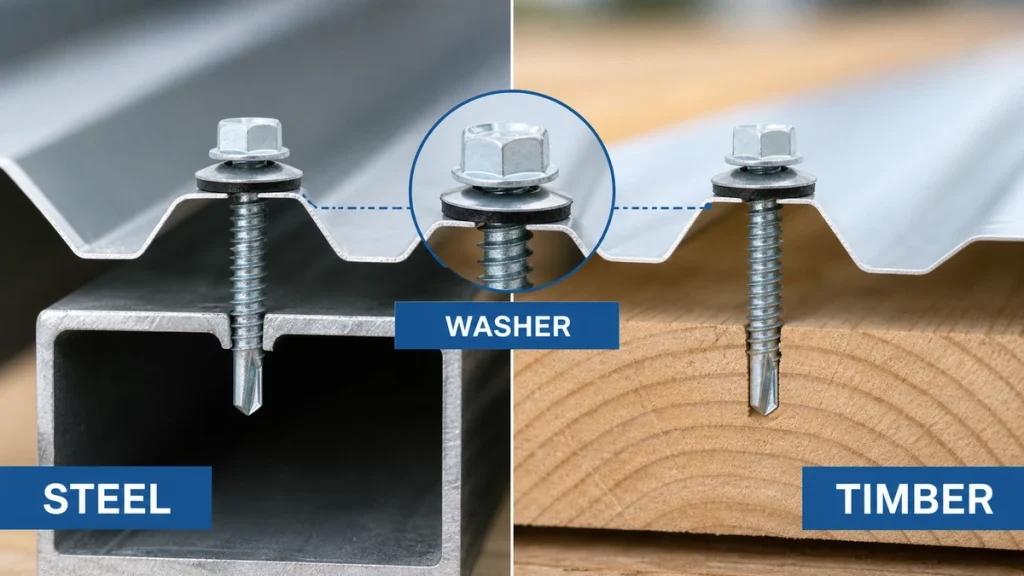
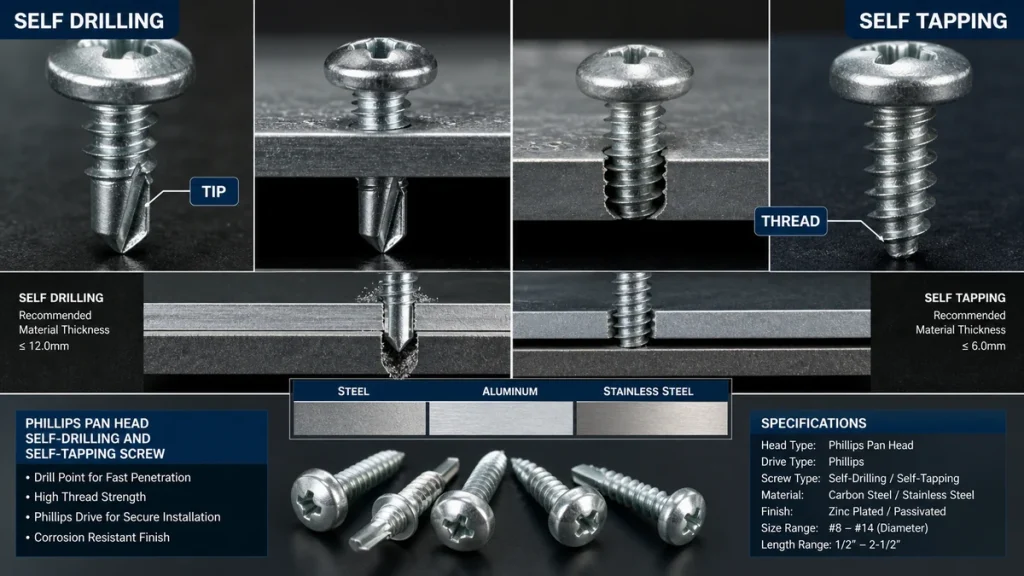
The practical distinction is whether the screw needs to drill, tap, or only fasten into a prepared hole. A self-drilling screw uses a drill point to cut its own hole in suitable metal; a self-tapping screw forms or cuts threads after a pilot hole or prepared opening; a wood or fiberboard screw relies on thread shape and holding power in softer material.
This matters because the point and thread design affect installation speed, pull-out resistance, risk of splitting, and surface finish. If “HP screw” appears on a bill of materials, confirm the drawing or sample before treating it as a standard product name.
Start with the joint: metal-to-metal, metal-to-wood, panel-to-frame, furniture board, or another assembly. The substrate decides whether the screw should have a drill point, tapping thread, coarse wood thread, or a thread form intended for board material.
Check the head style against the finished surface. A countersunk head sits flush when the material and hole preparation allow it; a hex head gives stronger tool engagement; a pan or wafer head can spread load on thinner sheets. Choosing the wrong head often causes poor seating before the screw ever reaches its holding limit.
Define length by the total material stack and required thread engagement, not by habit. Too short gives weak holding; too long can protrude, damage hidden layers, or slow installation. If a pilot hole is used, confirm the pilot hole practice together with screw diameter and thread type.
Do not leave coating and environment until the end. Indoor furniture, dry interior metalwork, and exposed roofing each place different demands on corrosion resistance and appearance. For an inquiry, send the application, material stack, drawing or sample photo, required head and drive type, coating preference, and any packaging or inspection requirements.