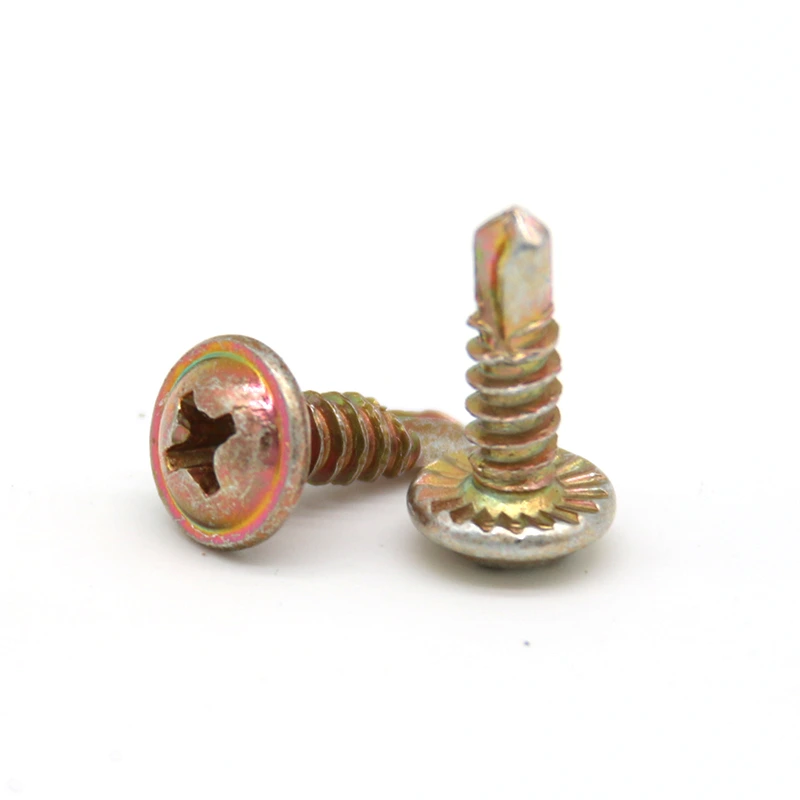
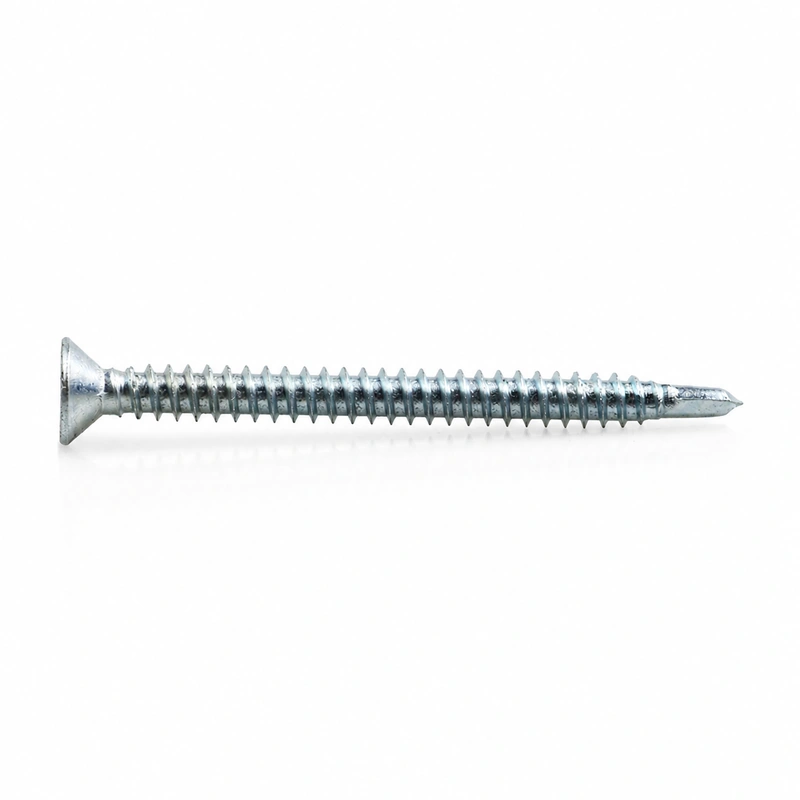
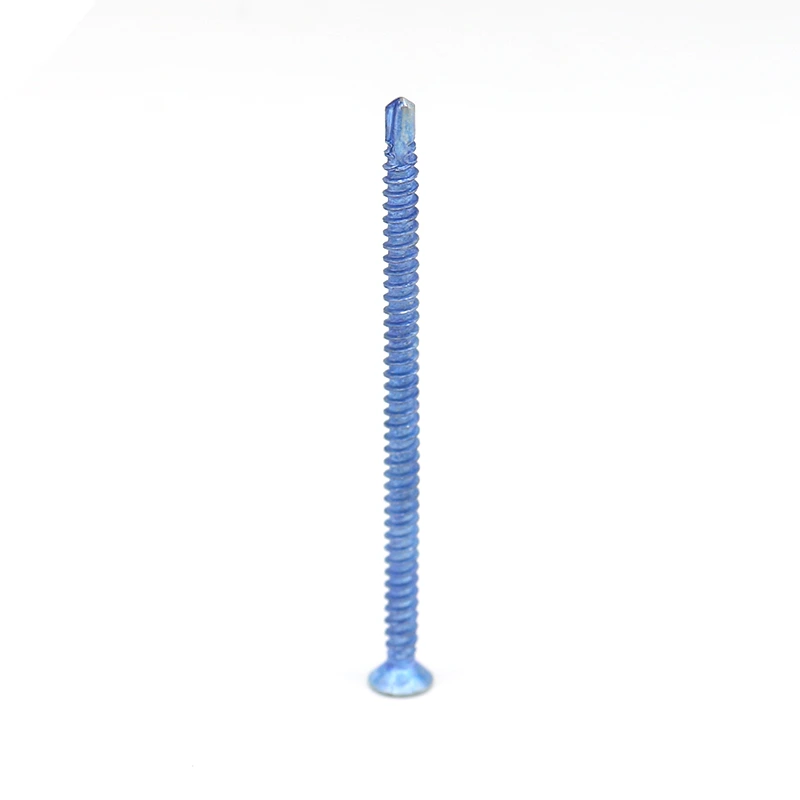
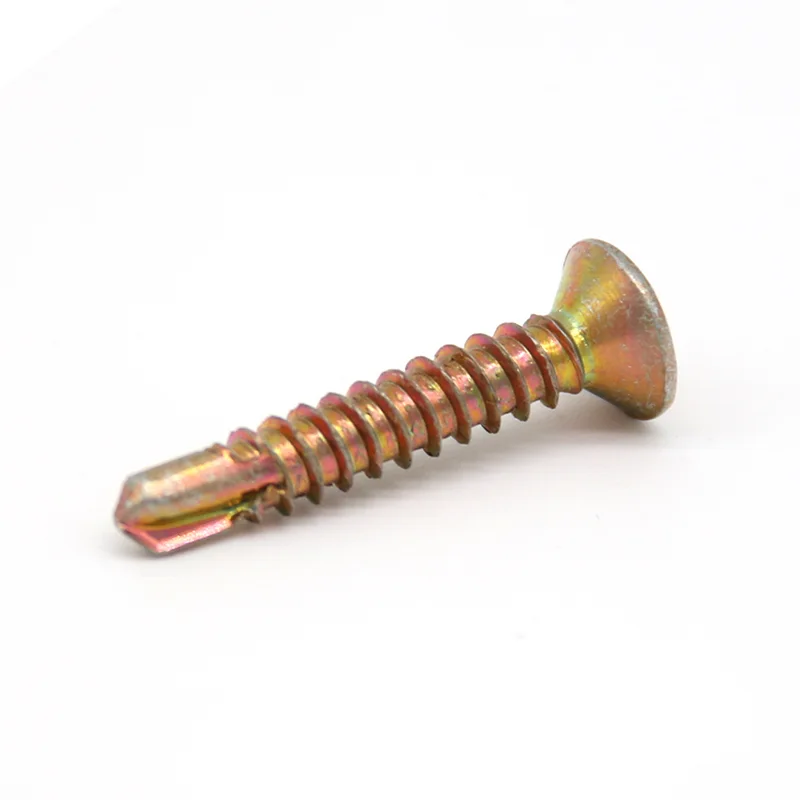
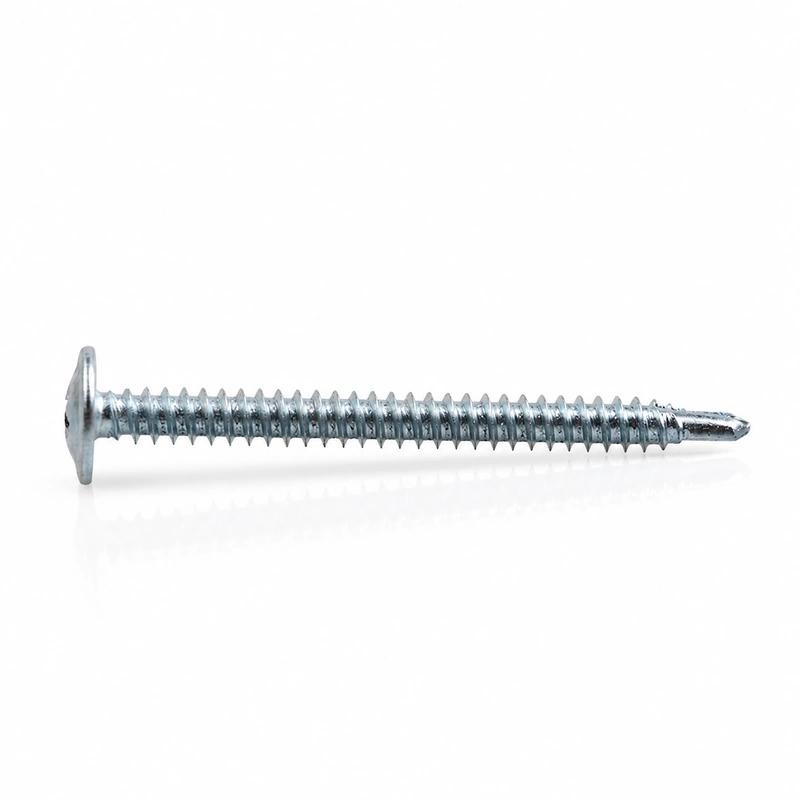
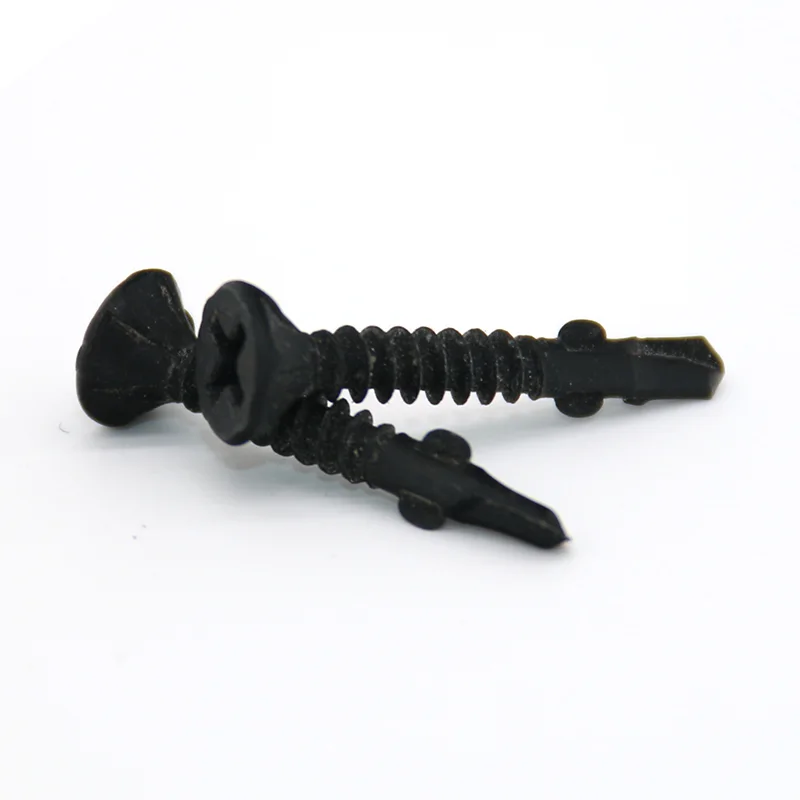
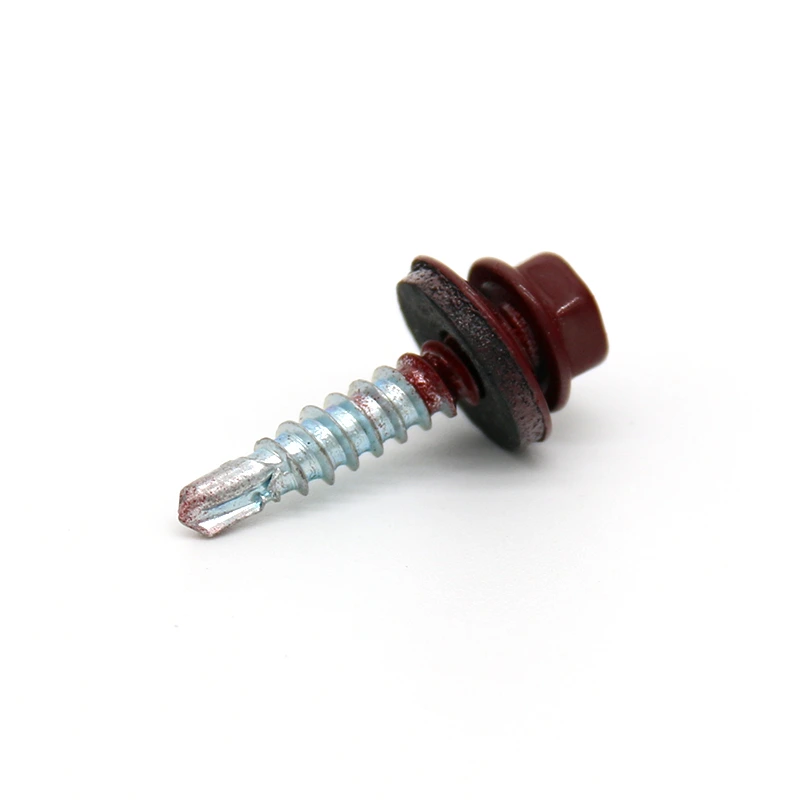
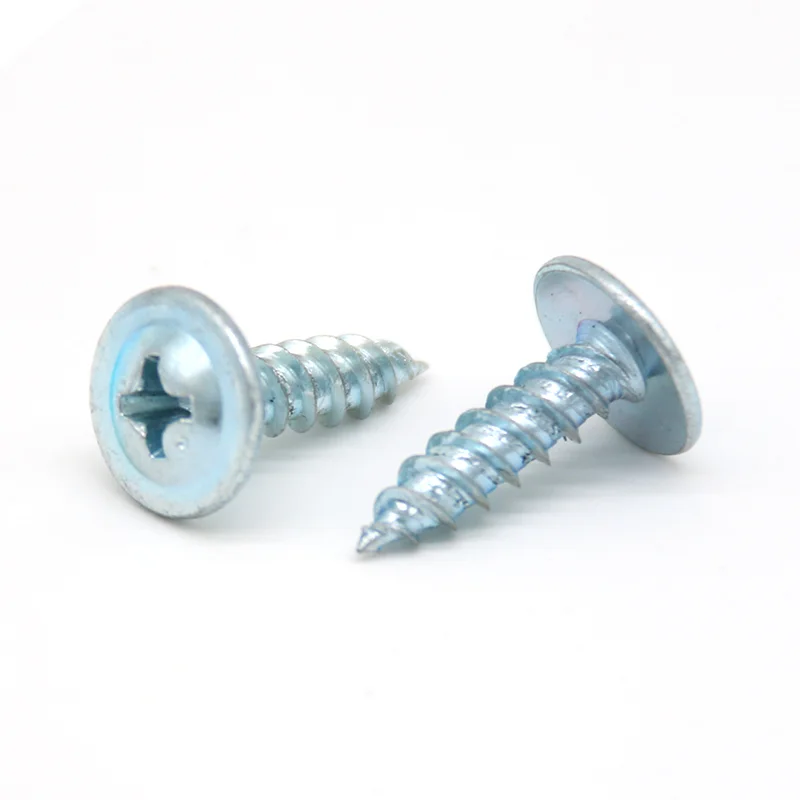
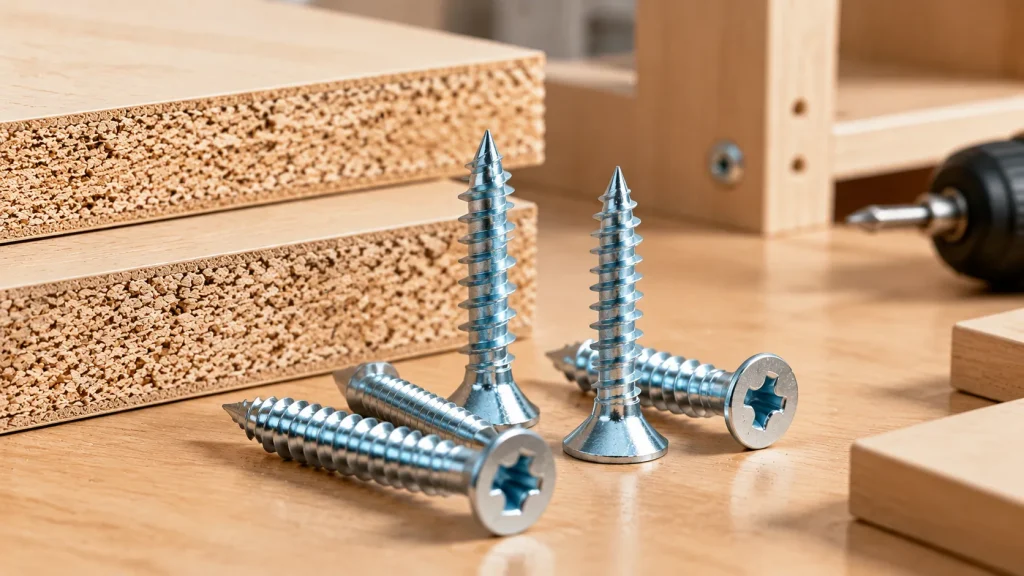
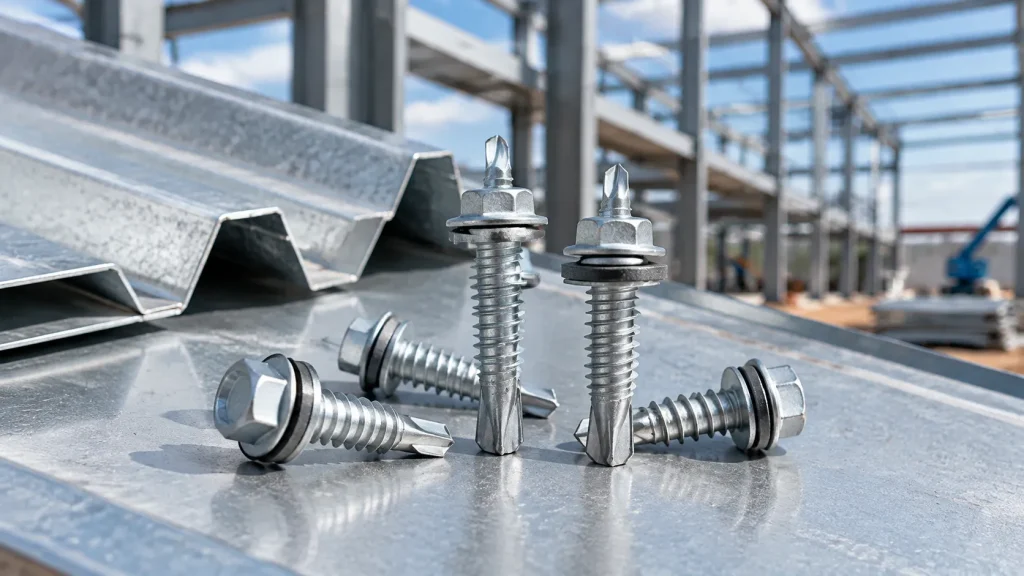
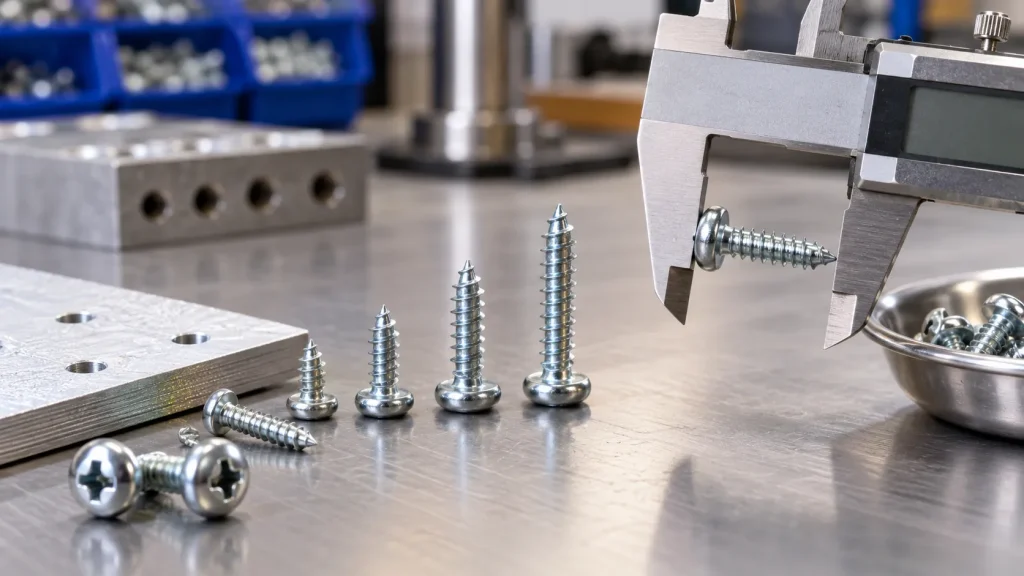
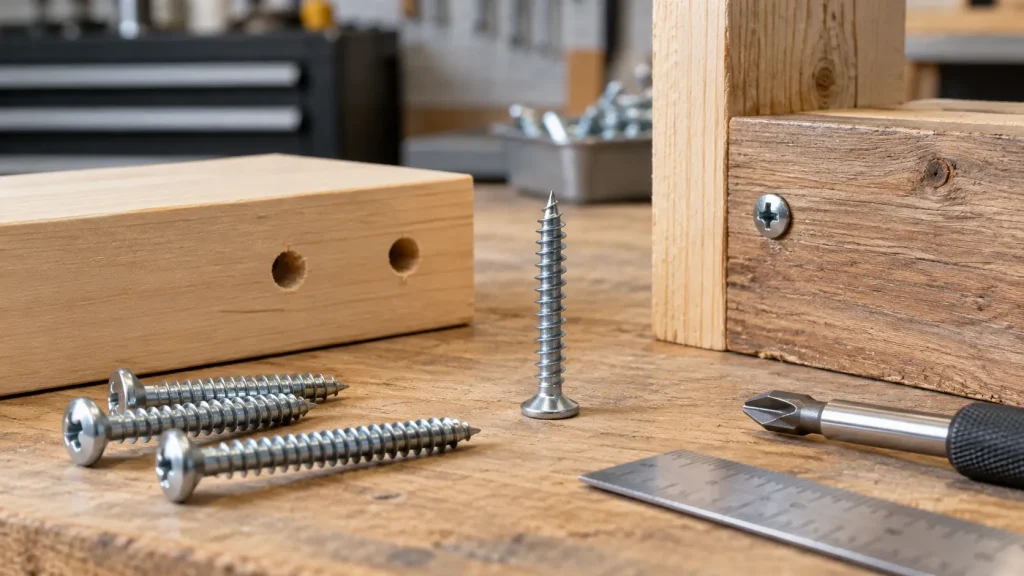
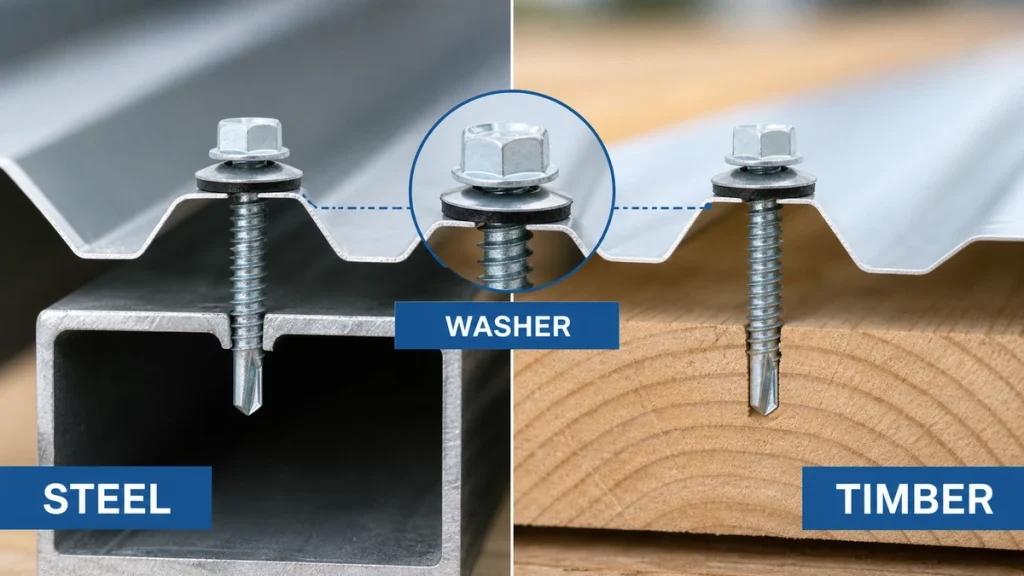
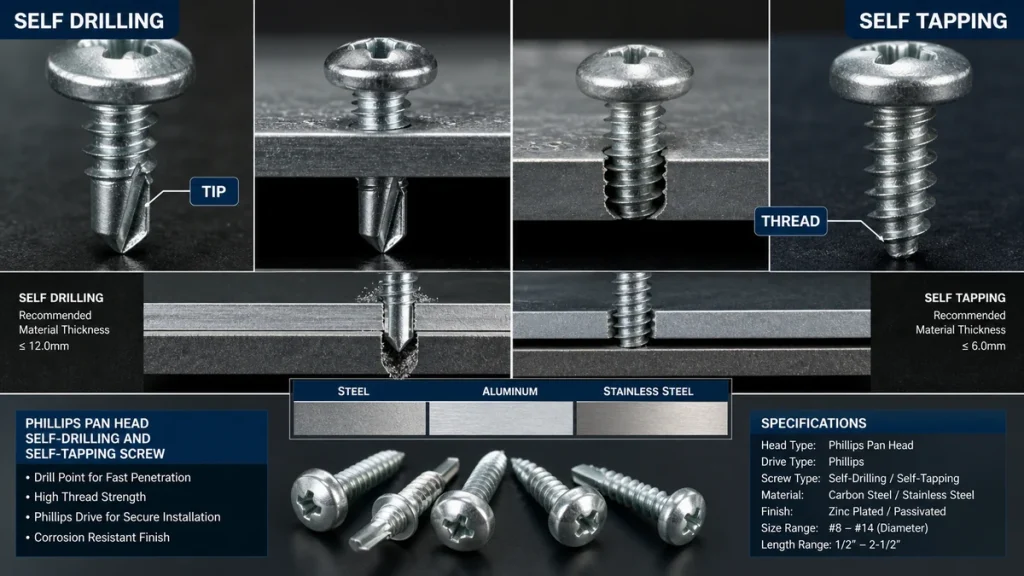
The most important distinction is between screws that cut into a prepared hole and screws designed to drill their own hole. Self-tapping screws form or cut threads in the receiving material, but they usually depend on the correct pilot hole. Self-drilling screws include a drill point, so the point style, drilling capacity, and material stack become part of the selection.
This matters because the wrong type can fail before the screw is fully seated. A self-tapping screw used without the right pilot hole may split material or overload the drive. A self-drilling screw used in the wrong metal thickness may drill poorly, overheat, or leave weak thread engagement.
Define the joint before the screw. State the materials being fastened, their thicknesses, and whether the screw goes into metal, timber, fiberboard, plastic, or a prepared insert. For metal-to-metal work, point geometry and thread form carry more weight. For wood-based panels, thread pitch, pull-out resistance, and head seating matter more.
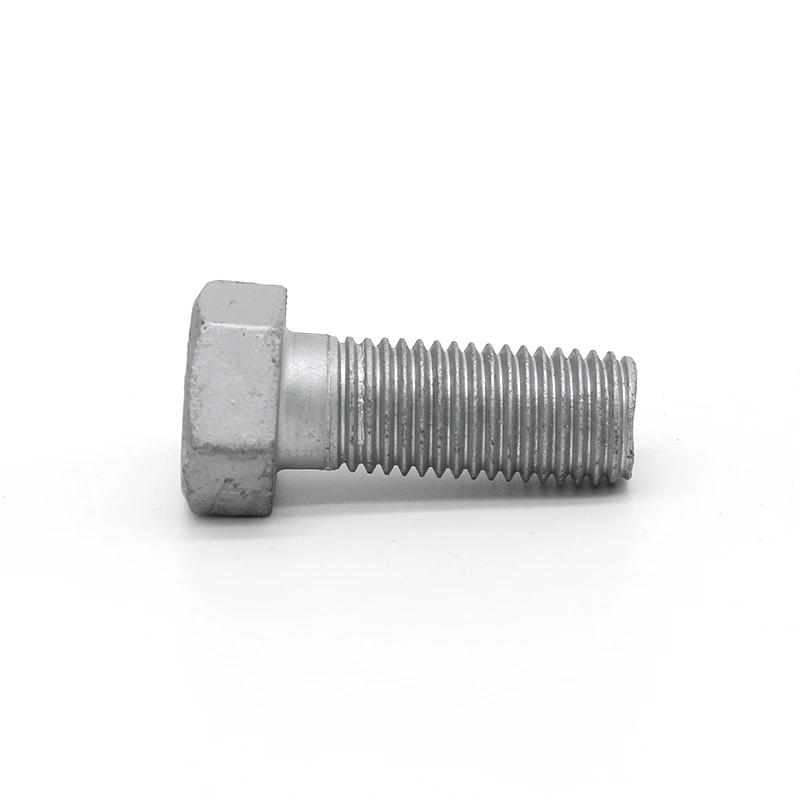
Match the head and drive to the assembly process. Countersunk heads sit flush in furniture and panel work, while hex heads are common where higher installation torque or washer use is expected. Cross recess, hex washer head, and other drive types affect tooling, cam-out risk, worker speed, and finish appearance.
Do not treat coating as decoration. Zinc, Dacromet-type coatings, and other finishes are selected for service environment, corrosion expectations, appearance, and compatibility with the materials being joined. Ask what coating options are available and what test or standard the order should reference if corrosion resistance is a purchase requirement.
Avoid vague RFQs. “Self tapping screw” or “roofing screw” is not enough for reliable quotation. Provide size, length, head type, drive type, material, coating, washer requirement if any, packing needs, drawings or standard references, order quantity, and the intended application. If the current screw is failing, describe the failure mode as well.