Internal Thread Cutting Tools | Hebei Wotu Fastener Manufacturing Co., Ltd.

Internal Thread Cutting Tools for Fastener Assemblies

An internal thread cutting tool is selected around the hole, material, thread standard, and production method. The main choice is not just size; it is whether the job needs a cutting tap, a forming tap, or a thread mill, and how that tool will create a clean, usable female thread without damaging the part.

For buyers working with fasteners or threaded assemblies, the thread quality must match the screw or bolt that will be installed later. A poor match can cause tight assembly, weak engagement, cross-threading, or rejected parts.

Related Products

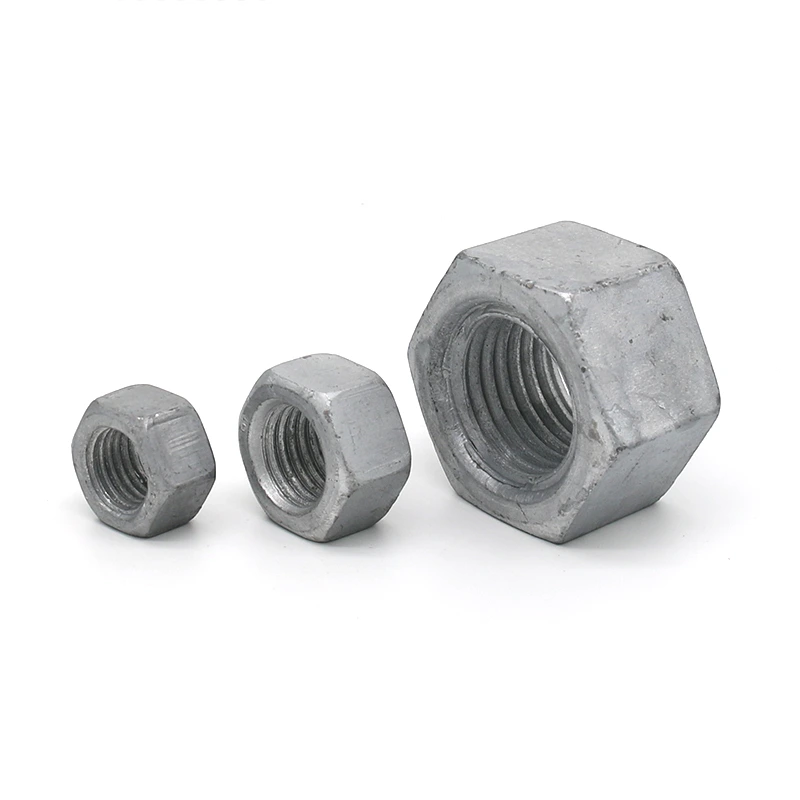
Hot-Dip Galvanized Hex Nut (DIN934 Thickened/GB Thin Nut In Multiple Specifications)

Hot-Dip Galvanized Hex Nut (DIN934 Thickened/GB Thin Nut In Multiple Specifications)

Brand: Wotu Surface: high temperature hot dip zinc plated surface treatment Specifications: Comply with DIN934, GB/T6170, GB/T6172.1 Chinese national standard German standard, in stock M6-M64 full range of specifications, length is nonstandard customized as required Packaging: 25kg woven bag/export carton, full-container wooden pallet wrapped with film, supports neutral packaging, private-label customization

Read More
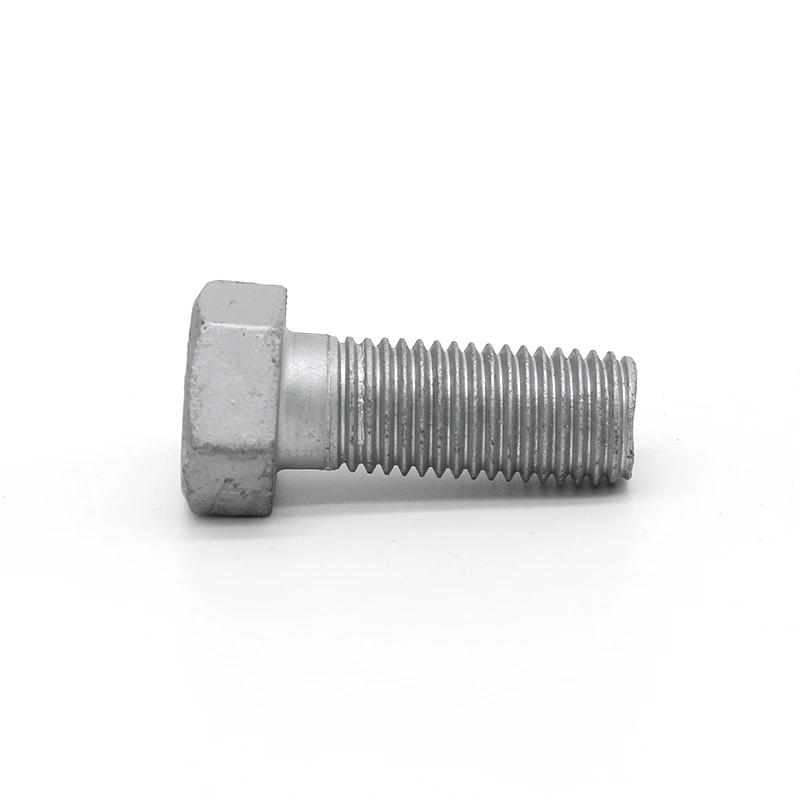
Hot-Dip Galvanized Hex Head Bolt (DIN931 Half Thread / DIN933 Full Thread / GB30 Chinese National Standard Bolt, Can Be Equipped With Nut And Washer Set)

Hot-Dip Galvanized Hex Head Bolt (DIN931 Half Thread / DIN933 Full Thread / GB30 Chinese National Standard Bolt, Can Be Equipped With Nut And Washer Set)

Brand: Wotu Surface: overall hot-dip zinc plating treatment Specifications: Comply with DIN and GB standards, in stock M6-M48 full range of specifications, length 20mm-300mm, supports nonstandard customized. Packaging: woven bag inside / 25kg export carton, film-wrapped wooden pallet; supports neutral packaging and customer private-label customization.

Read More
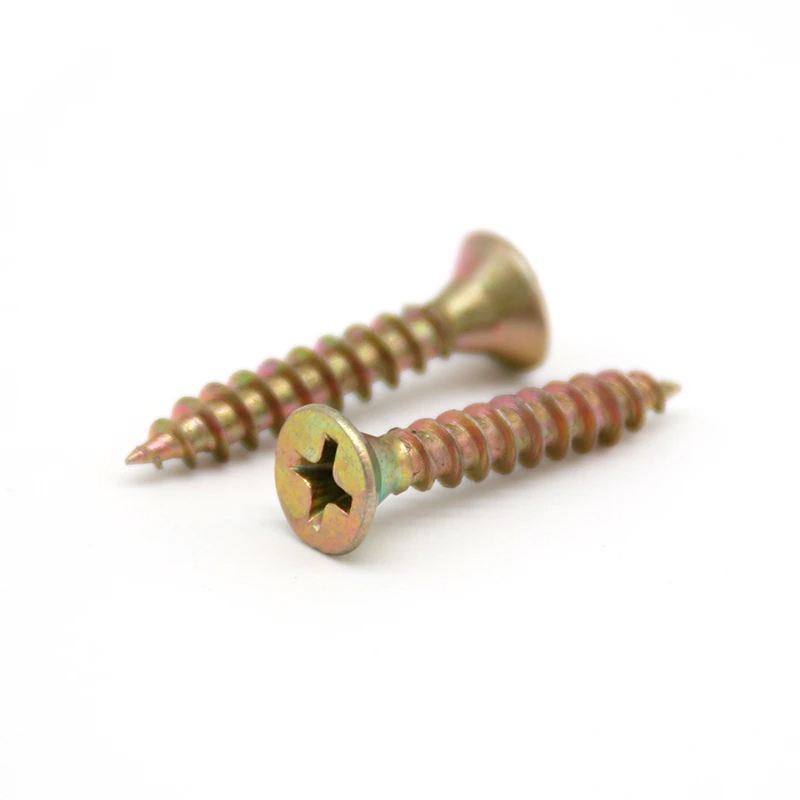
Countersunk Head Cross Thick Thread Fiberboard Screw

Countersunk Head Cross Thick Thread Fiberboard Screw

Brand: Wotu Surface: color zinc plated electroplating Specifications: in stock 3.5/4.0/4.5/5.0 regular wire diameter, rod length 16~80mm full range of specifications in stock, supports nonstandard length customization Packaging: 25kg cartons, whole wooden pallets

Read More
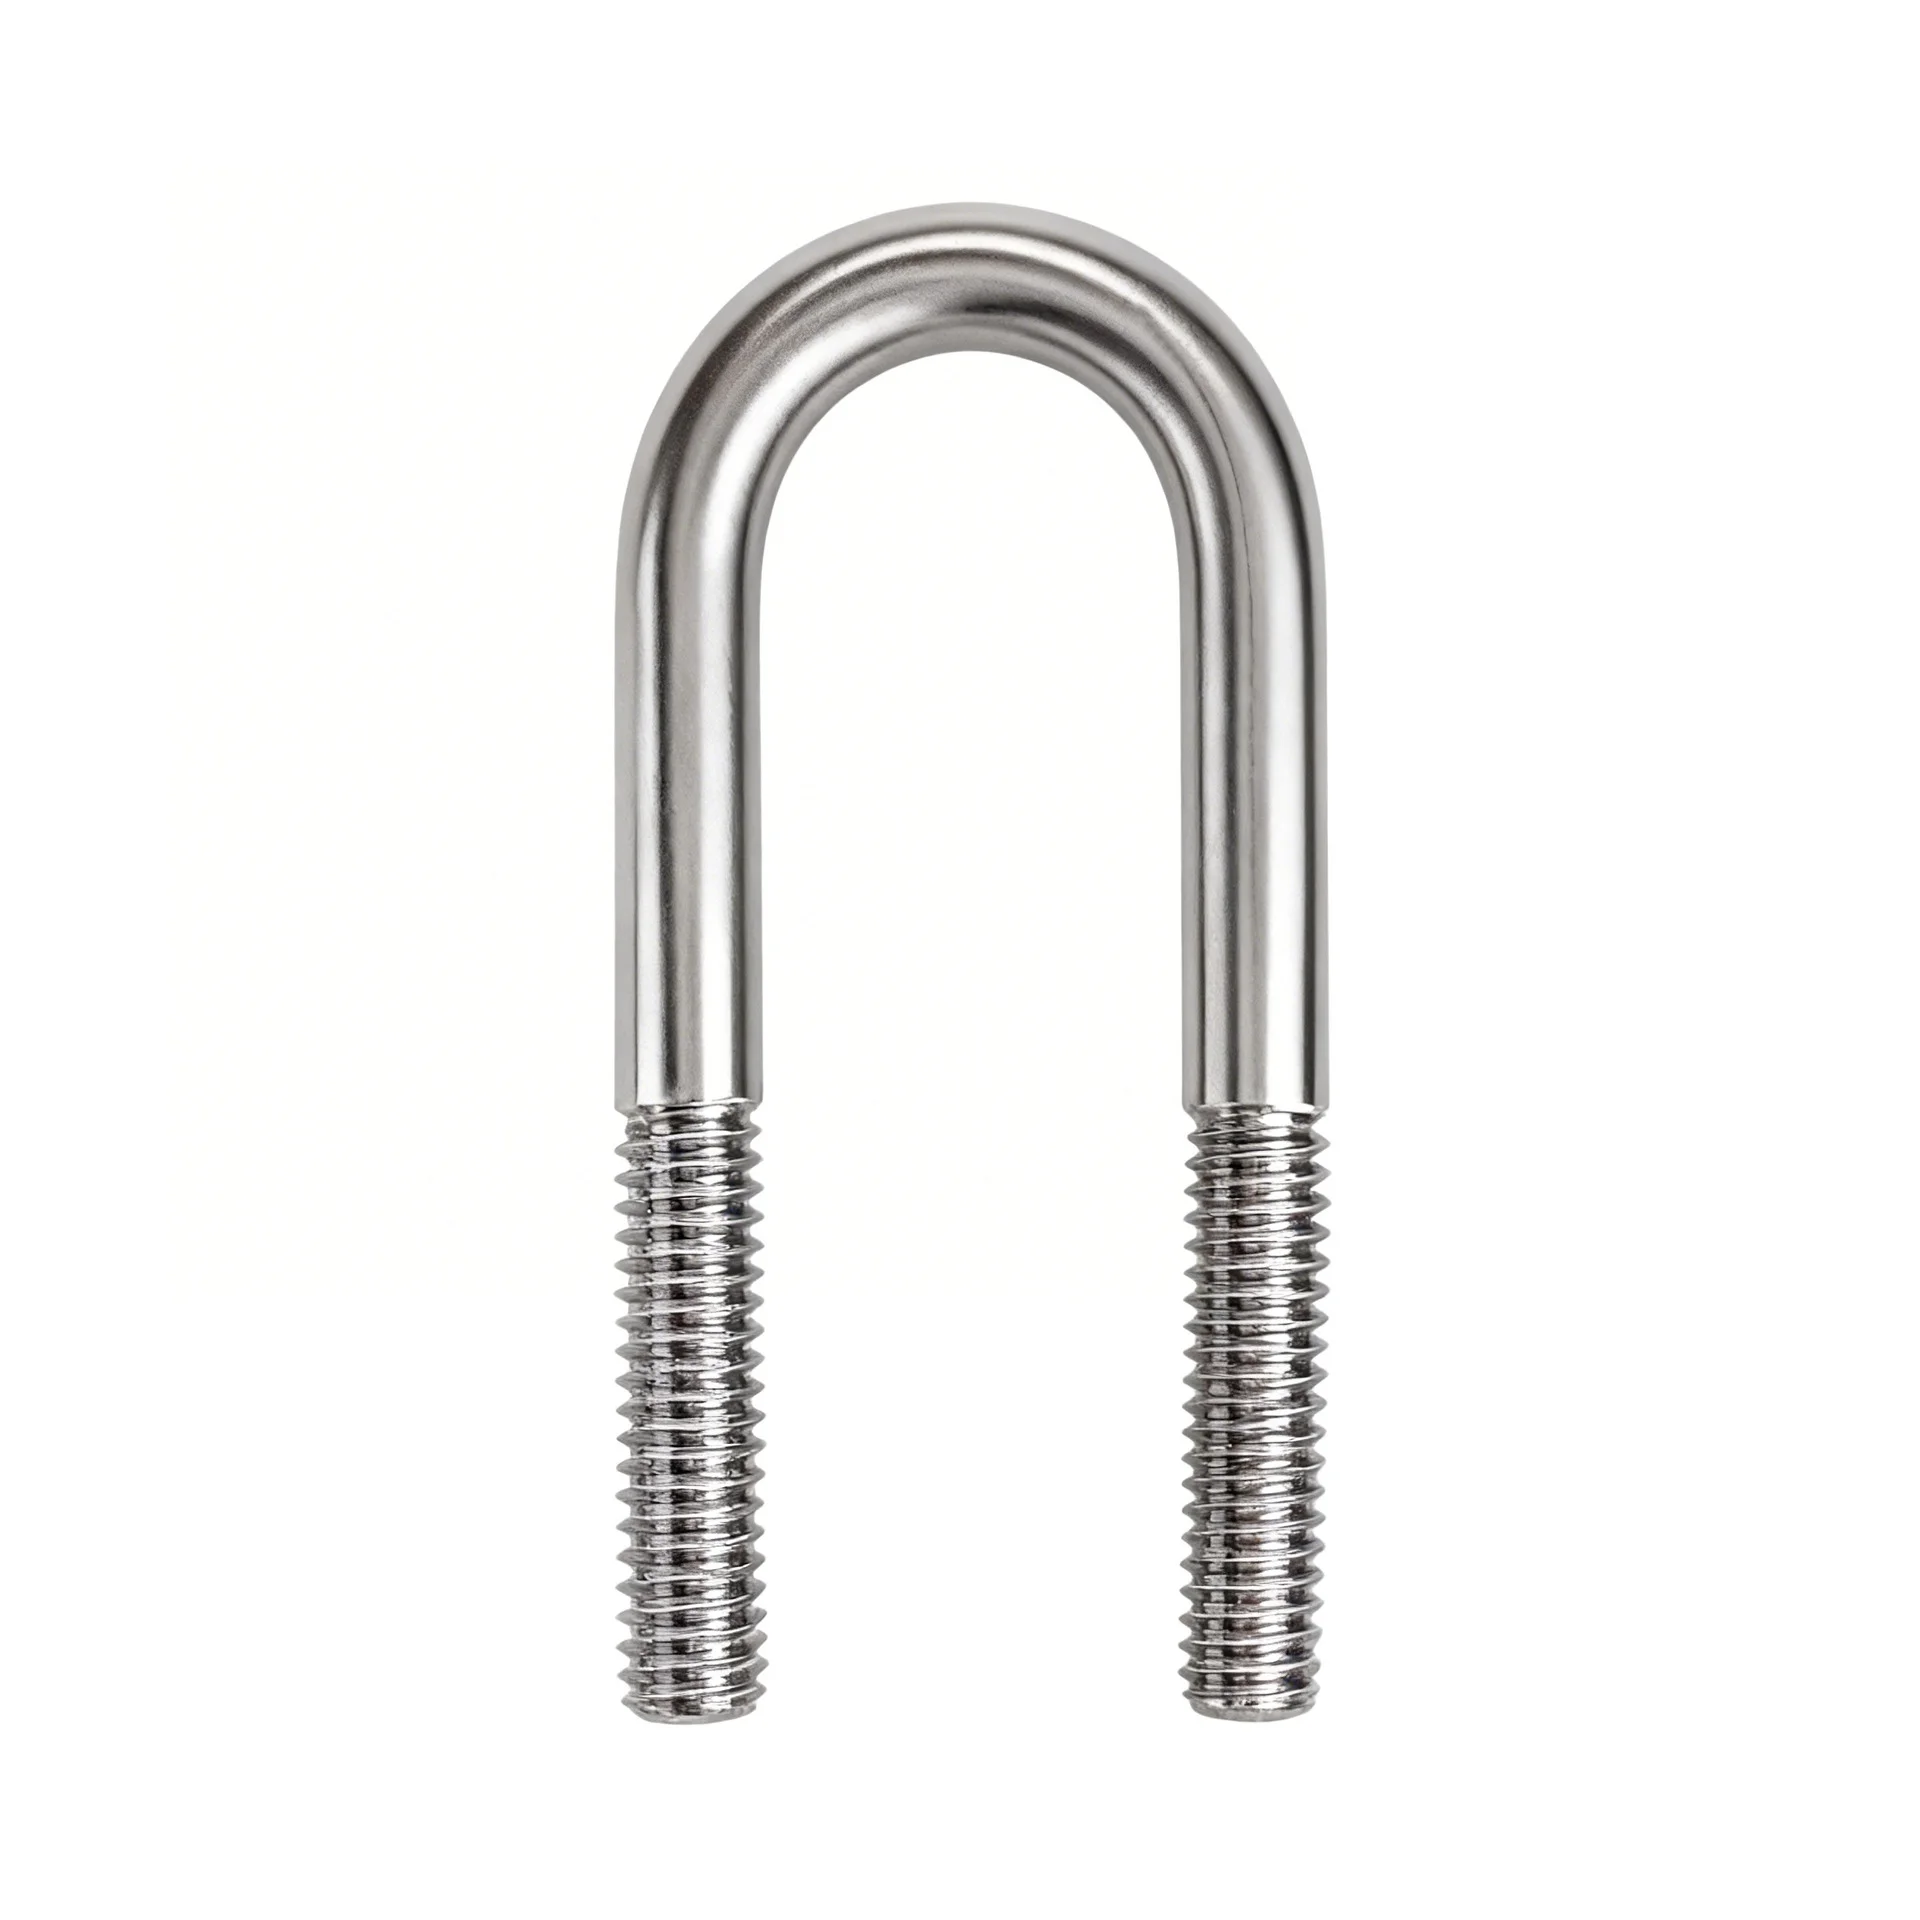
U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

Brand: Wotu Surface: natural black oxide / hot-dip galvanized / blue-white zinc plated, multiple processes available Specifications: Based on common industry drawing parameters, suitable for pipe diameter 25mm~139.7mm, screw diameter M10~M24, total length can be nonstandard customized Matching: can be matched with nut, flat washer and spring washer of the same specifications for complete shipment Packaging: Bundling and packaging + 25kg export carton, full-container wooden pallet wrapped with film, supports private-label export packaging

Read More
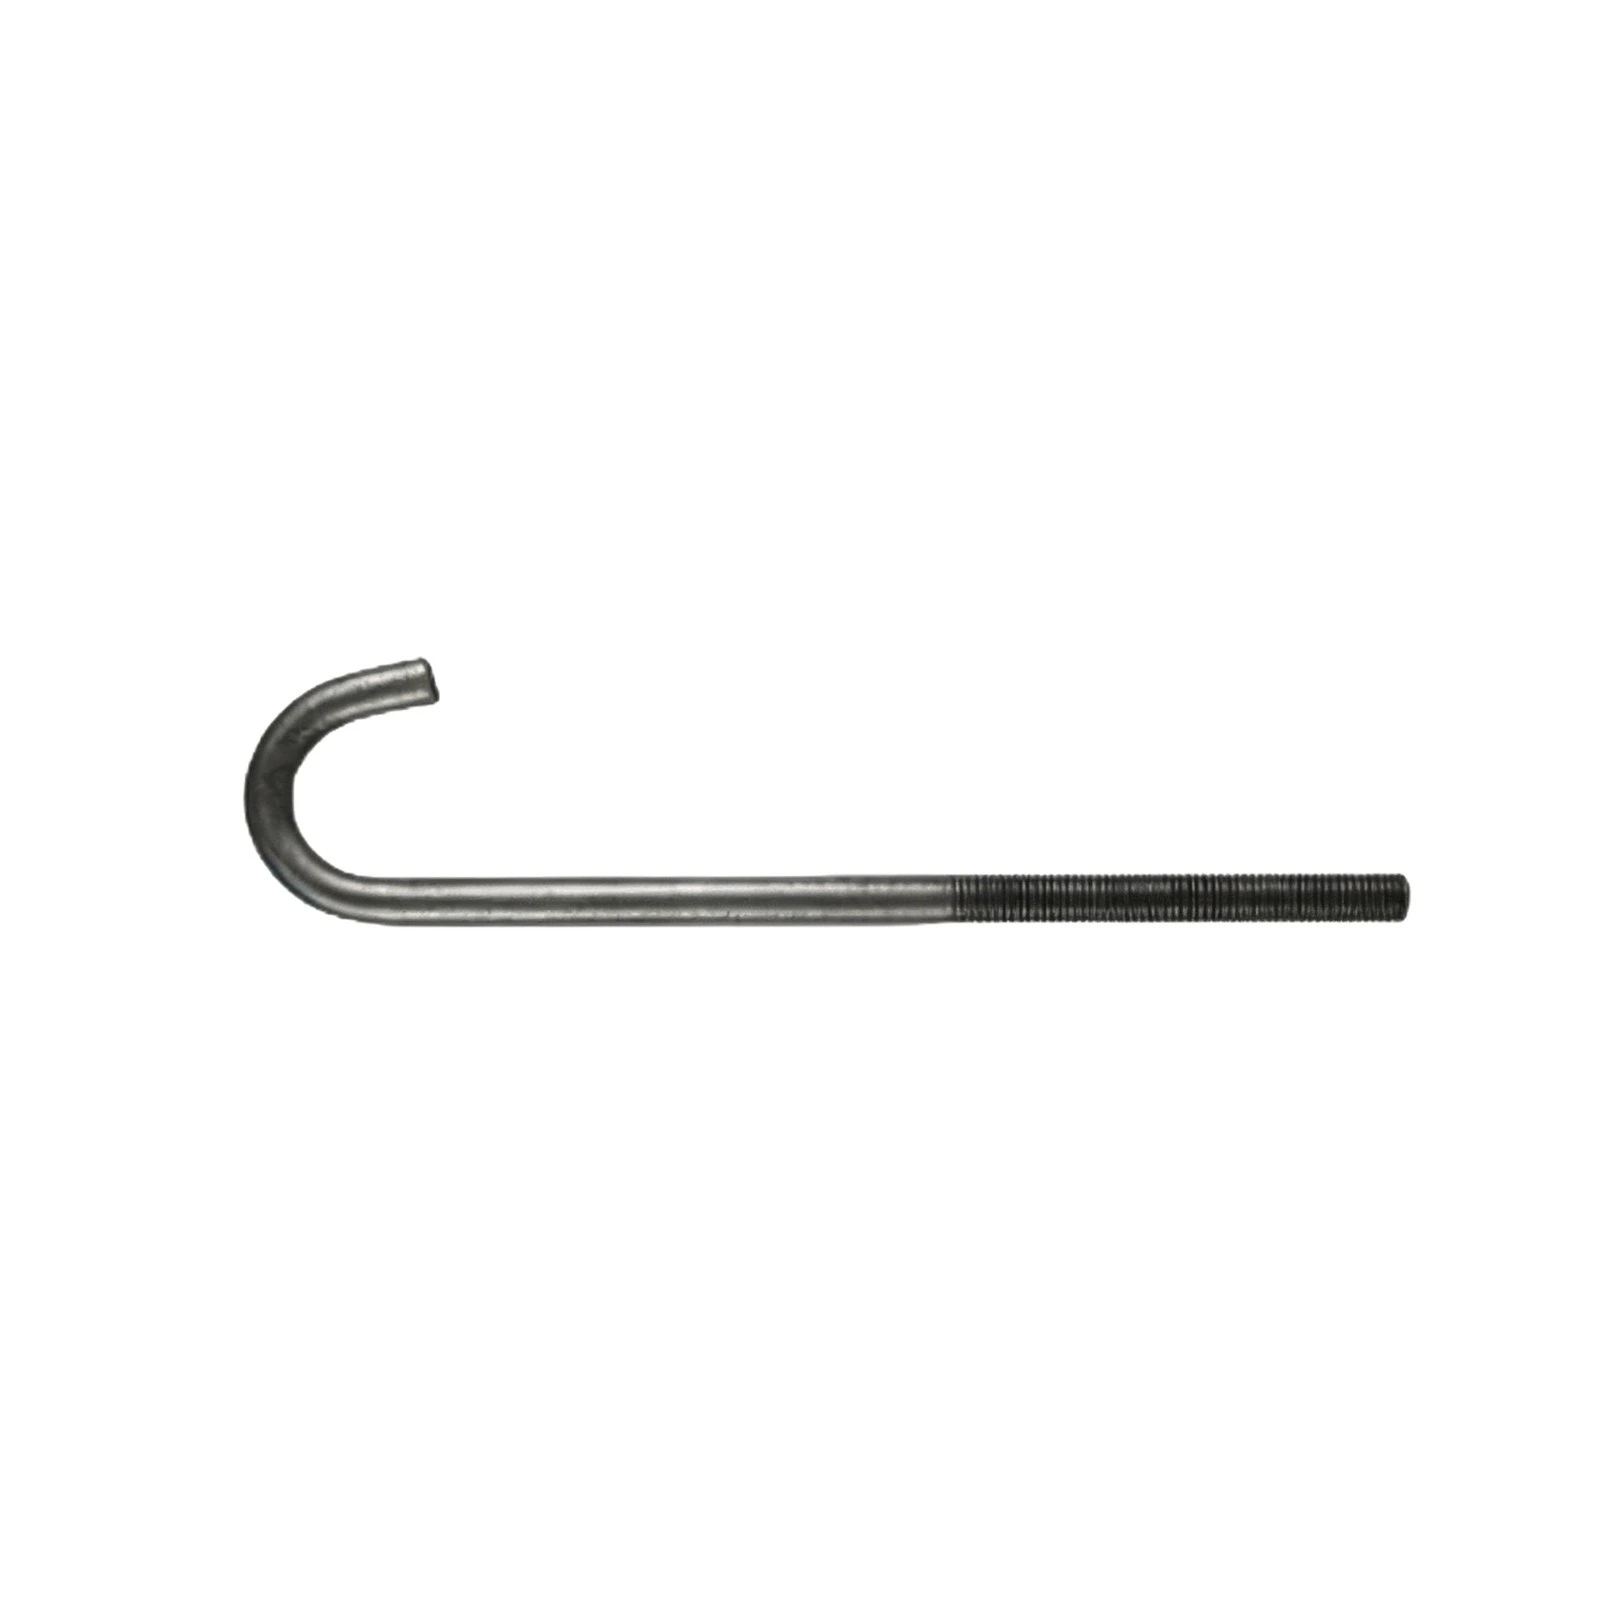
7-letter, 9-letter L-shaped anchor bolt (Chinese national standard GB/T799-1988 embedded anchor screw)

7-letter, 9-letter L-shaped anchor bolt (Chinese national standard GB/T799-1988 embedded anchor screw)

Brand: Wotu Surface: Natural black oxide treatment, customized hot-dip galvanized, zinc plated as required Specifications: Follow Chinese national standard GB/T799-1988, in stock M12-M48, total length 120mm~1500mm, nonstandard customized diameter, bending length, total screw length available Matching: Nuts, flat washers and spring washers of the same specification can be supplied in complete sets. Packaging: Bundling and packaging, using wooden pallets and film-wrapped export packaging in large quantities

Read More
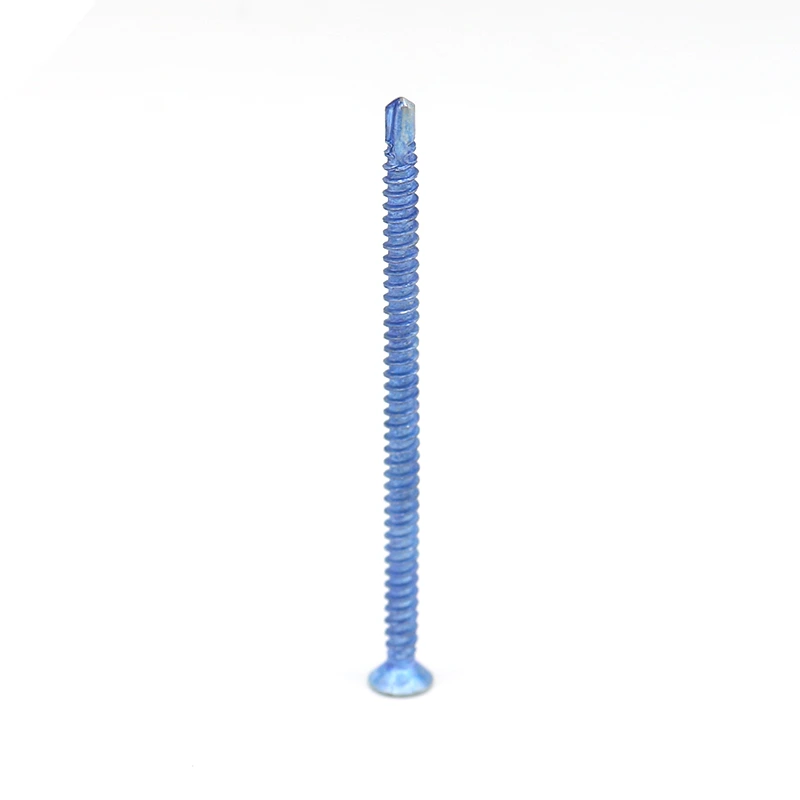
Countersunk Head Blue Zinc Self-Drilling Screw

Countersunk Head Blue Zinc Self-Drilling Screw

Brand: Hengzuan Surface: blue and white zinc plated, can be customized color zinc plated, black oxide plated Specifications: in stock 3.5/3.9/4.2/4.8/5.5 mainstream wire diameter, rod length 13mm~75mm full size range, nonstandard length can be customized as needed Packaging: 25kg export cartons, full wooden pallets wrapped with film, supports neutral export packaging, private-label customization

Read More

Selecting a Tool for Clean Internal Threads

Internal Thread Tool Criteria

Compare internal thread cutting tools by thread standard, tap or thread-mill type, flute geometry, workpiece material suitability, hole depth, chip control, coating, and the required tolerance of the finished thread. The best selection is the one that produces a reliable internal thread for the fastener and assembly method, not simply the lowest-cost tool of the same nominal size.

Criterion What To Check Why It Matters Buyer Tip
Thread standard, nominal size and pitch Match the tool to the required thread form, diameter, pitch and tolerance class. A mismatch can produce an unusable internal thread or poor fit with the mating fastener. Ask: Which thread standard, size, pitch and finished tolerance should the tool produce?
Tool type and cutting operation Confirm whether the job needs a hand tap, machine tap, forming tap, or a single-point internal threading tool. The correct tool depends on the machine, hole geometry, production volume and whether chips must be evacuated. Ask: Is the tool intended for manual tapping, CNC machining, blind holes, or through holes?
Workpiece material and hardness Review the material grade, hardness range and any coating, plating or heat treatment on the workpiece. Material behavior affects cutting load, edge wear, chip control and the risk of thread damage. Ask: Which workpiece materials and hardness range has this tool been designed to cut?
Blind-hole depth and chip management Compare the cutting length, usable thread depth and flute or chip-clearance design with the hole geometry. A blind hole needs enough chip space and clearance to avoid packing, breakage or an incomplete thread at the bottom. Ask: What minimum hole depth and bottom clearance does the tool require for this thread?
Machine interface and operating guidance Verify the shank or holder interface, spindle use, alignment requirements and recommended cutting conditions. Poor fit or incorrect operation can cause runout, oversize threads, premature wear or tool failure. Ask: Which holder, alignment method and cutting parameters should be used on our machine?

Key Decisions Before Cutting or Forming an Internal Thread

The most useful distinction is between cutting and forming the internal thread. A cutting tap removes material and creates chips, so chip evacuation and hole depth matter. A forming tap displaces material instead of cutting it, which can produce strong threads in suitable ductile materials but usually needs a different drill size and enough wall thickness around the hole.

Thread milling is another option when flexibility matters, especially for larger diameters, CNC work, or jobs where one tool may cover several thread sizes. It can reduce breakage risk in difficult parts, but it requires the right machine, program, and toolholding setup. The right choice depends on the workpiece material, blind or through-hole design, thread tolerance, batch size, and the fastener that will be assembled into the thread.

Start with the thread that the finished part must accept. Confirm the standard, nominal diameter, pitch, right- or left-hand direction, and required fit. If the internal thread will receive a screw, bolt, or stud already specified in the assembly, the tool choice should support that mating part rather than only matching a drawing note.

Match the tool style to the hole. Spiral point taps are often used for through holes because they push chips ahead. Spiral flute taps help pull chips back from blind holes. Straight flute taps can suit simpler materials and short runs. For forming taps, confirm that the material can be cold-formed and that the prepared hole size is correct for thread formation, not for a conventional cutting tap.

Do not treat pilot hole size as a minor detail. A hole that is too small can overload the tool or distort the thread; a hole that is too large can reduce thread engagement. Surface finish, coating, lubrication, and machine rigidity also change the result, especially in stainless steel, alloy steel, cast materials, or abrasive materials.

A practical next step is to provide the internal thread specification, workpiece material, hole type, production method, and the mating fastener details. If Hebei Wotu Fastener Manufacturing Co., Ltd. is being asked to support a threaded assembly, also confirm whether the requirement is for the thread cutting tool itself, the mating fastener, or advice on matching the two.

Criteria Importance Description Example Options
Thread creation method Primary decision Cutting taps remove material, forming taps displace material, and thread mills machine the profile using CNC motion. Each method changes hole preparation, chip behavior, and production setup. A ductile metal part may allow thread forming, while a brittle cast material may require a cutting method instead.
Hole type and depth High impact on tool style Blind holes, through holes, and deep holes need different chip-control strategies and clearance allowances. The full thread depth should be defined separately from drilled depth. A blind hole may need a spiral flute tap or a programmed thread mill path to avoid packing chips at the bottom.
Workpiece material Controls wear, chip formation, and feasibility Soft, ductile, hard, abrasive, and brittle materials behave differently during internal threading. Material choice affects tool geometry, coating, lubrication, and whether forming is suitable. Aluminum, stainless steel, alloy steel, and cast iron may call for different tap styles even when the nominal thread size is the same.
Mating fastener fit Critical for assembly reliability The internal thread must match the screw, bolt, or stud that will be installed. Thread standard, pitch, hand direction, and fit expectations should be checked before production. A metric bolt and an inch-series internal thread can look similar in size but will not assemble correctly.
Production method Affects cost and consistency Hand tapping, drill press work, tapping heads, and CNC machining place different demands on tool strength, alignment, speed control, and repeatability. A CNC batch job may justify thread milling or optimized machine taps, while a small repair job may use a conventional hand tap set.

Product Selection

Related Options

For furniture hardware, machinery housings, metal brackets, or other parts that receive threaded fasteners, the priority is consistent engagement between the internal thread and the screw or bolt. A buyer should choose the tool style and hole preparation method around the material and assembly load so the thread holds properly during installation and service.

Blog Articles / Reviews

How to Specify Countersunk Head Cross Thick Thread Fiberboard Screws for Furniture Assembly Projects

How to Specify Countersunk Head Cross Thick Thread Fiberboard Screws for Furniture Assembly Projects

Fiberboard screws are selected based on more than screw size alone. For furniture assembly and board-based applications, buyers need to match the screw structure with the characteristics of fiberboard, MDF, and similar engineered wood materials. A suitable specification should consider thread design, head style, screw length, diameter, installation method, and application requirements. For buyers sourcing […]

Frequently Asked Questions

Should I use a cutting tap, forming tap, or thread mill?

Use a cutting tap when the material can be machined cleanly and chip control is manageable. Consider a forming tap for ductile materials where chip-free threading and strong formed threads are useful, but confirm the correct pre-hole size. Thread milling can suit CNC work, larger diameters, or jobs needing more flexibility, but it depends on machine capability and programming.

What changes between blind-hole and through-hole threading?

A through hole gives chips a place to exit, so a spiral point tap is often practical. A blind hole traps chips at the bottom, so chip evacuation, usable thread depth, and bottom clearance become more important. The drawing should separate total hole depth from full thread depth.

Is the drill size the same for every internal thread tool?

No. Cutting taps and forming taps often need different prepared hole sizes because one removes material and the other displaces it. Using the wrong drill size can cause tool overload, poor thread engagement, or a thread that does not fit the mating fastener correctly.

How much does the mating screw or bolt matter?

It matters a lot because the internal thread is only useful if it works with the fastener that will be installed. Confirm the thread standard, diameter, pitch, tolerance or fit expectation, and material combination before selecting the tool. This is especially important where assembly torque, vibration, or repeated installation is expected.

What information should I send before asking for advice?

Provide the thread size and pitch, workpiece material, blind or through-hole design, hole depth, production method, and expected batch size. If the request relates to a fastened assembly, also include the screw or bolt that must fit the internal thread. For Hebei Wotu Fastener Manufacturing Co., Ltd., clarify whether you need the tool itself, a matching fastener, or support checking thread compatibility.

Leave Your Message

Send the thread size and pitch, workpiece material, and whether the hole is blind or through. If the internal thread must match a specific screw or bolt, include that fastener detail as well.