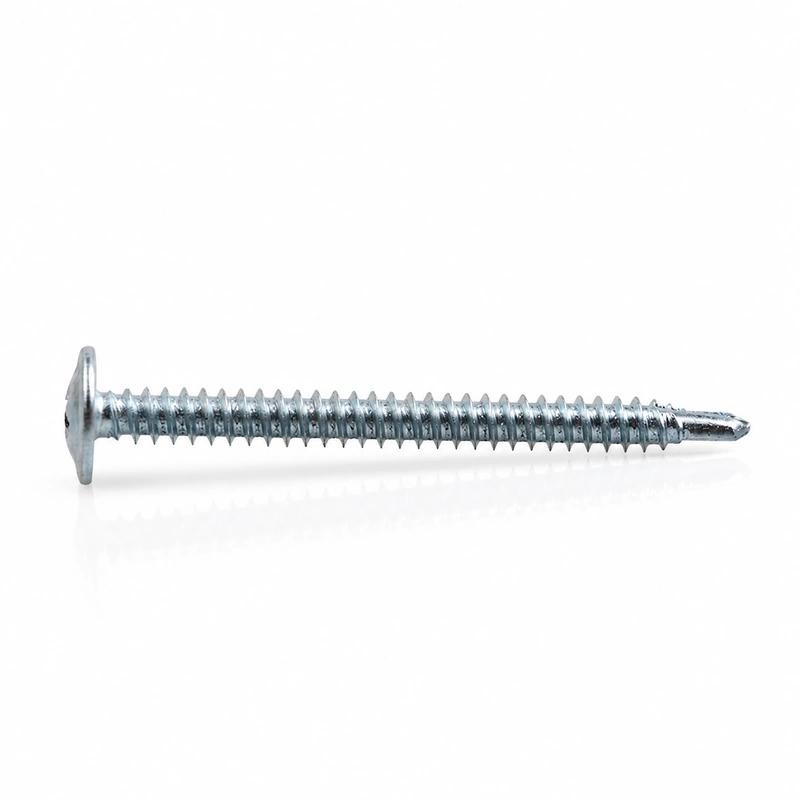
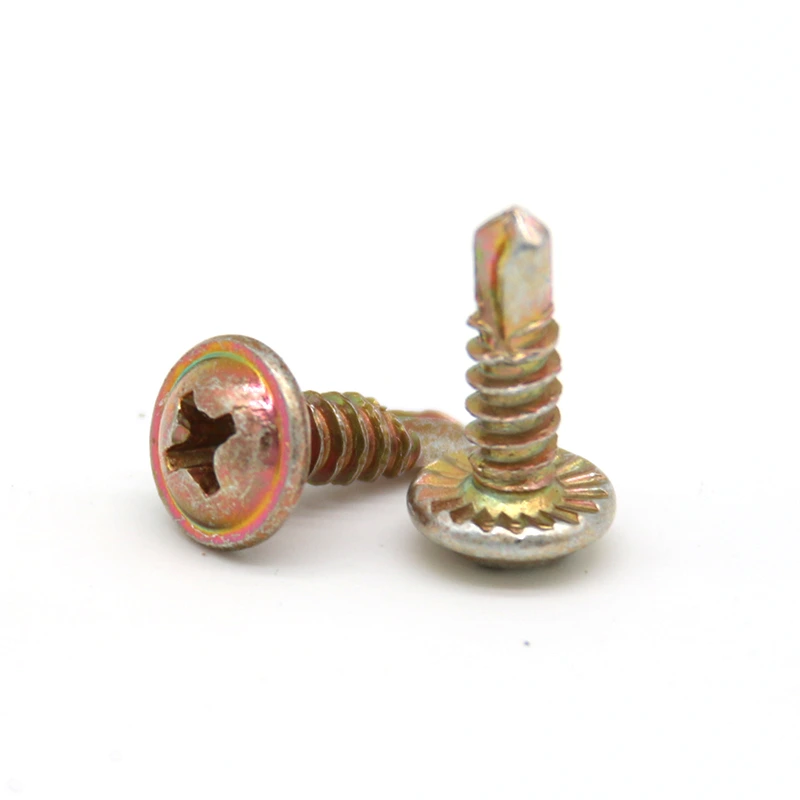
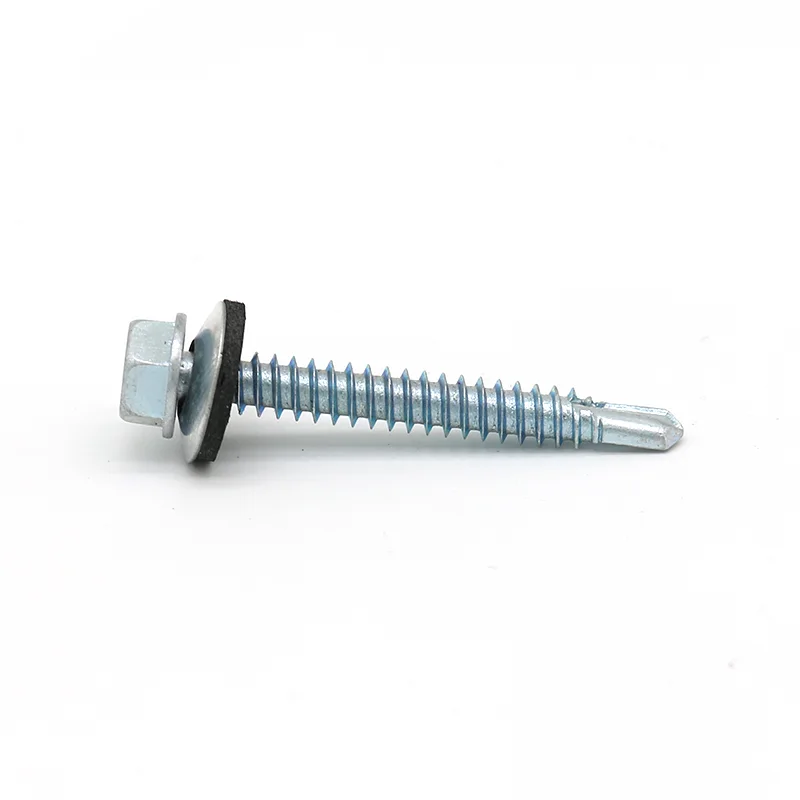
| Head angle and countersink fit |
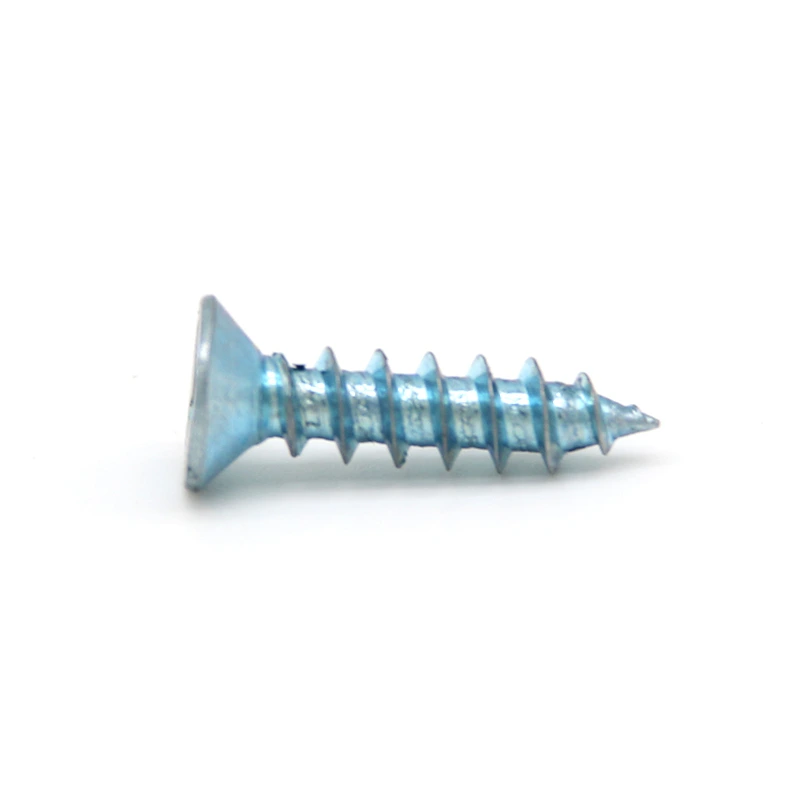
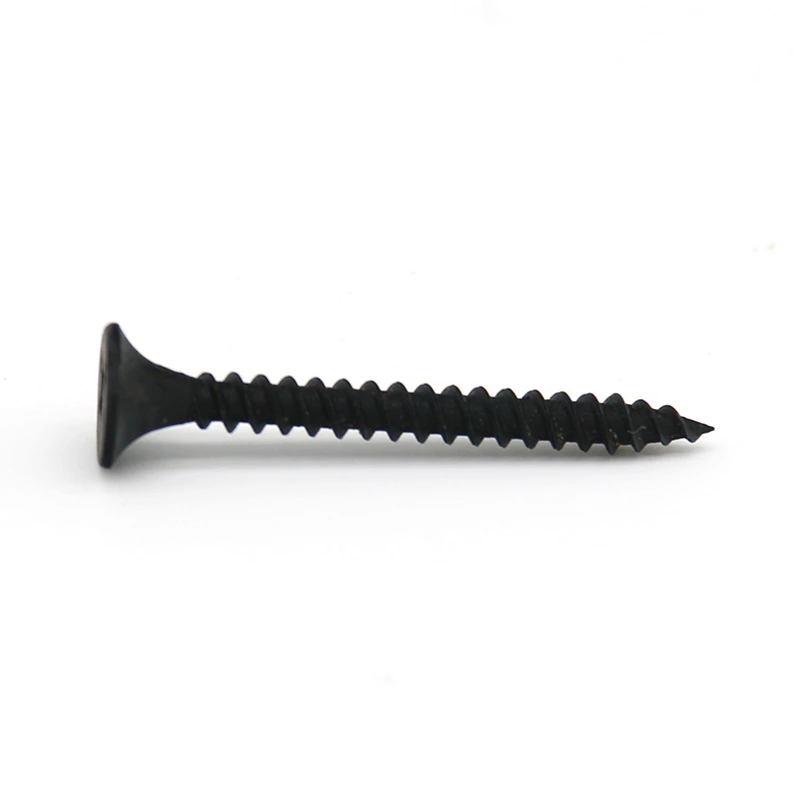
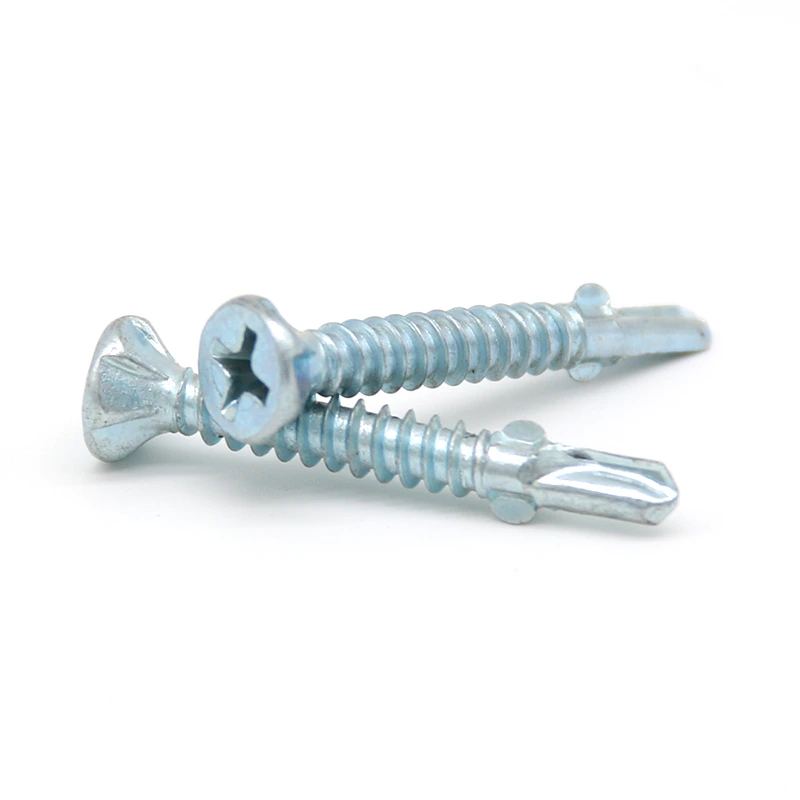
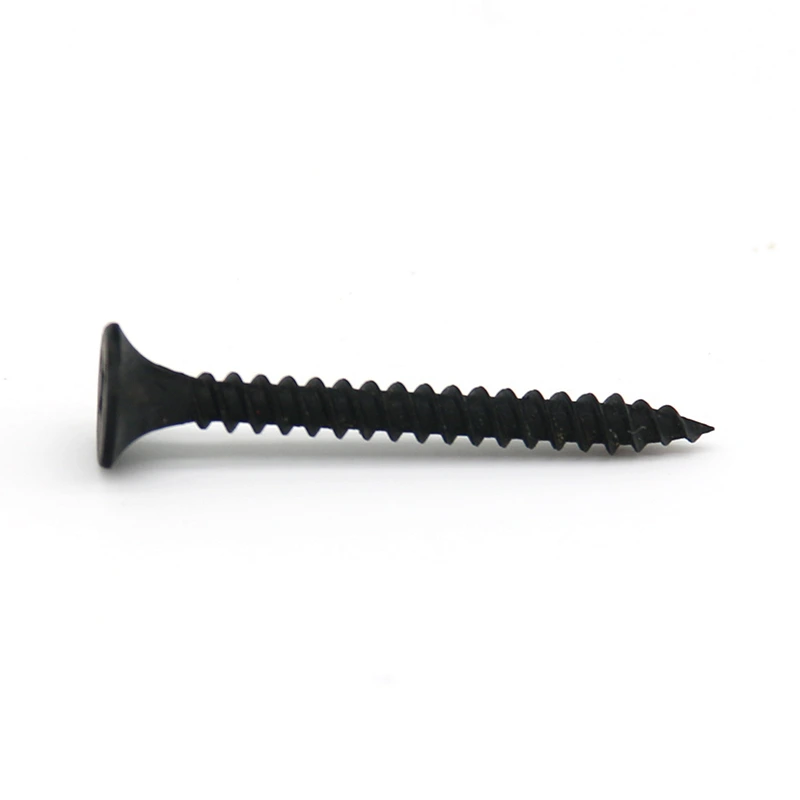
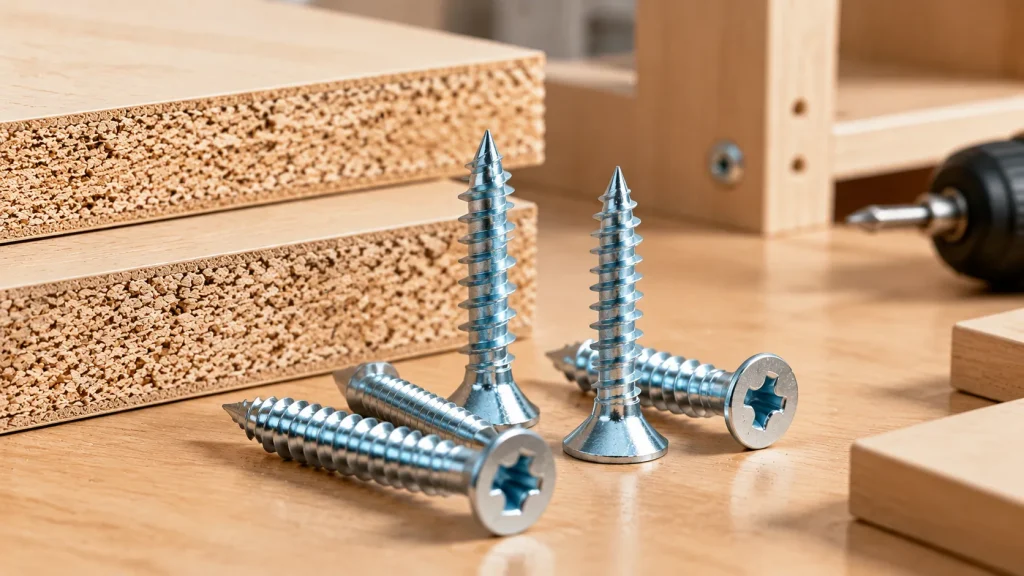
Match the flat head angle and head diameter to the countersink in the mating part or drawing. |
A flat head tapping screw should sit flush without rocking, bottoming out too early, or leaving the head proud of the surface. |
Can you confirm the required head angle, head diameter, and whether the screw must finish flush after tightening? |
| Thread type for the base material |
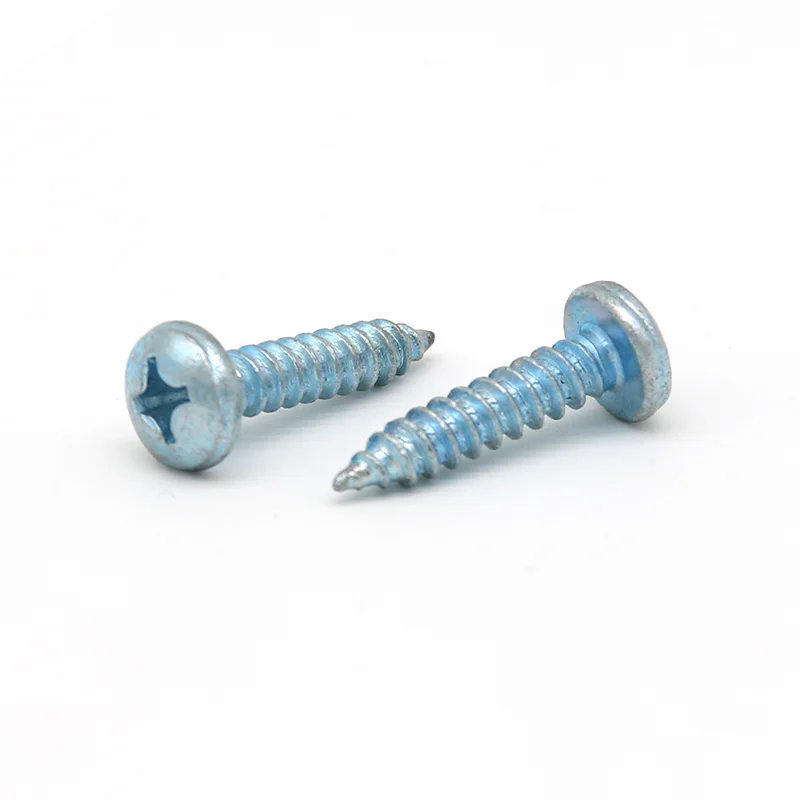
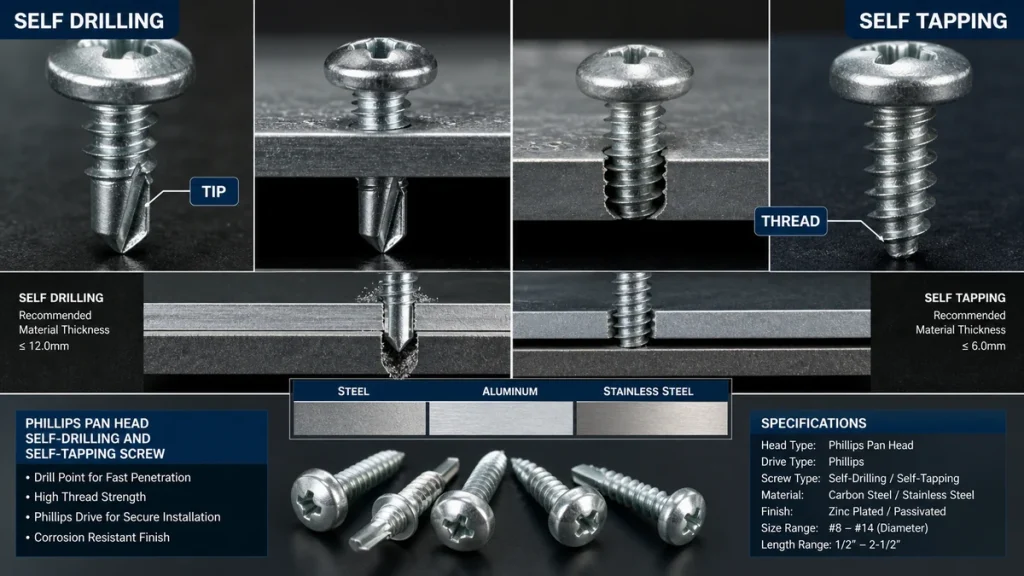
Identify whether the screw will tap into sheet metal, plastic, wood-based material, or a pre-formed pilot hole. |
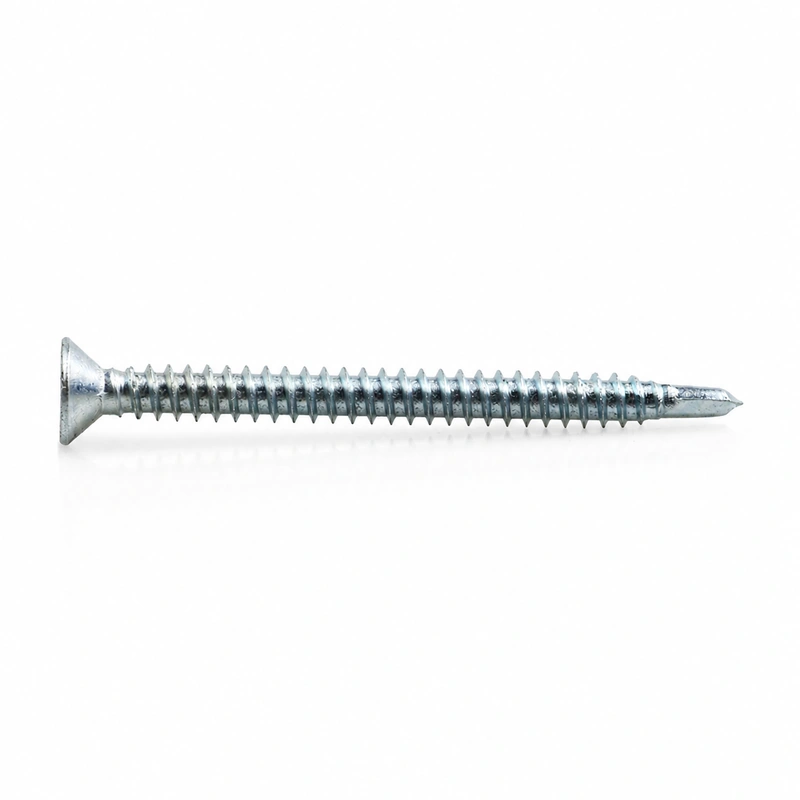
Thread pitch, depth, and point style affect how cleanly the screw forms or cuts its mating thread and how well it resists loosening or pull-out. |
What material and thickness will the screw enter, and is the hole already drilled or punched? |
| Pilot hole and engagement length |
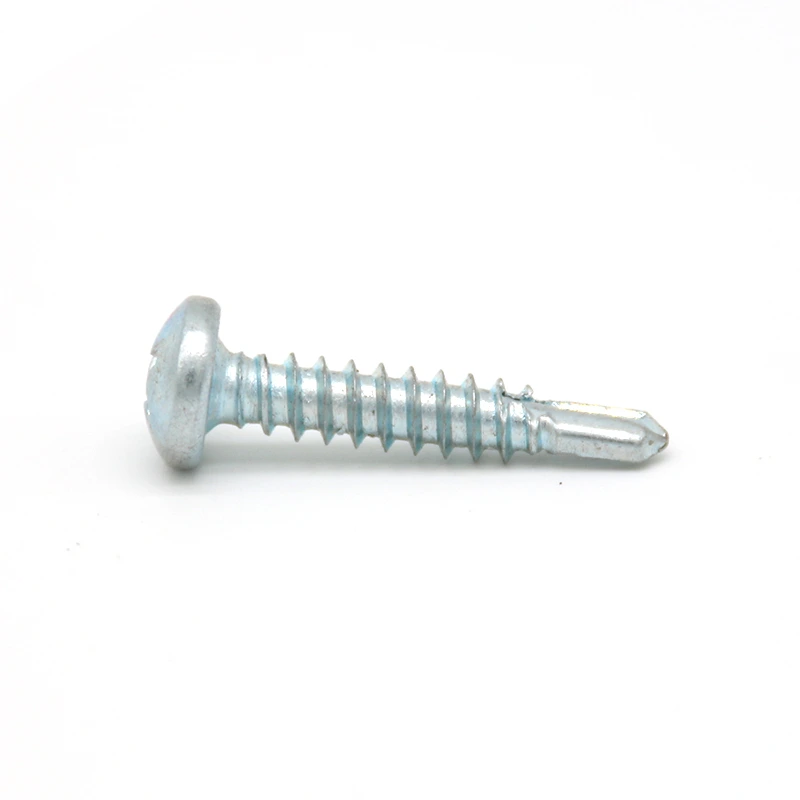
Compare the planned pilot hole size and the available thread engagement with the screw diameter and length. |
A hole that is too small can split or distort the part; a hole that is too large can reduce holding strength. Too little engagement may strip during assembly. |
Can you share the pilot hole diameter, material thickness, and required screw length under the head? |
| Drive recess and assembly tool |
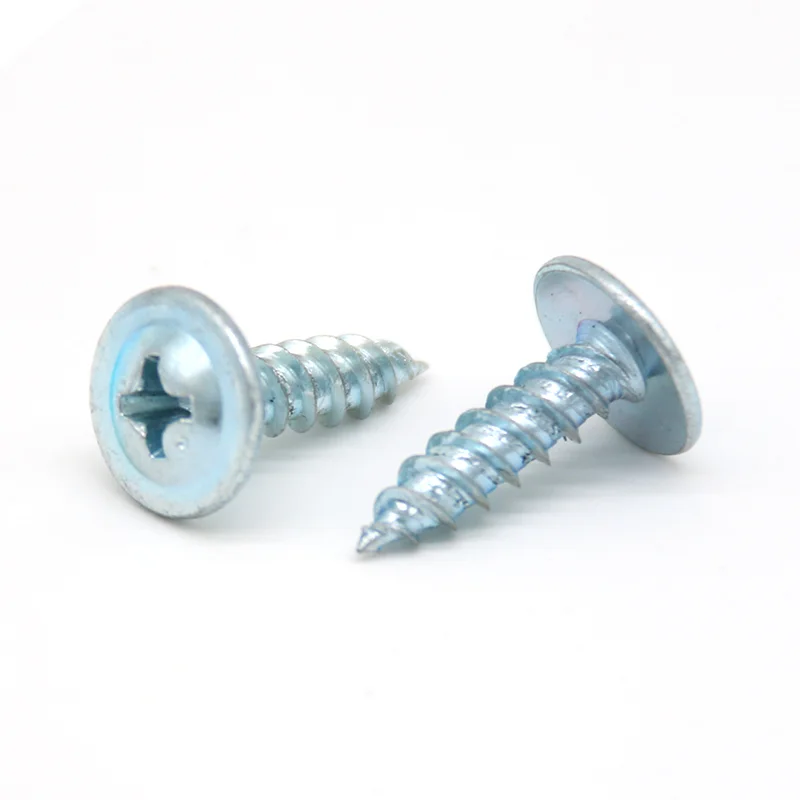
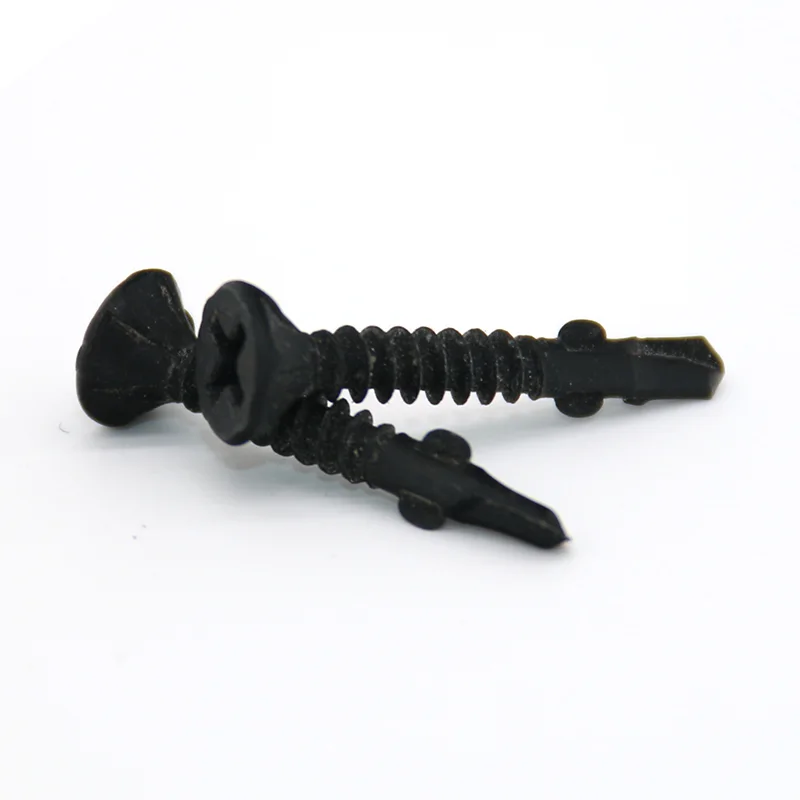
Choose a drive style that matches the production tool, torque control, and access angle, such as cross recess or another specified drive. |
The wrong recess can cam out, damage the finish, slow assembly, or make field removal difficult. |
Which driver bit and installation method will be used: hand tool, electric driver, or automated assembly? |
| Surface finish and operating environment |
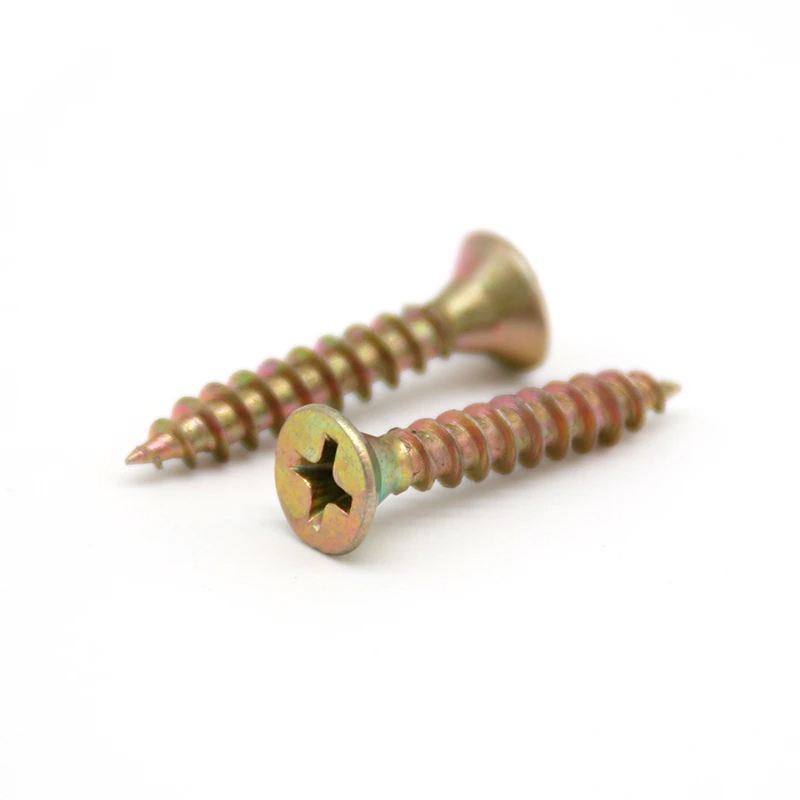
Specify the coating or material based on indoor use, outdoor exposure, contact with treated wood, chemicals, or dissimilar metals. |
Finish choice affects corrosion resistance, appearance, friction during driving, and compatibility with the assembled parts. |
Will the screw be used indoors, outdoors, in a humid area, or against a material that may cause corrosion? |