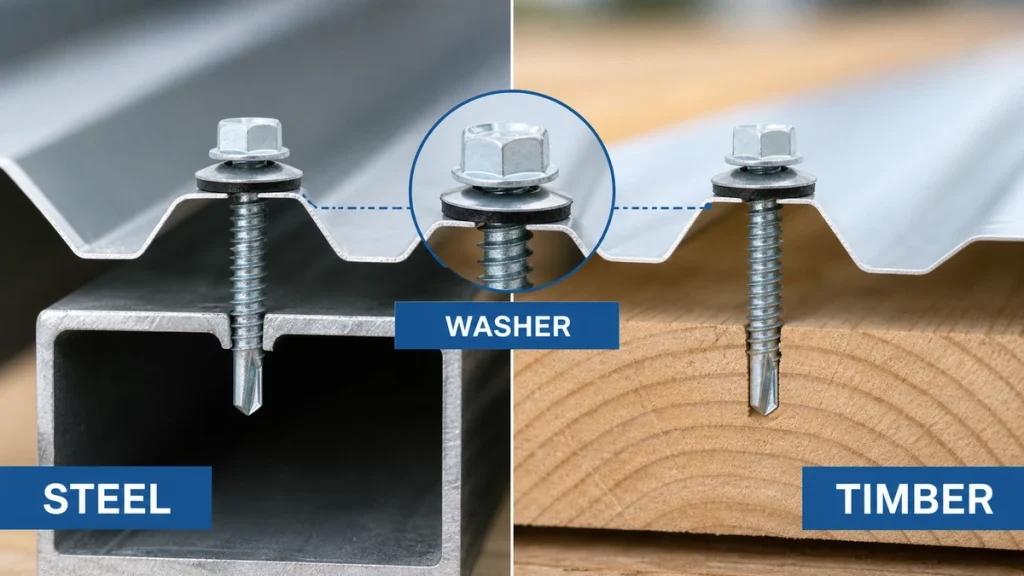
| Insert style for the parent metal |
Confirm whether the application needs a press-in, rivet nut, helical wire, key-locking, or solid threaded insert. |
Each style transfers load differently and suits different sheet thicknesses, hole conditions, repair work, or repeated assembly. |
Ask: is the insert for new production, thread repair, thin sheet metal, or a machined housing? |
| Internal thread and mating fastener |
Match the internal thread form, diameter, pitch, and thread depth to the bolt or screw used in the assembly. |
A mismatch can cause cross-threading, poor clamp load, or limited thread engagement before the joint is fully tightened. |
Send the mating fastener size and note whether the joint will be assembled and removed often. |
| Base metal thickness and hole preparation |
Verify the required drilled, tapped, reamed, or punched hole size and the minimum wall or sheet thickness around the insert. |
Threaded inserts for metal depend on correct hole geometry; an oversized or thin section can reduce pull-out and spin resistance. |
Ask what hole tolerance and preparation method the insert requires before releasing drawings or tooling. |
| Installation method and access |
Check whether installation needs a hand tool, pneumatic tool, press, staking operation, tang removal, or special locking keys. |
The installation process affects production speed, fixture design, inspection steps, and suitability for field repair. |
Ask if the insert can be installed from one side only, especially for tubes, enclosures, and closed sections. |
| Material, coating, and operating environment |
Compare the insert material and surface finish with the parent metal, exposure conditions, and any lubrication or corrosion concerns. |
Galvanic corrosion, heat, vibration, and wear can shorten joint life if the insert material is poorly matched to the assembly. |
Ask which insert material and finish are recommended for the exact metal, environment, and service temperature. |