Repeat Machine Selection | Hebei Wotu Fastener Manufacturing Co., Ltd.

Repeat machine selection for consistent production cycles

A repeat machine is selected for a production task that must run through the same sequence consistently, such as feeding, forming, fastening, pressing or assembling a workpiece. The key decision is not simply whether the machine can repeat a cycle, but whether it can repeat the required operation accurately with your material, tooling and production volume.

Start by defining the workpiece, the operation to be repeated and the result that must remain consistent. That information determines the machine layout, tooling, control method, feeding arrangement and level of operator involvement.

Related Products

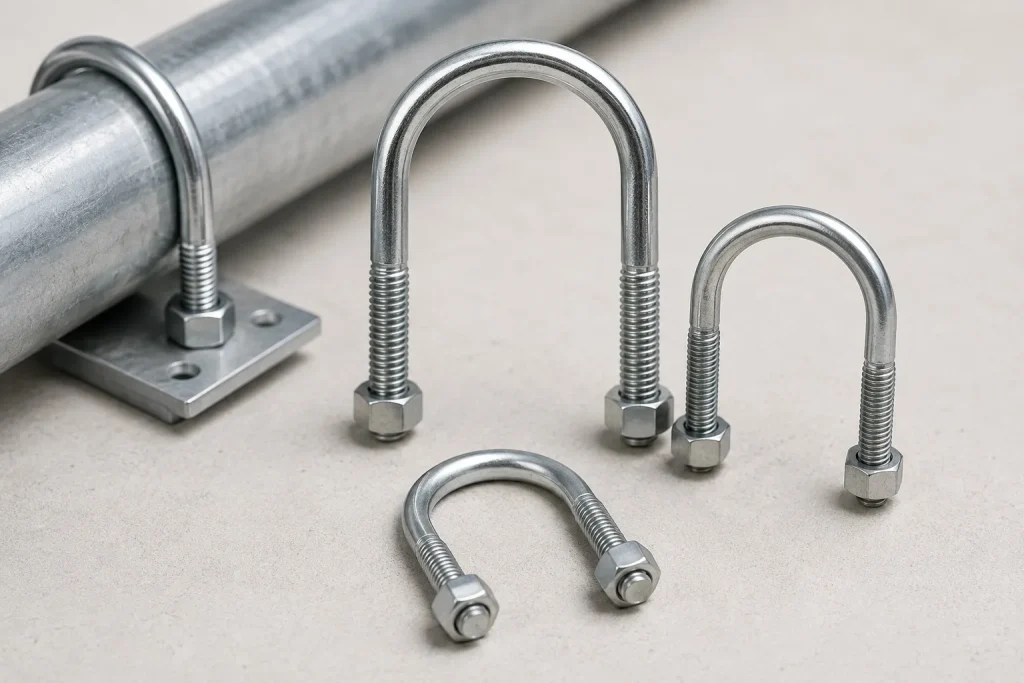
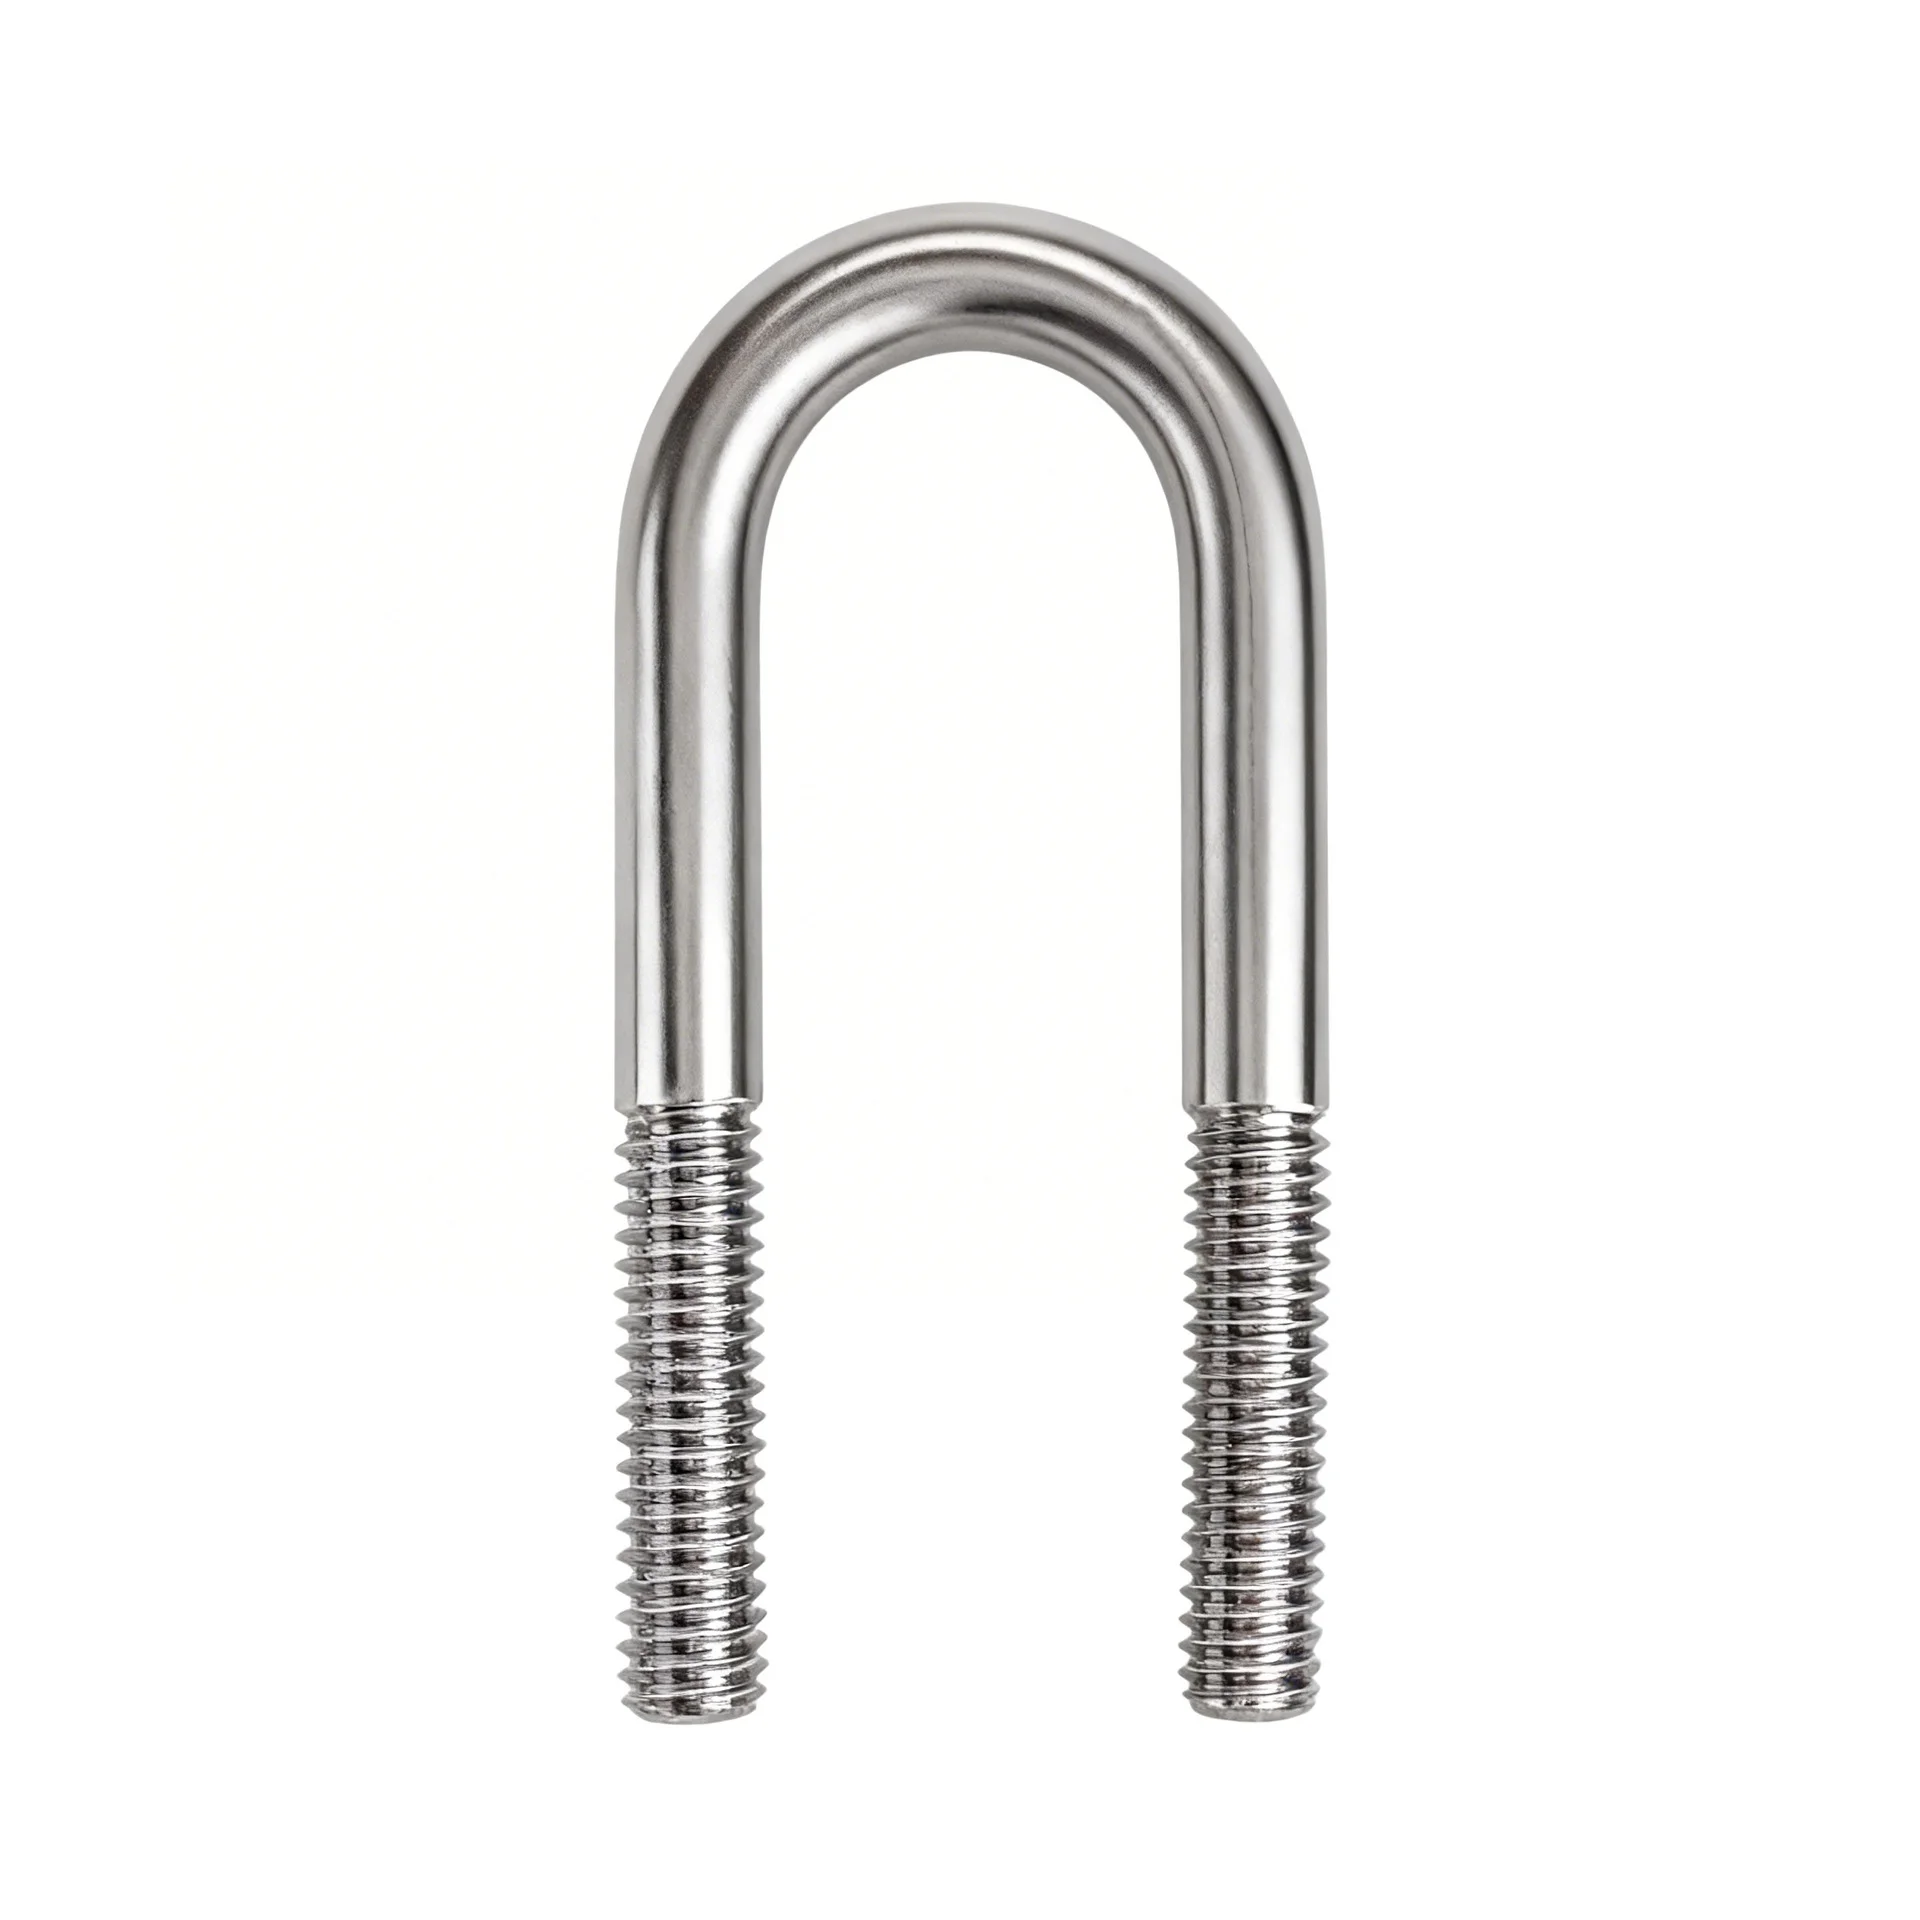
U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

U-bolt ( / U-bolt, M10/M12/M16/M20/M24 multiple specifications)

Brand: Wotu Surface: natural black oxide / hot-dip galvanized / blue-white zinc plated, multiple processes available Specifications: Based on common industry drawing parameters, suitable for pipe diameter 25mm~139.7mm, screw diameter M10~M24, total length can be nonstandard customized Matching: can be matched with nut, flat washer and spring washer of the same specifications for complete shipment Packaging: Bundling and packaging + 25kg export carton, full-container wooden pallet wrapped with film, supports private-label export packaging

Read More
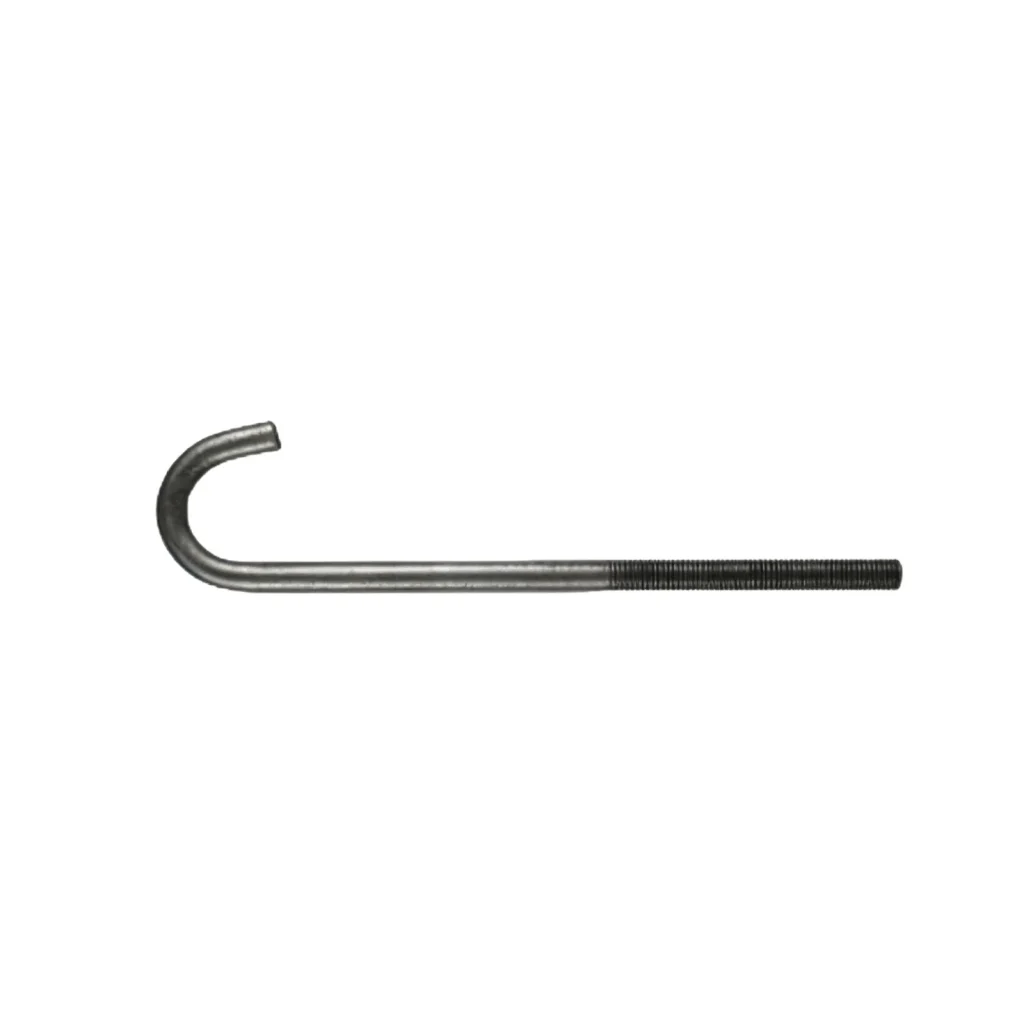
7-letter, 9-letter L-shaped anchor bolt (Chinese national standard GB/T799-1988 embedded anchor screw)

7-letter, 9-letter L-shaped anchor bolt (Chinese national standard GB/T799-1988 embedded anchor screw)

Brand: Wotu Surface: Natural black oxide treatment, customized hot-dip galvanized, zinc plated as required Specifications: Follow Chinese national standard GB/T799-1988, in stock M12-M48, total length 120mm~1500mm, nonstandard customized diameter, bending length, total screw length available Matching: Nuts, flat washers and spring washers of the same specification can be supplied in complete sets. Packaging: Bundling and packaging, using wooden pallets and film-wrapped export packaging in large quantities

Read More
Hex thin nut

Hex thin nut

Brand: Wotu Surface: zinc plated Specifications: in stock M8~M64 full standard specifications, covering precision, machinery, and steel structure full size range, supporting nonstandard tooth pitch and customized thickness Matching: Can be matched with bolts of corresponding specifications, flat washer, spring washer complete set of shipment Packing: packed in 25kg cartons and packed on wooden pallets.

Read More
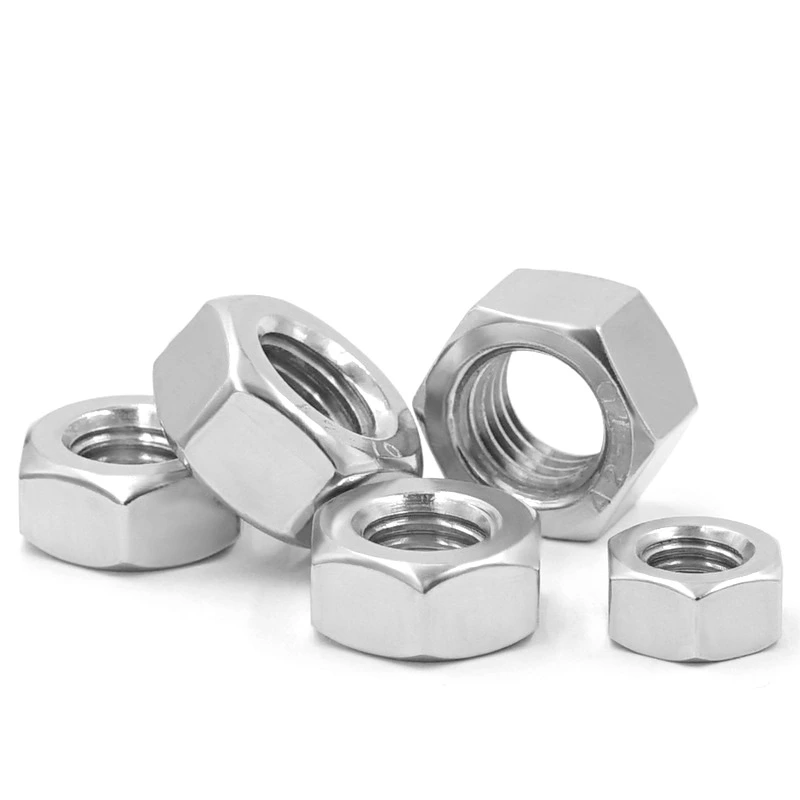
Hex nut (Chinese national standard GB52-1976)

Hex nut (Chinese national standard GB52-1976)

Brand: Wotu Surface: 304 stainless steel Specifications: in stock M6~M24 full standard metric specifications, supports nonstandard pitch, thickening/customized Matching: Can be matched with bolts of corresponding specifications, flat washer, spring washer complete set of supporting shipment Packaging: 25kg cartons, whole wooden pallets

Read More
Hot-Dip Galvanized Chinese National Standard Flat Washer (GB/T97.1A Level Flat Washer)

Hot-Dip Galvanized Chinese National Standard Flat Washer (GB/T97.1A Level Flat Washer)

Brand: Wotu Surface: overall hot-dip zinc plated anti-corrosion treatment, optional blue-white zinc plated, color zinc plated, black oxide Specifications: Execute GB/T97.1-2002 Chinese national standard, in stock M6-M64 full range of specifications, inner diameter, outer diameter, thickness strictly comply with Chinese national standard parameters, support nonstandard size customized Packaging: 25kg woven bag / export carton packaging, full pallets wrapped with film, supports private-label customization

Read More
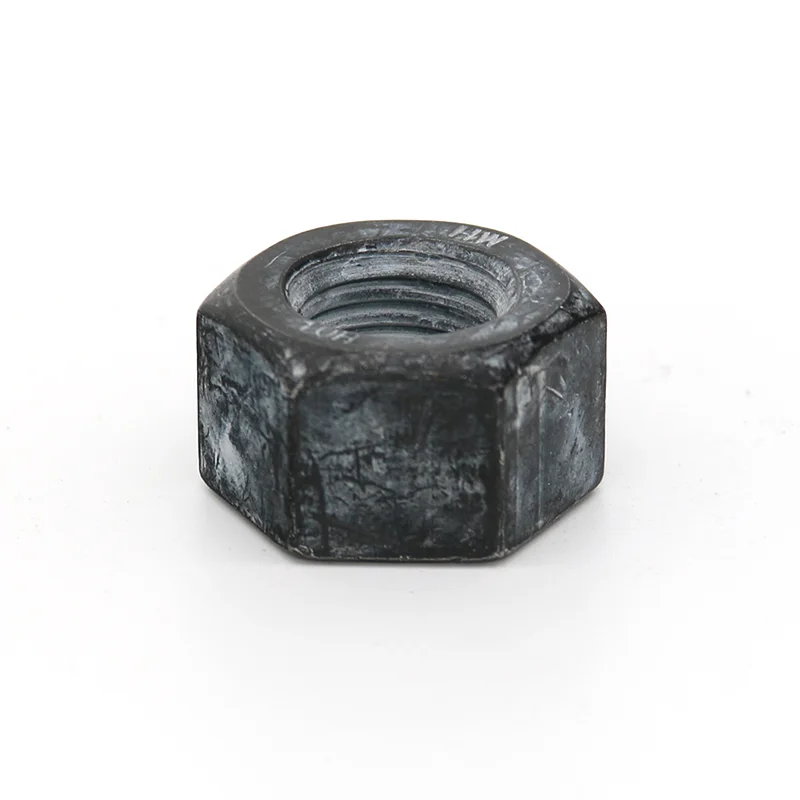
Grade 8/Grade 10 High-strength Black Oxide Hex Nut (DIN934/GB Chinese National Standard Thickened Nut)

Grade 8/Grade 10 High-strength Black Oxide Hex Nut (DIN934/GB Chinese National Standard Thickened Nut)

Brand: Wotu Surface: quenching and tempering heat treatment + high temperature black oxide anti-rust treatment Specifications: Comply with DIN934, GB/T6170 standards, in stock M6-M48 full range of specifications, nonstandard sizes can be customized Packaging: 25kg carton/woven bag inner packaging, whole wooden pallet wrapped with film for export packaging, supports neutral/private-label customization packaging

Read More

Compare repeat machines by operation, control and changeover

Repeat machine selection criteria

When comparing a repeat machine, review the working method, tooling arrangement, workpiece handling, control and adjustment options, changeover procedure, inspection points and compatibility with your existing line. The right choice depends on the operation and required result rather than on the machine name alone.

Criterion What To Check Why It Matters Buyer Tip
Repeatable cycle control Ask how the machine sets, stores, and repeats the same operation across batches. Small changes in stroke, timing, or feed can create inconsistent parts and more sorting work. Can the operator lock the setting after approval so the next batch runs the same way?
Part size and tooling fit Confirm the material, part shape, and size range the machine is intended to handle. A repeat machine that works well on one fastener or component may need different tooling for another. Send a drawing or sample part and ask what tooling changes are required.
Feeding and part orientation Review how blanks or parts enter the machine and how misfeeds are detected. Poor feeding causes stoppages, damaged parts, and uneven output even when the main mechanism is accurate. Ask what happens if a part arrives upside down, doubled, or out of position.
Changeover between jobs Find out which adjustments are manual and which are preset or guided by the control system. Frequent job changes can turn a fast machine into a bottleneck if setup takes too long. Ask for the normal changeover steps for your two most common parts.
Access for maintenance and wear parts Identify the parts that wear during repeated cycling and how easily they can be inspected or replaced. High-repeat operation depends on stable guides, tooling, sensors, and moving parts. Ask which spare parts the buyer should keep on hand for regular production.

Choose a repeat machine for consistent production cycles

The practical distinction is between cycle repetition and process repeatability. A basic machine may repeat the same timed sequence, while a more controlled system may monitor position, force, speed or other process conditions to keep each part within the required result.

This matters when small changes in material, tool wear or part positioning can affect fit or quality. For a simple repetitive task, a straightforward control system may be easier to maintain; for tighter production control, ask how the machine detects variation and how operators adjust or verify the process.

Define the operation first. Describe exactly what the machine must repeat: for example, a fastening, forming, pressing, feeding or assembly sequence. Include the workpiece material, shape, dimensions and any surface treatment. A machine designed for one type of movement or tooling may not suit a different operation, even if both are described as repetitive production.

Balance output with changeover needs. A machine configured for one stable part may offer a simpler workflow, while a flexible machine can be more useful where several part variants share the same line. Ask how tooling, guides and stored programs are changed, and whether the changeover can be completed without extensive adjustment or trial production.

Check feeding and quality control as part of the whole process. Repeated motion does not solve inconsistent blanks, misalignment, tool wear or incorrect part orientation. Confirm how parts enter the machine, how jams or missing parts are handled, and what checks are available for the finished result. Avoid judging the machine only by its cycle description if the surrounding feeding and inspection steps remain manual.

Prepare a representative enquiry. Send a drawing or clear part description, the operation to repeat, material information, expected production pattern, acceptable variation and any existing equipment the machine must connect with. Ask which assumptions need testing and what sample run or process review is recommended before finalising the configuration.

Criteria Importance Description Example Options
Operation type Critical to the basic machine design The machine must match the actual action being repeated, such as pressing, forming, feeding, fastening or assembly. A machine suitable for one motion may not accept different tooling or part handling without redesign. A repeated pressing operation and a repeated fastening operation may both need stable positioning, but they use different tooling, force control and inspection methods.
Process repeatability High when finished-part consistency matters Look beyond the cycle sequence and consider whether the machine can keep the result consistent as materials, tooling and operators change. The right level of monitoring depends on the tolerance and risk of defects. A simple part may only need a repeated stop position, while a more sensitive operation may need checks for stroke, force or correct part presence.
Feeding and positioning Often the main cause of production instability A repeat machine can only work reliably if parts arrive in the correct orientation and location. Manual loading, bowl feeding, conveyor feeding or fixture loading each changes speed, flexibility and jam risk. Hand loading may suit low-volume work with several part types, while dedicated automatic feeding may suit one stable part made in higher volume.
Changeover requirements Important for mixed production or short runs Tooling, guides, fixtures and control settings may need adjustment when the part changes. A machine optimized for one part can be efficient, but a more adjustable setup may reduce downtime across multiple variants. A fixed fixture may run one part consistently, while adjustable guides and stored settings may be more useful for a family of similar parts.
Inspection and fault handling Important where scrap, rework or line stoppage is costly Ask how the machine handles missing parts, misfeeds, tool wear, incomplete operations and operator adjustment. Inspection can be manual, in-process or downstream depending on the application. For a low-risk operation, periodic operator checks may be enough; for a critical assembly step, part presence and completed-cycle checks may be needed.

Product Selection

Related Options

For a line producing the same part repeatedly, the main priority is stable positioning and a controllable cycle from loading through completion. For mixed part sizes or frequent design changes, give greater weight to accessible tooling changes, recipe management and adjustment range before comparing automation level or headline output.

Blog Articles / Reviews

Why Do U Bolts Loosen in Pipe Supports? 6 Causes and Prevention Methods

Why Do U Bolts Loosen in Pipe Supports? 6 Causes and Prevention Methods

U bolts usually loosen in pipe supports because the connection loses clamping force, receives continuous vibration, restricts thermal pipe movement, uses an incorrectly sized U bolt, experiences surface settlement, or suffers from corrosion and inadequate inspection. This issue affects EPC contractors, pipe installers, industrial maintenance teams, equipment manufacturers and fastener distributors working with water, oil […]

Anchor Bolts: 7 Ordering Errors That Cause Site Rework

Anchor Bolts: 7 Ordering Errors That Cause Site Rework

ost anchor bolt ordering errors come from incomplete drawings, unclear dimensions, unsuitable material or coating choices, undefined tolerances, and mismatched nuts or washers. These mistakes affect steel fabricators, EPC contractors, equipment installers, importers, and distributors because anchor bolts are usually embedded before the connected structure arrives on site. Once concrete has cured, even a small […]

Hex Thin Nut vs Standard Hex Nut: Which Fits Space-Limited or Locking Assemblies?

Hex Thin Nut vs Standard Hex Nut: Which Fits Space-Limited or Locking Assemblies?

Direct Answer: Choose a hex thin nut when reduced nut height is genuinely required by the assembly or when the engineering design specifies it as part of a locking arrangement. Choose a standard hex nut when full nut height, normal thread engagement, and the specified load-bearing function are required. Buyers should compare nut height, thread […]

What Is a Fastener? Types, Functions and Industrial Uses

What Is a Fastener? Types, Functions and Industrial Uses

A fastener is a hardware component that mechanically joins or secures parts. Common examples include screws, bolts, nuts and rivets; washers are supporting components used in many fastening assemblies. Some connections can be dismantled by removing threaded fasteners, while others, such as riveted joints, normally require the fastener to be destroyed during removal. In industrial […]

Which Hexagonal Wood Screw Specifications Should Buyers Freeze Before Production?

Which Hexagonal Wood Screw Specifications Should Buyers Freeze Before Production?

A hexagonal wood screw order should not be released from a gauge number and length alone. Before production, the buyer and supplier need one approved specification that fixes the screw diameter, length basis, thread geometry, point, hex-head dimensions, material, finish, installation method, substrate and acceptance evidence. The pilot hole belongs in the application specification as […]

Applications of Anchor Bolts

Applications of Anchor Bolts

Fixed anchor bolts, also known as short anchor bolts, are cast in with the foundation and used to secure equipment that does not experience strong vibration or impact. 1. Fixed anchor bolts, also known as short anchor bolts, are cast in with the foundation and used to secure equipment that does not experience strong vibration […]

Frequently Asked Questions

What information is needed to judge whether a machine suits my operation?

Provide the workpiece drawing or size range, material, the action to be repeated, the required finished result and the expected production pattern. It also helps to explain how parts will be loaded, positioned and removed, because feeding and handling often decide whether the repeated cycle stays stable.

Is a fully automatic machine always the better option?

Not always. A simpler semi-automatic arrangement may be easier to set up and maintain for small batches, frequent part changes or operations that still need operator judgment. Full automation becomes more attractive when the part is stable, the volume is high and feeding, positioning and inspection can be controlled reliably.

What is the common misunderstanding about repeatability?

Repeating the same motion is not the same as producing the same result. Material variation, tool wear, part misalignment and inconsistent feeding can all change the finished part even if the machine cycle is unchanged. Ask how the process is adjusted, checked and stopped when variation occurs.

How should I compare different control methods?

A basic timed or sequence-based control may be enough for a simple repetitive action with generous tolerance. If the result depends on position, force, speed or stroke consistency, ask whether those conditions can be set, monitored or verified during production. More control can improve process visibility, but it can also add cost, training and maintenance needs.

What should be checked before approving a configuration?

Confirm the tooling concept, loading method, part orientation control, changeover steps and inspection points. If possible, review sample parts or a trial process using the same material and part condition that will be used in production. This reduces the risk of buying a machine that repeats a cycle but does not produce the required outcome consistently.

Leave Your Message

Describe the operation to be repeated, the workpiece material and dimensions, and your expected production pattern. If the machine must connect to existing equipment, include the required feeding, inspection or control interface.