Threaded Inserts For Plastic Selection Guide | Hebei Wotu Fastener Manufacturing Co., Ltd.

Threaded Inserts for Plastic

Threaded inserts for plastic create a reusable metal thread in a molded, printed, or machined plastic part. The main decision is not only the thread size; it is how the insert will be installed, how much load the plastic can support, and whether the joint must survive repeated assembly.

For a stable purchase decision, match the insert style to the plastic material, boss design, installation method, and service conditions before confirming quantity or price.

Related Products

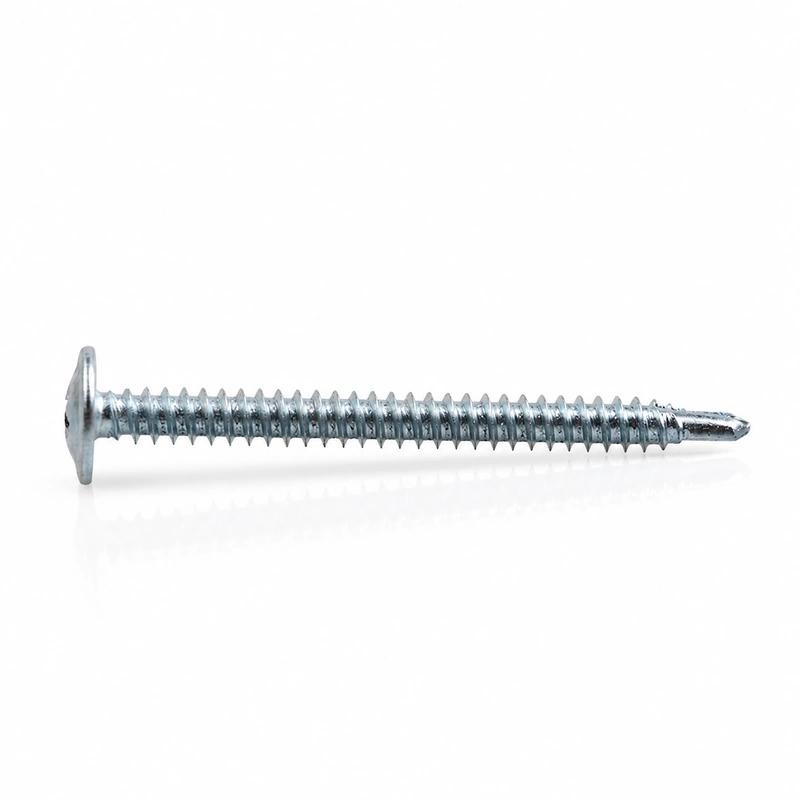
Countersunk Head Cross Thick Thread Fiberboard Screw

Countersunk Head Cross Thick Thread Fiberboard Screw

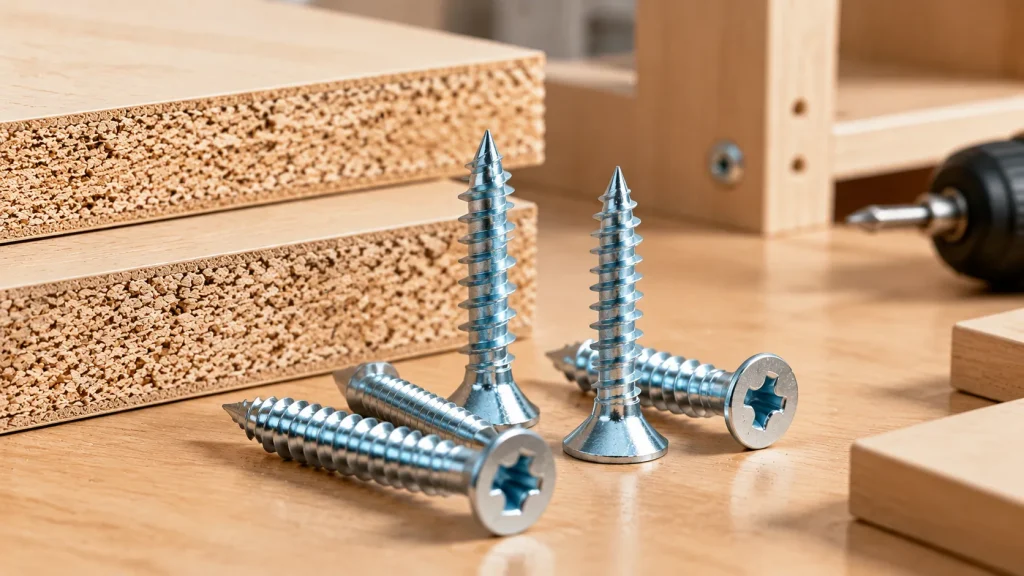
Brand: Wotu Surface: color zinc plated electroplating Specifications: in stock 3.5/4.0/4.5/5.0 regular wire diameter, rod length 16~80mm full range of specifications in stock, supports nonstandard length customization Packaging: 25kg cartons, whole wooden pallets

Read More
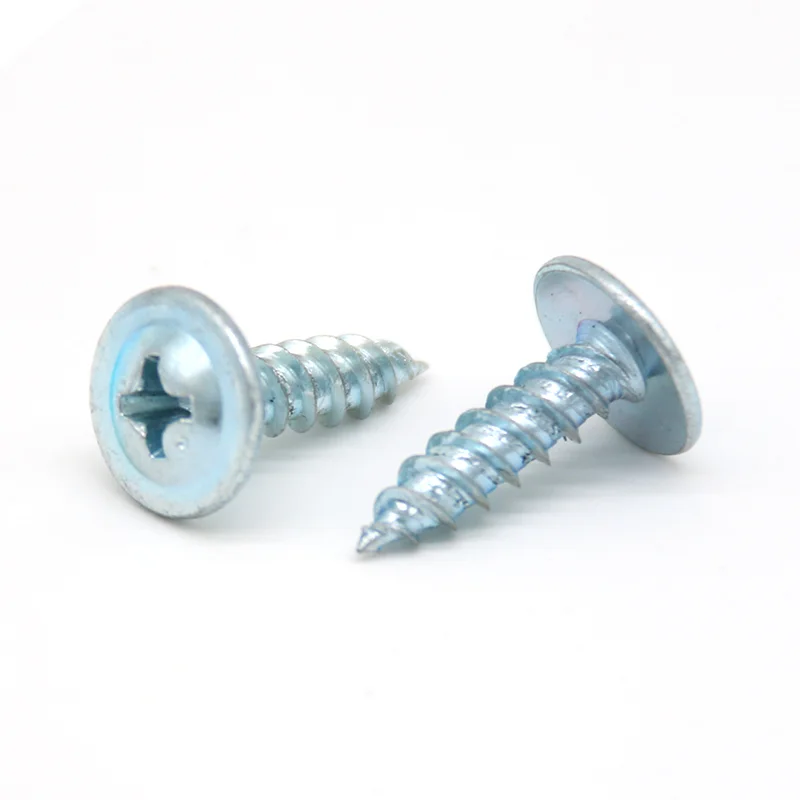
Blue-White Zinc Plated Pan Head With Pad Self-Tapping Screw

Blue-White Zinc Plated Pan Head With Pad Self-Tapping Screw

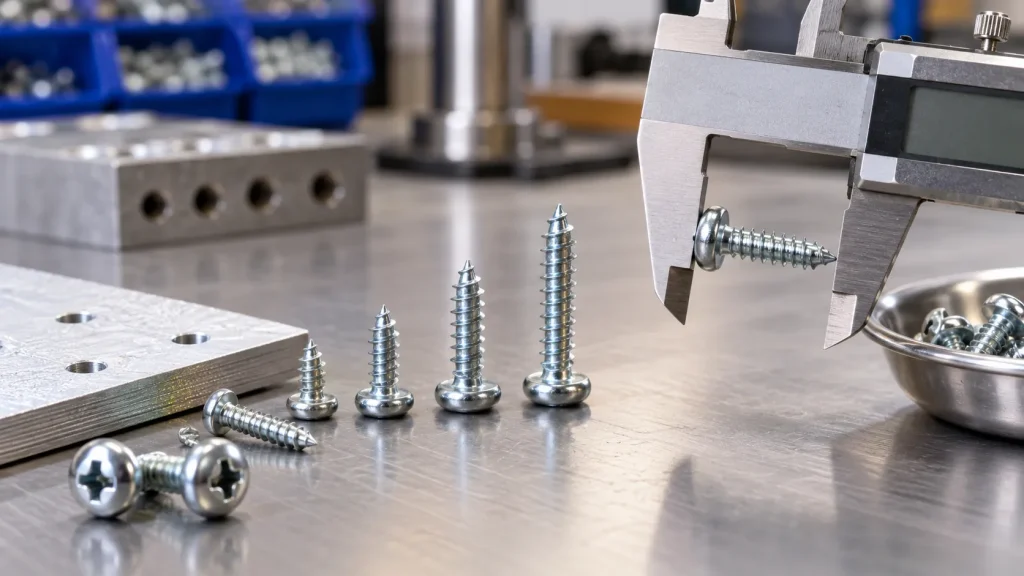
Brand: Hengzuan Surface: blue and white zinc plated Specifications: in stock ST4.2/ST4.8full range of specifications, length 13~50mm in stock, support nonstandard length customization Packaging: 25kg cartons, solid wood packaging, support neutral packaging, private-label customization

Read More
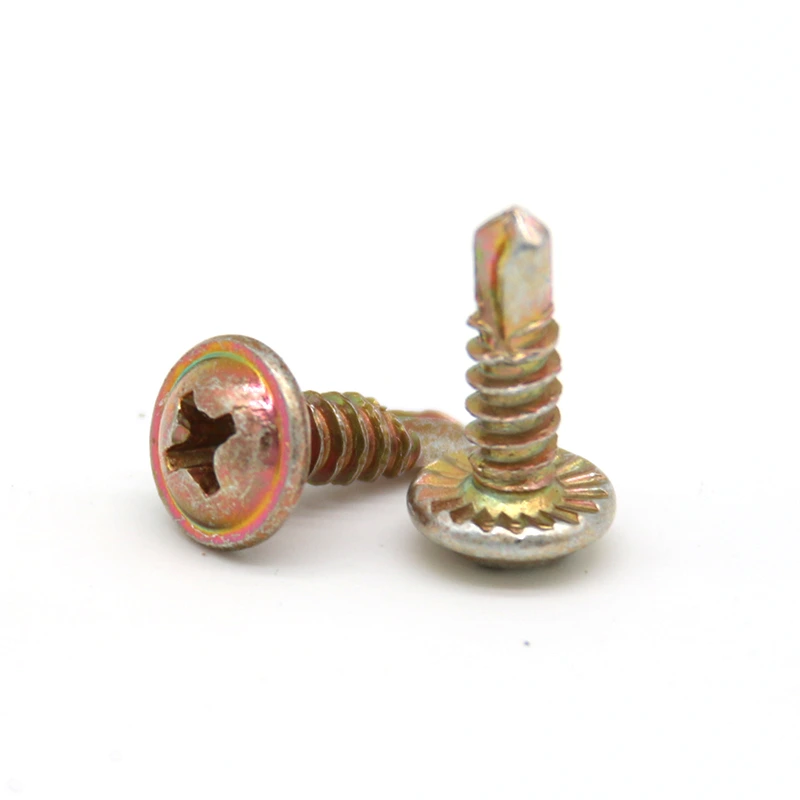
Wafer Head Self-Drilling Screw

Wafer Head Self-Drilling Screw

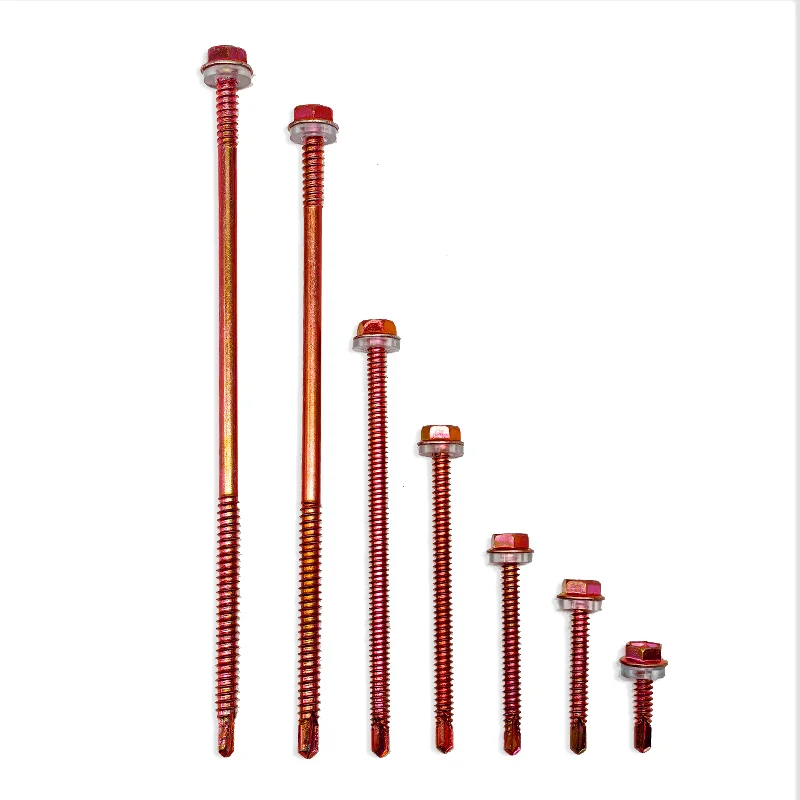
Brand: Hengzuan Surface: blue and white zinc plated, can be customized color zinc plated, black oxide plated Specifications: Comply with GB/T15856.2 Chinese national standard, in stock ST3.5/ST4.2/ST4.8/ST5.5 mainstream wire diameter, rod length 13mm~50mm full range of specifications, nonstandard length customization on demand, drilling applicable plate thickness 2~5mm Packaging: 25kg export cartons, full pallets wrapped with film, supports neutral export packaging, private-label customization

Read More
Countersunk Head Blue-White Zinc Plated Self-Drilling Screw (Chinese National Standard: Phillips Countersunk Head Self-Drilling And Self-Tapping Screw GB/T15856.2-2002)

Countersunk Head Blue-White Zinc Plated Self-Drilling Screw (Chinese National Standard: Phillips Countersunk Head Self-Drilling And Self-Tapping Screw GB/T15856.2-2002)

Brand: Hengzuan Surface: blue and white zinc plated, can be customized color zinc plated, black oxide plated Specifications: Comply with GB/T15856.2-2002 Chinese national standard, in stock ST4.2/ST4.8/ST5.5 full range of specifications, length 13mm~75mm optional, supports customized nonstandard rod lengths; drilling adaptation plate thickness 0.7~6mm Packaging: 25kg export cartons, full pallets wrapped with film, supports neutral export packaging, customer private-label customization

Read More
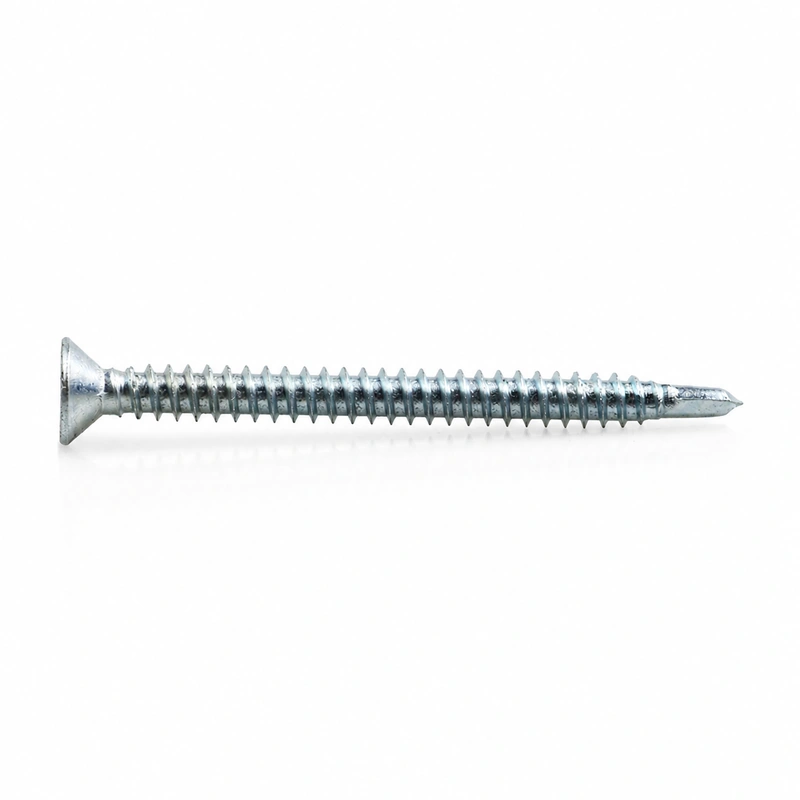
Countersunk Head Self-Tapping Screw

Countersunk Head Self-Tapping Screw

Brand: Hengzuan Surface: blue and white zinc plated, optional color zinc plated, black oxide treatment Specifications: Follow GB/T846-1985 Chinese national standard, in stock ST4.2/ST4.8/ST5.5 full range of specifications Packaging: 25kg export cartons, full pallets wrapped with film, supports neutral export packaging, private-label customization

Read More

Key insert details to compare before ordering

Insert selection

Compare threaded inserts for plastic by installation method, external knurl or retention profile, thread size, body length, flange style, material, and compatibility with the plastic part design. The right choice should fit both the assembly requirement and the way the insert will be installed in production.

Criterion What To Check Why It Matters Buyer Tip
Insert installation method Compare heat-set, ultrasonic, press-fit, and self-tapping designs against the plastic part and assembly equipment. The installation method affects cycle time, equipment needs, hole design, and the risk of cracking or distortion. Ask which insert types are available for your plastic grade and whether installation guidance or process samples can be provided.
Plastic grade and part geometry Share the resin, filler content, wall thickness, boss shape, and available installation-hole dimensions for review. A design that works in a tough reinforced plastic may damage a thin or brittle boss, while the wrong hole fit can reduce retention. Send a part drawing or representative sample and ask for the recommended hole and boss design.
Internal thread and engagement Confirm the thread form, nominal size, usable thread depth, and screw engagement required by the joint. Insufficient engagement can strip the insert or screw thread; excessive screw length can bottom out or damage the plastic part. Provide the mating screw specification and clamped-part thickness before finalizing the insert length.
Insert material and service environment Verify the insert material and finish against moisture, chemicals, temperature changes, and contact with the mating fastener. The surrounding plastic may tolerate the environment while the insert or screw interface corrodes, binds, or loses serviceability. Describe the exposure conditions and ask which material and finish are suitable for the intended service life.
Retention and assembly performance Request applicable pull-out, push-out, and torque information for the chosen insert, plastic, hole design, and installation process. Retention depends on the complete joint rather than the insert alone, so catalogue fit does not guarantee reliable assembly. Ask how test conditions match your part and whether sample testing can confirm installation torque and repeated screw removal.

Matching a threaded insert to the plastic part and assembly load

The most important distinction is between inserts that are installed with heat, ultrasonic energy, press-fit force, expansion, or molding-in during part production. Heat-set and ultrasonic inserts are common for thermoplastics because the surrounding plastic flows around the knurl pattern. Press-fit or expansion styles can be useful when heat is not suitable, but they depend heavily on hole control and plastic strength.

This matters because the wrong installation method can damage the boss, reduce pull-out resistance, or create weak threads even if the insert material and thread size look correct on a drawing. A small change in hole diameter, boss wall thickness, or knurl geometry can change the result more than buyers expect.

Start with the plastic and production process. ABS, PC, PA, POM, PP, and glass-filled materials behave differently during insertion and loading. A brittle or highly filled plastic may need a different outside profile than a softer thermoplastic. If the part is 3D printed, tell the supplier the print material, print direction, and whether the insert will be installed after printing.

Choose the insert style around the load case. Pull-out load, torque resistance, vibration, repeated screw removal, and clamp force do not all favor the same design. Straight knurls, helical knurls, undercuts, flanges, and closed-end bodies each solve different problems. A flange can help control seating, while a blind or closed-end insert can help where screw depth must be limited.

Do not freeze the insert before checking the mating part design. Boss outside diameter, hole depth, lead-in, wall thickness, and screw engagement length should work together. A common mistake is selecting an insert from thread size alone, then discovering that the plastic boss is too thin or the screw bottoms out before clamping the assembly.

For the next step, send the thread size, insert type if already chosen, plastic material, hole or boss drawing, installation method, expected screw removal frequency, and any surface finish or material preference. If you are asking Hebei Wotu Fastener Manufacturing Co., Ltd. for supply, confirm whether the required insert style and material are available before treating the design as final.

Criteria Importance Description Example Options
Installation method Usually the first decision after material Heat-set, ultrasonic, press-fit, expansion, and molded-in inserts place different demands on equipment, hole tolerance, and plastic behavior. A thermoplastic housing may suit heat insertion, while a part that cannot be heated may need a mechanical press-fit or expansion style.
Plastic material and boss design Critical for retention and crack resistance The surrounding plastic must support installation force and service load. Boss diameter, wall thickness, hole depth, and bottom clearance can change performance more than the thread size alone. A thin boss around a long insert may crack during installation or under screw tightening.
Retention profile Important when load or screw cycling is significant Knurls, grooves, undercuts, and flanges affect pull-out resistance, torque resistance, seating control, and resistance to rotation. A flanged insert can help control seating depth, while a more aggressive external profile may improve resistance to turning in the plastic.
Open-end versus closed-end body Application-dependent Open-end inserts allow screw length flexibility but need enough clearance behind the insert. Closed-end or blind styles help limit screw depth or protect the opposite side of the part. A cover with limited internal clearance may require a closed-end insert to prevent the screw from passing through.
Assembly service life High for parts opened repeatedly Parts that are serviced often need stable metal threads, controlled clamp load, and enough engagement length to avoid loosening or stripping the plastic support. An electronics enclosure opened for maintenance needs more attention to screw cycling than a one-time assembled trim part.

Blog Articles / Reviews

How to Specify Countersunk Head Cross Thick Thread Fiberboard Screws for Furniture Assembly Projects

How to Specify Countersunk Head Cross Thick Thread Fiberboard Screws for Furniture Assembly Projects

Fiberboard screws are selected based on more than screw size alone. For furniture assembly and board-based applications, buyers need to match the screw structure with the characteristics of fiberboard, MDF, and similar engineered wood materials. A suitable specification should consider thread design, head style, screw length, diameter, installation method, and application requirements. For buyers sourcing […]

How Should Buyers Evaluate Self Tapping Screws for Project Procurement?

How Should Buyers Evaluate Self Tapping Screws for Project Procurement?

#4 self tapping screws should not be purchased from the “#4” designation alone. For a usable B2B specification, the buyer still needs the actual screw diameter, thread form or pitch, overall length, substrate, pilot-hole condition, head and drive style, material, surface finish and quantity. This matters because suppliers may use different naming systems. Wotu Fastener’s […]

Which M10–M24 U-Bolt Measurements Must Buyers Send Before an RFQ?

Which M10–M24 U-Bolt Measurements Must Buyers Send Before an RFQ?

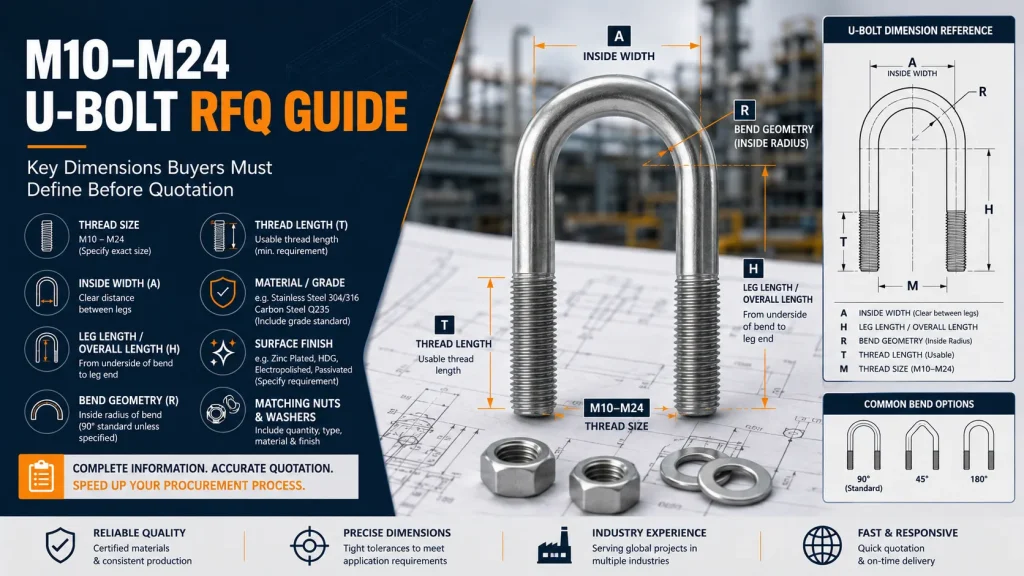
Direct Answer: For an M10–M24 U-bolt RFQ, buyers should send a dimensioned drawing that defines thread diameter, inside width, leg or overall length, bend geometry, thread length, application diameter, material or grade requirement, surface finish, matching nuts/washers, quantity, and packing needs. Nominal thread size alone is not enough because different measurement datums can produce U-bolts […]

Which Hexagonal Wood Screw Specifications Should Buyers Freeze Before Production?

Which Hexagonal Wood Screw Specifications Should Buyers Freeze Before Production?

A hexagonal wood screw order should not be released from a gauge number and length alone. Before production, the buyer and supplier need one approved specification that fixes the screw diameter, length basis, thread geometry, point, hex-head dimensions, material, finish, installation method, substrate and acceptance evidence. The pilot hole belongs in the application specification as […]

What Should Buyers Check Before Ordering Hot-Dip Galvanized Flat Washers?

What Should Buyers Check Before Ordering Hot-Dip Galvanized Flat Washers?

A hot-dip galvanized flat washer should be purchased as a defined joint component, not simply as an M-size metal disc. A usable specification identifies the dimensional standard and series, nominal size, inside and outside diameters, thickness, product grade, hardness or mechanical requirement, base material, coating requirement and the bolt, nut and bearing surface with which […]

DIN 931 vs DIN 933 Hex Bolts: What Should Buyers Confirm Before Bulk Ordering?

DIN 931 vs DIN 933 Hex Bolts: What Should Buyers Confirm Before Bulk Ordering?

DIN 931-style half-thread and DIN 933-style full-thread hex bolts should not be selected from diameter and overall length alone. The practical choice depends on the joint stack, required grip, location of the thread transition, available nut engagement, mating hardware, material or property requirement, coating system and governing product specification. A half-thread bolt is not automatically […]

Frequently Asked Questions

Can the same insert be used in all plastic materials?

No. Softer thermoplastics, brittle plastics, and glass-filled materials respond differently to heat, pressure, and loading. Confirm the resin grade, filler content if known, and molded or printed part design before fixing the insert style.

Should I choose heat-set inserts or press-fit inserts?

Heat-set inserts often suit thermoplastics because heat allows the plastic to flow around the external profile. Press-fit inserts avoid heat but need tighter hole control and enough plastic strength around the boss. The better choice depends on the material, available installation equipment, production volume, and required pull-out or torque resistance.

Is thread size enough information to quote or select an insert?

Thread size is only one part of the decision. Body length, outside diameter, knurl pattern, flange style, hole depth, boss wall thickness, and screw engagement can all affect whether the joint works reliably.

What is a common design mistake with inserts in plastic bosses?

A frequent mistake is leaving too little plastic around the insert. Even a strong metal thread can fail if the boss cracks, deforms, or cannot support the installation force. Check the boss diameter, wall thickness, lead-in, and bottom clearance together with the insert drawing.

When is a molded-in insert a better option?

A molded-in insert can be useful when the part is designed around insert placement during molding and the assembly needs strong retention without a secondary installation step. It also adds tooling and process considerations, so it is not always practical for prototypes, small batches, or designs that may still change.

What details should be sent with an enquiry?

Send the internal thread size, target insert length if known, plastic material, installation method, hole or boss dimensions, expected screw cycles, and the load direction. If the style is not decided, share the part drawing and assembly requirement so suitable options can be discussed.

Leave Your Message

Send the thread size, plastic material, installation method, and a drawing or hole dimensions. Also note the expected load or service frequency so the insert style can be checked against the application.